Direct Factory Portfolio
Engineered HMI Assemblies, FPC Circuits & Specialized Substrates
Seamlessly integrate custom graphic overlays, tactile dome arrays, backlighting solutions, and embedded controller boards built in our Shenzhen facility under full CE compliance.
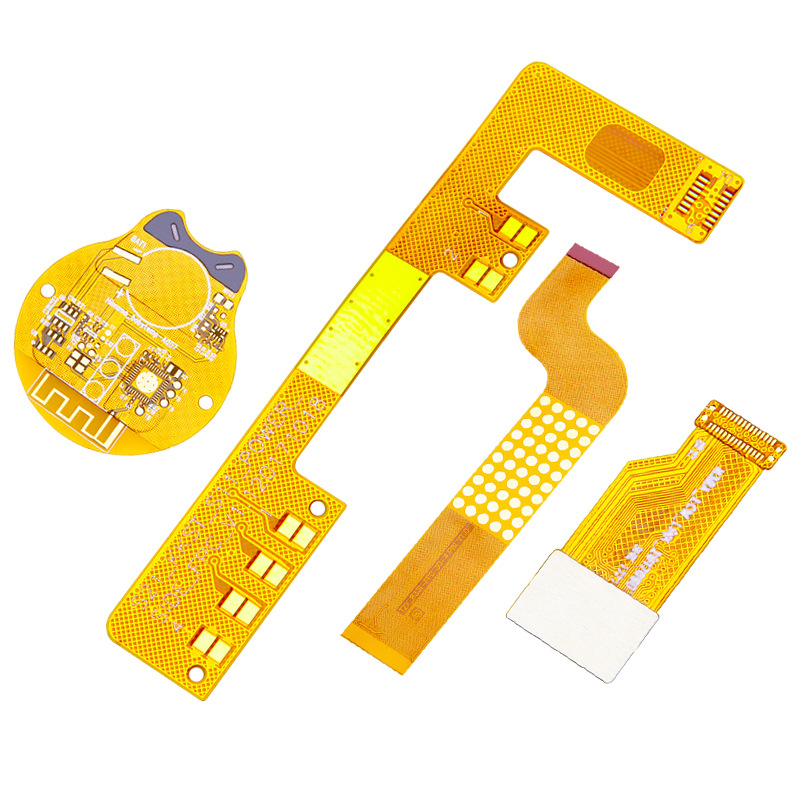
High-Temperature Resistant FPC Flexible PCB (Polyimide Substrate)
Examine Specifications →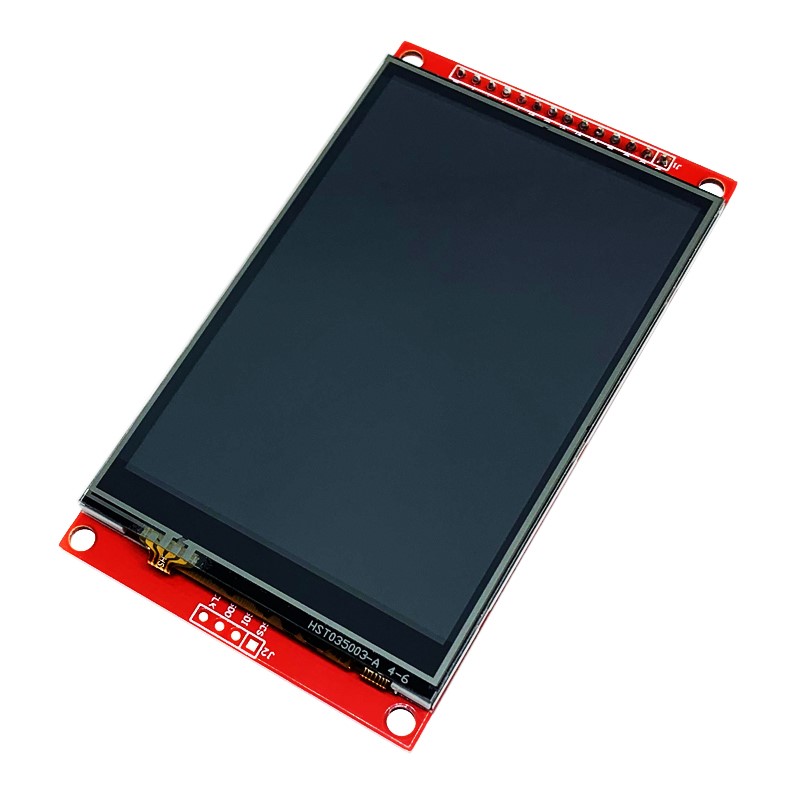
3.5-Inch TFT LCD Display Module 320x480 SPI Serial Screen
Examine Specifications →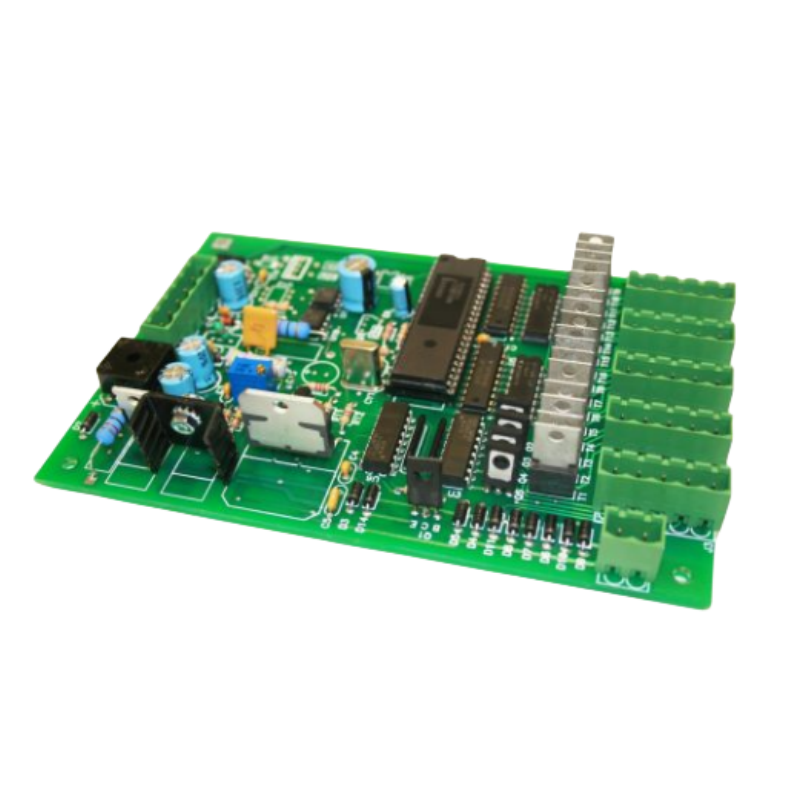
OEM PCBA One-Stop PCB Assembly (SMT & DIP Electronics)
Examine Specifications →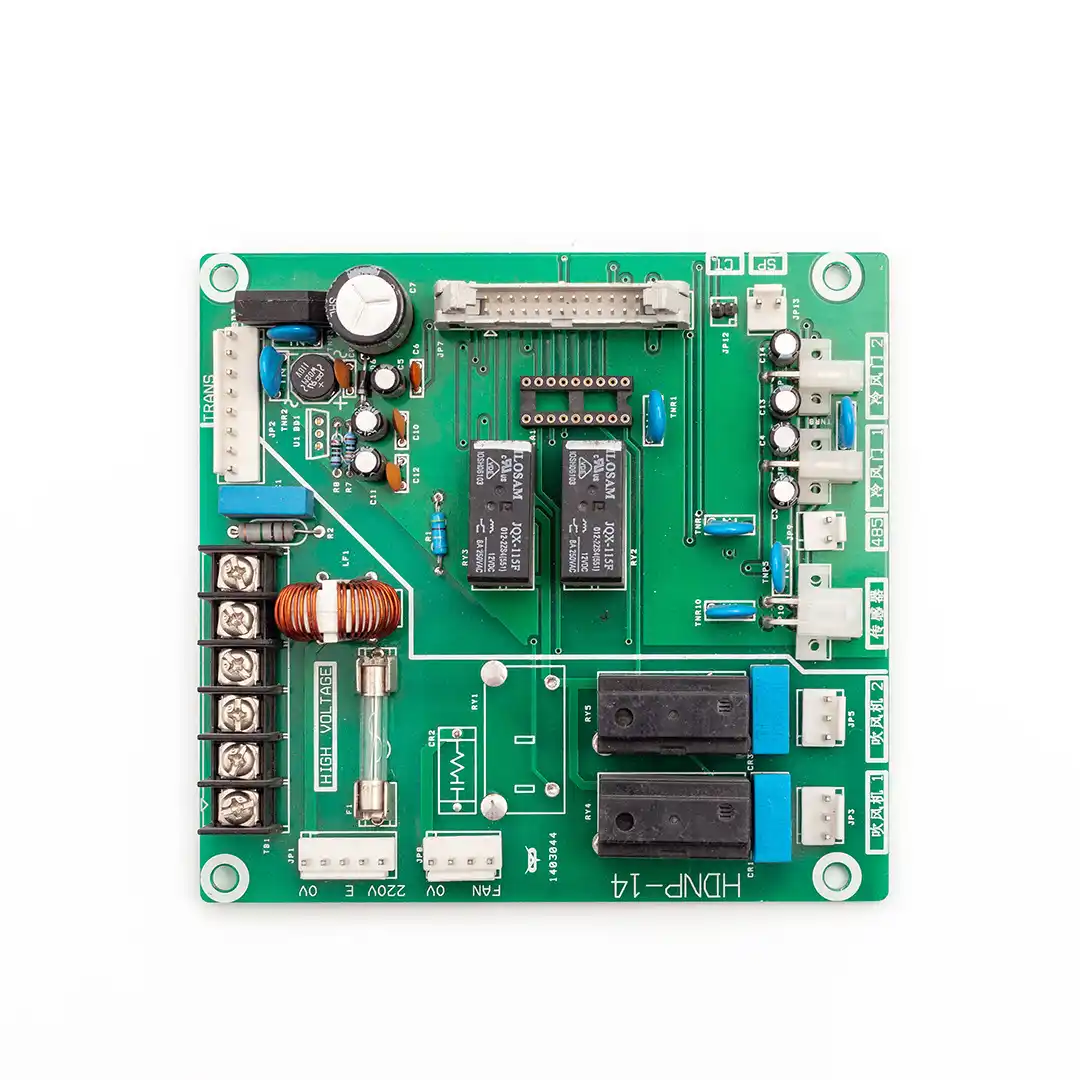
Custom PCBA Assembly with Complete Gerber & BOM Sourcing
Examine Specifications →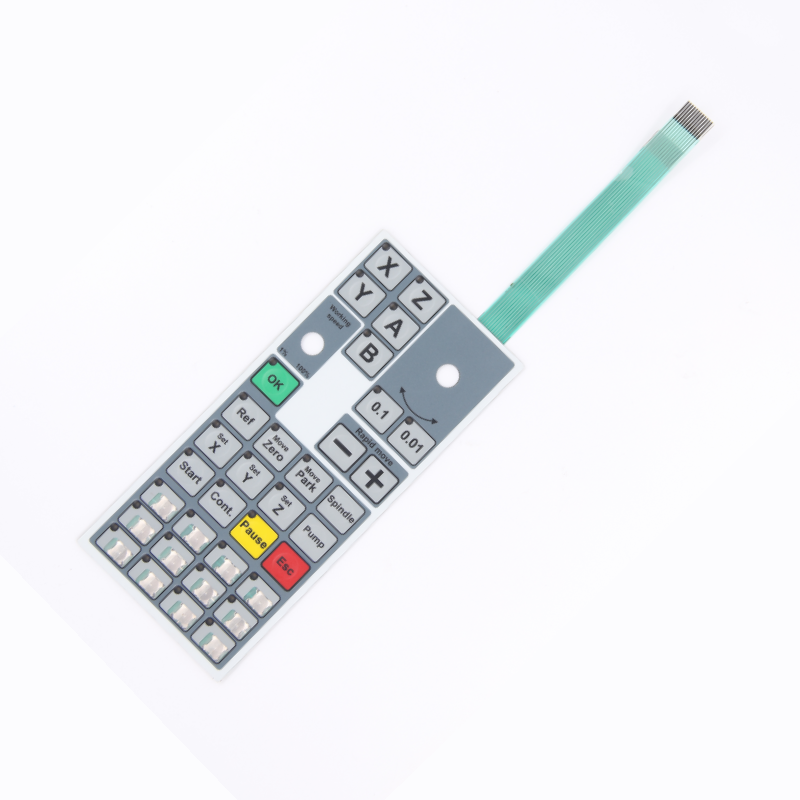
Custom Membrane Switch Keypad (PET/PC Overlay & Silver Paste)
Examine Specifications →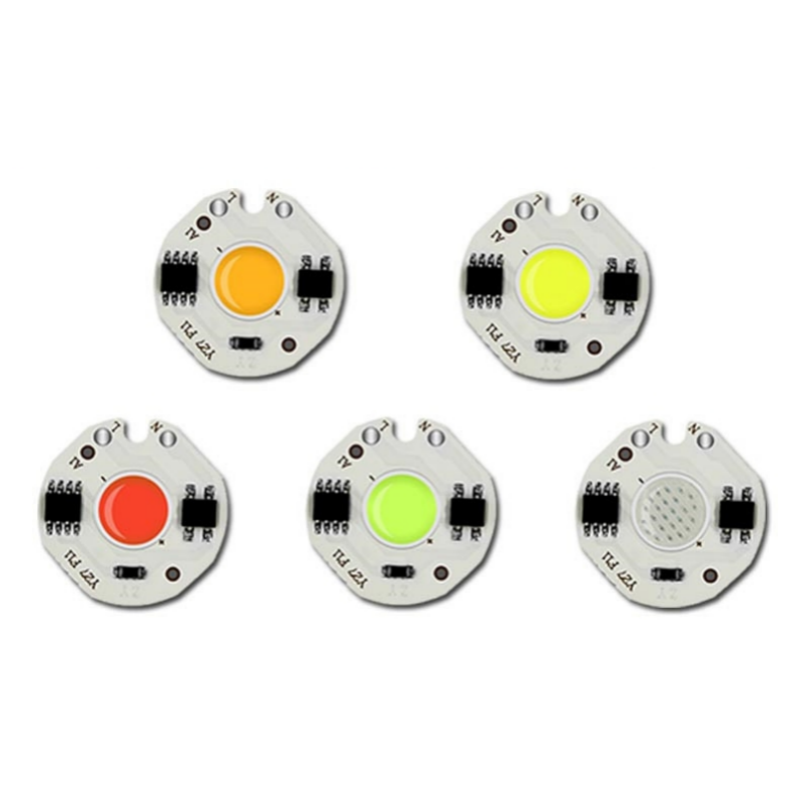
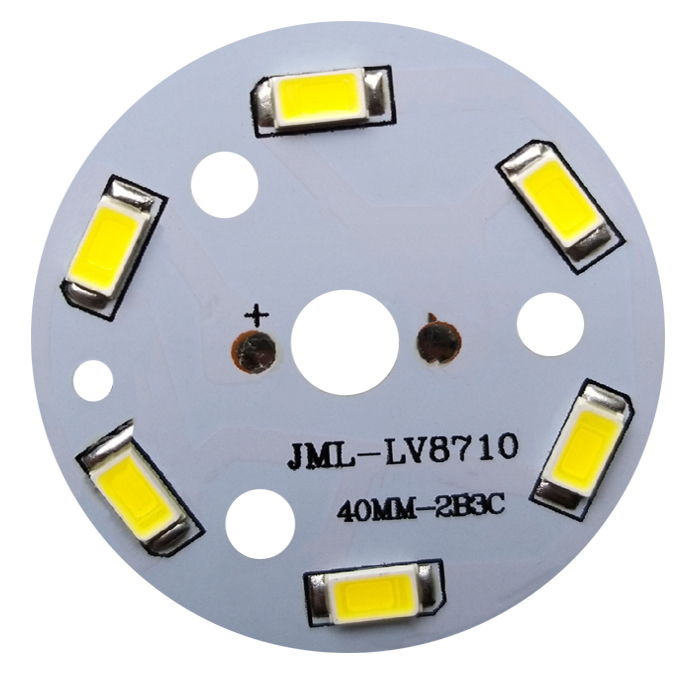
110V/220V Driverless COB LED Light Source Module
Examine Specifications →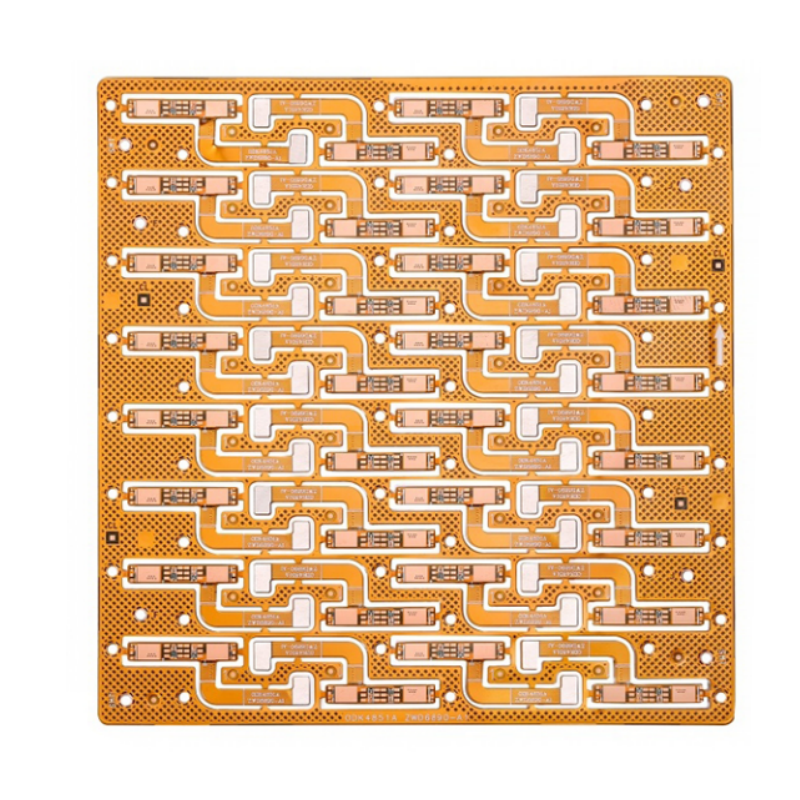
Custom FPC PCBA Service & Flexible Circuit Board SMT
Examine Specifications →14+
Years International OEM Export
5,000,000+
Switch Actuation Lifecycle
<24h
Engineering DFM Review Turnaround
5 Pcs
Flexible Low Prototyping MOQ
Engineering White Paper: CE Certification Demands for Industrial Membrane Switches
In modern industrial automation, medical electronics, cleanroom environments, and outdoor instrumentation, a membrane switch is no longer treated merely as a passive mechanical decal. Under the rigorous compliance landscape enforced by the European Union, an electronic user-interface panel entering the European Economic Area (EEA) must demonstrate definitive conformity with harmonized CE directives. As an experienced manufacturing partner based in Shenzhen, VUKO Electronics engineers membrane keypads, graphic panels, and integrated PCBA sub-assemblies to withstand exhaustive European third-party audit requirements.
Core Regulatory Insight: To apply the CE mark legitimately on a membrane switch sub-assembly containing active or passive circuitry, compliance documentation must verify alignment with the Electromagnetic Compatibility (EMC) Directive 2014/30/EU, the Low Voltage Directive (LVD) 2014/35/EU, and the RoHS 3 Directive 2015/863/EU amending 2011/65/EU.
1. Electromagnetic Compatibility (EMC Directive 2014/30/EU)
Membrane switches act as the primary boundary layer between human electrostatic discharge (ESD) and delicate internal microcontrollers. Under EN 61000-4-2 (Electrostatic Discharge Immunity), our membrane assemblies are engineered to absorb up to 15kV air discharge and 8kV contact discharge without latch-up or trace breakdown. We accomplish this by designing multi-layer shielding barriers: printed conductive silver/carbon grids, full-surface sputtered Indium Tin Oxide (ITO) layers, or copper-clad polyimide backing layers tied directly to chassis ground via perimeter grounding tails.
2. Low Voltage Directive (LVD 2014/35/EU) & Dielectric Integrity
When membrane switch panels interface with equipment operating within 50 to 1,000 V AC or 75 to 1,500 V DC, dielectric breakdown strength is a safety-critical parameter. VUKO utilizes high-dielectric polyester (PET) films (e.g., DuPont Mylar, MacDermid Autotex) that offer dielectric insulation capabilities exceeding 1,500V AC per 0.125mm thickness. Insulation resistance between non-connected conductive traces is maintained at >100 MΩ at 500V DC under standard humidity cycles, preventing leakage currents and guaranteeing operator safety.
3. Material Safety & Environmental Stewardship (RoHS & REACH)
All raw materials—including graphic overlay films, pressure-sensitive acrylic adhesives (e.g., genuine 3M 467MP, 3M 468MP, 3M 300LSE), conductive silver paste, carbon bridge inks, and UV-curable dielectric coatings—are strictly certified free of hazardous heavy metals, polybrominated biphenyls (PBB), and phthalates (DEHP, BBP, DBP, DIBP). Batch-specific XRF material testing and full chemical declaration sheets (CoC) accompany our volume export shipments.
Material Stack-Up Science & Electro-Mechanical Dynamics
The operational lifespan, tactile tactile sensation, and environmental resilience of a custom membrane switch hinge upon precise multi-layer mechanical stack-up design. Below is a detailed engineering comparison of raw substrate materials commonly specified in our Shenzhen workshops:
| Evaluation Parameter | Autotex Textured PET (Polyester) | Polycarbonate (PC / Lexan) | Flexible Printed Circuit (FPC - PI) | Rigid FR-4 Backed Assembly |
|---|---|---|---|---|
| Mechanical Flex Life | >5,000,000 continuous cycles | ~100,000 cycles (Stress-whitening prone) | >10,000,000 cycles (Dynamic bending) | Rigid structural backing (No flex) |
| Chemical / Reagent Resistance | Immune to IPA, acetone, acids, bleach | Susceptible to aromatic solvents | High chemical resistance (Kapton polyimide) | Resistant to standard industrial washes |
| Tactile Actuation Force Range | 180g to 450g (Via metal dome array) | 150g to 350g (Embossed polydome) | Customized snap tactile response | Tactile micro-switches or metal domes |
| Circuit Conductivity & Pitch | Screen-printed Ag (<1.0 Ω/sq, pitch ≥1.0mm) | Graphic fascia / non-conductive layer | Etched Cu (<0.05 Ω/sq, ultra-fine pitch) | Multi-layer etched copper routing |
| Thermal Endurance | -40°C to +85°C operating | -20°C to +75°C operating | -50°C to +150°C (Solder reflow safe) | Tg 130°C to 170°C (High-Tg optional) |
| Primary Application Profile | Medical, industrial HMI, food prep | Indoor displays, office electronics | High-density robotics, avionics, sensors | Heavy machinery, rugged test consoles |
Actuation Force Curves & Contact Bounce Control
Precision tactile response is governed by our computerized load-deflection testing. Using high-grade stainless steel domes (SUS301/SUS304) with options for gold or nickel plating, our switch profiles ensure a clean tactile snap ratio between 40% and 65%. Contact chatter (switch bounce) is strictly minimized to <5 milliseconds, eliminating false digital triggering in high-speed microcontrollers.
Future Procurement Trends & Next-Gen HMI Innovations
As smart manufacturing, IoT-enabled factory equipment, and portable diagnostic devices proliferate, human-machine interface procurement is shifting rapidly. Engineering directors and procurement executives are migrating away from legacy, single-function membrane keypads toward intelligent, hybrid control surfaces. Below are five defining procurement and technological evolutions identified by VUKO's R&D engineering division:
1. Transition to Copper FPC Backers
While screen-printed silver paste circuits remain cost-effective for static layouts, mission-critical systems increasingly demand etched copper polyimide (FPC) circuits. FPC backers eliminate silver migration (dendrite shorting) in high-humidity zones, permit ultra-dense ZIF connector termination, and enable direct surface-mount (SMT) reflow soldering of side-firing LEDs, resistors, and driver ICs directly onto the flexible membrane tail.
2. Capacitive Touch & Hybrid Switching
Procurement teams are ordering hybrid user interfaces that merge mechanical emergency buttons with capacitive slide, wheel, and multi-touch sensors behind flat, non-porous glass or chemically tempered PET overlays. This provides sleek, modern consumer-like aesthetics while complying with IP69K washdown sanitation requirements in clinical and pharmaceutical processing plants.
3. Optical Bonding of Displays & Backlights
Integrated HMI panels now frequently integrate display windows featuring anti-reflective (AR), anti-glare (AG), and anti-fingerprint (AF) surface coatings. We apply high-transmittance optically clear adhesives (OCA) to bond 3.5-inch to 10.1-inch TFT LCD/OLED modules directly underneath the membrane fascia, eradicating condensation, parallax shift, and internal ambient light reflections.
4. Hermetic IP67 / IP68 Ingress Sealing
Harsh operating conditions necessitate perimeter hydrophobic gasket channels. Utilizing high-tack, low-surface-energy adhesives (like 3M 300LSE) cut with precision laser die equipment, our engineers incorporate internal equalization air vents with breathable semi-permeable membranes (Gore-Tex vents) that equalize barometric pressure changes without allowing fluid, mist, or oil penetration.
5. Complete Turnkey Box-Build Integration Under One Purchase Order
Managing fragmented supply chains—ordering overlays from a printer, PCBs from a fabricator, SMT from an assembly house, and sheet metal brackets from a stamping vendor—results in accumulative dimensional stacking errors, delayed lead times, and disputed quality liability. Strategic buyers now leverage turnkey manufacturing partners capable of consolidating the entire sub-assembly: graphic overlay, tactile circuit, aluminum backing plate, controller PCBA, and display harness shipped as a 100% pre-tested modular unit.
Factory Pedigree & Manufacturing Advantages: Why Partner with VUKO
Shenzhen VUKO Electronics Co., Ltd. is positioned at the nexus of the world's most agile electronic manufacturing ecosystem. Over the past 14+ years exporting high-reliability hardware to North America, Western Europe, Japan, and Australia, we have refined our processes into a unified turnkey powerhouse that removes friction from custom HMI development.
Vertically Integrated Lines
In-house screen printing, automated CNC film cutting, SMT pick-and-place lines, flying probe testing, and cleanroom lamination avoid vendor markups and shorten iteration cycles.
24-Hour DFM Engineering Review
Submit your CAD, vector artwork, and Gerber/BOM packages. Our senior mechanical and PCB layout engineers evaluate trace spacing, dome pitch, venting paths, and tolerances within 24 hours.
Agile Low MOQ From 5 Pcs
Accelerate hardware validation with prototype pilot runs as low as 5 units. Seamlessly scale into production batches of hundreds of thousands with precision-machined steel tooling dies.
100% Comprehensive QC Testing
Every single membrane panel and PCBA undergoes 100% electrical continuity and short testing, loop resistance profiling, tactile actuation feel audit, and visual color spectrometry check.
Supply Chain Assurance: All international shipments are securely protected via Alibaba Trade Assurance, guaranteeing payment security, on-time delivery, and direct factory traceability from raw PET rolls to final anti-static vacuum packaging.
Comprehensive Procurement & Engineering DFM FAQ
Clear engineering communication prevents costly re-spins and delivery bottlenecks. Below are critical technical inquiries handled routinely by our international sales engineering department:
What specific test documentation is provided to satisfy European CE audits? +
For custom membrane switch panels and integrated PCBA sub-assemblies, VUKO supplies comprehensive Factory Acceptance Test (FAT) records. This encompasses Dielectric Breakdown Certificates (>1,500V AC), Contact Resistance logs (typically <100 Ω for silver paste, <1 Ω for copper FPC), Insulation Resistance verification (>100 MΩ at 500V DC), RoHS/REACH material chemical declarations, and life-cycle test certificates certifying actuation durability exceeding 1 to 5 million cycles.
How do you eliminate silver migration in high-temperature, humid environments? +
Silver migration (dendritic crystal growth) occurs when moisture, DC voltage bias, and silver ions interact across narrow trace spacings. To counter this, VUKO utilizes three proven counter-measures: (1) Applying continuous carbon over-print layers over all exposed silver trace contact fingers, (2) Implementing high-density UV dielectric crossover masks with zero pinhole tolerances, and (3) Recommending flexible printed circuits (copper FPC with polyimide coverlay) in operating environments exhibiting relative humidity greater than 85% RH.
What are the exact dimensional limits for trace width and pitch on screen-printed silver circuits? +
For conventional screen-printed silver conductive ink on heat-stabilized PET, our standard design rules require a minimum trace width of 0.5mm (0.020") and minimum trace-to-trace spacing of 0.5mm. In dense connector routing sections, we can achieve 0.35mm trace and spacing under tight environmental cleanroom parameters. If your design requires sub-0.2mm pitch, we transition the circuit layer to an etched copper FPC substrate.
What CAD files and graphic formats must be provided for quotation and tooling fabrication? +
To initiate a comprehensive 24-hour DFM and quotation, please supply: (1) Vector artwork for the graphic overlay in Adobe Illustrator (.AI), CorelDraw (.CDR), or vector .PDF format with PMS Pantone color codes designated, (2) 1:1 mechanical dimensional drawings with layer stack-up definitions in AutoCAD (.DWG or .DXF) or 3D STEP/IGES, and (3) Circuit schematics, netlists, or Gerber RS-274X files for the conductive trace routing and connector pinout pin-assignment.
How does VUKO achieve true IP65, IP66, and IP67 perimeter sealing? +
Standard membrane panels without perimeter seals are vulnerable to liquid wicking through edge capillary action. To achieve IP65 to IP67 sealing, we engineer a continuous adhesive perimeter border around all active circuit traces and dome cutouts, ensuring a minimum perimeter seal width of 3.0mm to 5.0mm. We pair this with high-performance 3M acrylic adhesive systems (such as 3M 468MP or 3M 300LSE) and incorporate internal air venting channels routed strictly between dome cavities rather than vented to the external atmosphere.
What tactile feedback options can be engineered into the keypad? +
We offer four distinct tactile styles: (1) Stainless steel metal domes (diameters from 6mm to 20mm; actuation forces from 180g to 450g with audible and crisp tactile feedback), (2) Thermally embossed graphic polydomes (formed directly on the PET overlay; moderate tactile feel with quiet actuation), (3) Flat, non-tactile switches with visual or audible LED/beeper feedback, and (4) Hybrid silicone rubber keypads bonded atop membrane switches to provide deep mechanical stroke travel (1.0mm to 2.5mm).
What is your typical tooling charge policy and lead time schedule? +
Initial engineering tooling covers film artwork plots, screen stencils, embossing dies, and laser cutting setup fees. Prototype samples (5 to 10 pcs) are typically manufactured within 7 to 10 business days following artwork and CAD approval. Mass production lead time averages 12 to 18 business days depending on volume and SMT component availability. For qualifying annual volume contracts, upfront NRE tooling charges can be fully amortized and credited back upon milestone order fulfillment.
Accelerate Your Custom HMI Project with Factory Direct Engineering
Submit your Gerber files, BOM lists, or panel artwork vectors today. Our senior technical team in Shenzhen delivers complete DFM feedback, stack-up optimization, and transparent tiered factory pricing within 24 hours.