Precision Electronics Portfolio
Engineered Hardware & Custom Assembly Solutions
Direct from our ISO 9001 certified manufacturing plant in Shenzhen, tailored for medical electronics, industrial automation, and rugged computing in Costa Rica.
14+
Years International OEM/ODM Export Experience
24h
Rapid DFM Feedback & Quotation Turnaround
±0.05mm
Laser Microvia & Fine Pitch SMT Precision
100%
AOI, X-Ray & Electrical Testing Prior to Air Freight
Technical Whitepaper & Strategic Sourcing Guide
High-TG HDI PCB Engineering: Mitigating Tropical Climate Delamination & Meeting Free Zone SMT Standards
Costa Rica has firmly established itself as Latin America’s silicon republic and biomedical manufacturing beacon. Operating out of key economic nodes like the Coyol Free Zone (Alajuela), BES Free Zone, and Global Park (Heredia), tier-1 multinational contractors and localized OEMs face rigorous environmental and operational challenges. Electronics deployed in the Central Valley, coastal marine installations near Puerto Caldera and Moín, or within hyper-critical medical cleanrooms demand zero-failure hardware interconnects. As a specialized China turnkey assembly partner, Shenzhen VUKO Electronics engineers high glass-transition temperature (High-TG ≥ 170°C) High-Density Interconnect (HDI) circuit boards built strictly to withstand thermal shock, persistent tropical relative humidity (RH > 85%), and intensive operational cycles.
"For Costa Rican engineers and procurement managers under PROCOMER free trade zone regimes, circuit board durability is not merely about mechanical interconnects. It hinges on the thermomechanical stability of the base epoxy matrix during RoHS-compliant lead-free reflow (reaching peaks of 260°C) and long-term dielectric performance in non-climate-controlled Central American ambient settings."
♦ Glass Transition Temperature (Tg) and Material Reliability in Tropical Climates
The glass transition temperature (Tg) designates the physical temperature boundary where the cured epoxy substrate shifts from a rigid, glassy state into a compliant, viscoelastic structure. Standard FR-4 laminates typically possess a low Tg of 130°C to 140°C. Under repeated industrial thermal cycling, or during modern lead-free wave and reflow soldering operations, the Z-axis Coefficient of Thermal Expansion (Z-CTE) of standard material expands dramatically (often exceeding 60-70 ppm/°C post-Tg). In microvia geometries and plated through-holes (PTH), this rapid dimensional expansion strains copper barrel walls, precipitating micro-cracking, barrel barrel separation, and unrecoverable field intermittency.
Shenzhen VUKO Electronics utilizes premium Grade-A copper-clad laminates (such as Shengyi S1000-2, ITEQ IT-180A, and Isola 370HR) maintaining Tg values exceeding 170°C to 180°C, accompanied by high decomposition temperatures (Td ≥ 345°C) and T288 delamination resistance times surpassing 30 minutes. In Costa Rica’s distinct dual-season climate—where wet equatorial conditions elevate humidity absorption in plastic and composite materials—High-TG substrates fundamentally suppress moisture absorption rates (water uptake ≤ 0.12%). This entirely mitigates 'popcorning' failures, inner-layer conductive anodic filament (CAF) degradation, and pad lifting during multi-stage surface mount assembly (SMT).
| Engineering Parameter | Standard FR-4 Specification | VUKO High-TG HDI Industrial Grade | Costa Rica Application Benefit |
|---|---|---|---|
| Glass Transition Temp (Tg) | 130°C – 140°C (DMA) | ≥ 170°C – 180°C (DSC/TMA) | Withstands lead-free 260°C reflow without structural warping. |
| Z-Axis CTE (50°C to 260°C) | 4.5% – 6.5% total expansion | ≤ 2.2% – 2.8% low expansion | Prevents PTH copper fatigue in continuous medical & industrial monitors. |
| Time to Delamination (T288) | < 5 – 10 minutes | ≥ 30 to 45 minutes | Zero delamination across double-sided multi-cycle SMT passes. |
| Moisture Absorption Rate | 0.25% – 0.35% (by weight) | ≤ 0.10% – 0.13% | Immunity to humidity-induced blistering in San José/Cartago wet seasons. |
| Microvia Technology | Mechanical Drill ≥ 0.20mm | UV/CO2 Laser 0.075mm – 0.10mm | Enables 0.35mm/0.4mm ultra-fine pitch BGA integration (IoT/SBCs). |
| Via Filling Chemistry | Open / Solder Mask Plugged | Copper Clad VIPPO / Resin Filled | Planar pad surface for high-density components and superior heat sinks. |
♦ High-Density Interconnect (HDI) Architecture: Any-Layer & Microvia Mastery
As next-generation medical wearables, smart agricultural soil probes, and industrial IoT telematics compress extensive processing cores into miniaturized chassis, conventional mechanical multi-layer drilling becomes a physical spatial bottleneck. HDI fabrication utilizes microvia technology drilled via pulsed UV and CO2 lasers, producing aspect-ratio controlled blind and buried vias with diameters as low as 75 μm (0.003 inches). Our production floor in Shenzhen executes sequential lamination cycles supporting 1+N+1, 2+N+2, and complex Any-Layer (ELIC) HDI architectures.
Furthermore, to empower dense surface mount packaging—such as 0.4mm pitch ball grid arrays (BGAs), wafer-level chip scale packages (WLCSP), and 0201/01005 passives—VUKO employs automated Via-in-Pad Plated Over (VIPPO) processing. By filling microvias with thermally conductive non-conductive epoxy resins or electroplated solid copper, followed by planarization and cap plating, our lines provide an impeccably smooth copper surface. This eliminates solder scavenging during reflow, guarantees uniform solder fillet formation, and enhances RF signal integrity by eliminating unterminated copper stub antennas that otherwise disrupt Bluetooth 5.2, Wi-Fi 6E, and LoRa communications.
Regional Integration
Localized PCB & PCBA Engineering Applications Across Costa Rica
From Free Zone (Zona Franca) medical device contract manufacturing to distributed agro-industrial telemetry across Guanacaste and Limón.
MedTech & Life Sciences (Coyol & Heredia Free Zones)
Costa Rica is a premier exporter of medical equipment. VUKO supplies IPC Class 3 compliant High-TG multilayer rigid-flex circuits and miniaturized HDI boards for patient monitors, surgical handheld electronics, laparoscopic controllers, and infusion pump sub-assemblies. With biocompatible ENIG/immersion silver surface plating, our boards ensure signal fidelity and zero particulate contamination under cleanroom assembly protocols.
Agro-Industrial IoT & Precision Farming (San Carlos & Guanacaste)
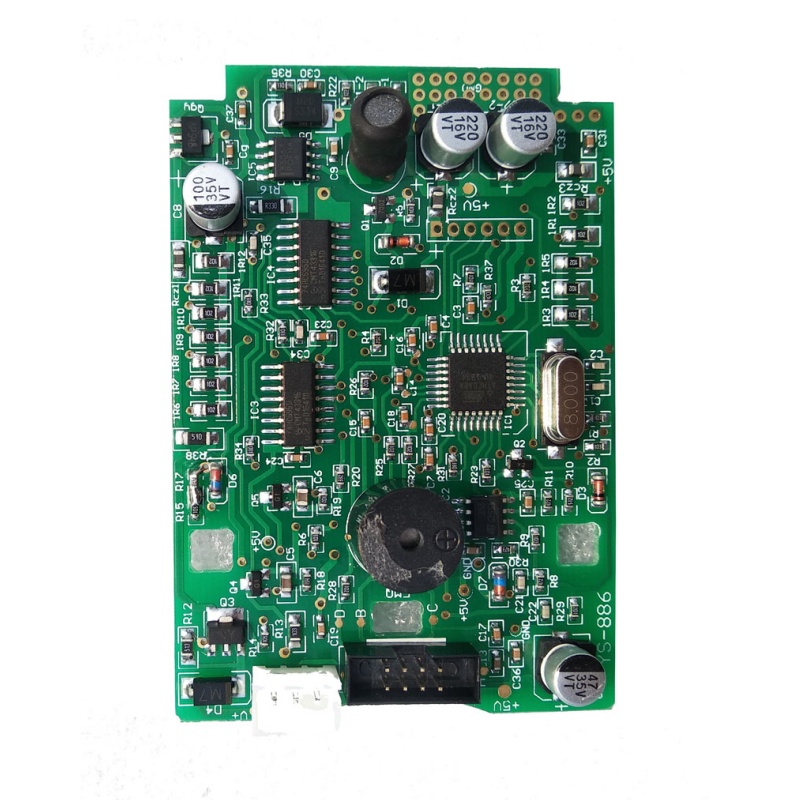
Deployments in sugarcane plantations, coffee mills, and pineapple packaging plants require sensory electronics capable of operating through extreme humidity fluctuations, soil acidity, and direct sun exposure. Our conformal-coated IoT sensor PCBAs and BLDC motor controller assemblies power solar-connected remote irrigation controllers, chemical dosage valves, and LoRaWAN long-range microclimate telemetry networks.
Renewable Energy & Decarbonization Grids (ICE & Distributed Solar)
Aligned with Costa Rica’s national mandate for 99%+ renewable electrical generation, our heavy copper boards (2 oz to 6 oz copper weight) and high-thermal aluminum MCPCBs serve grid-tied solar microinverters, wind turbine pitch-actuator drives, and smart energy sub-metering infrastructure installed across San José and Cartago municipal utility grids.
Industry 4.0 & Nearshoring Dynamics
Strategic Sourcing Trends Shaping Costa Rica's Hardware Ecosystem
Navigating nearshoring growth, US-China-Central America supply chain logistics, and component resilience.
Nearshoring Integration with North American Tech
As multinational original equipment manufacturers relocate secondary and tertiary design lines from Asia directly into Costa Rica to leverage CAFTA-DR trade advantages, local engineering teams require rapid prototyping pipelines. Our Shenzhen factory acts as the ultra-fast back-end accelerator, turning complex 8-to-16-layer HDI prototypes around within 5 to 7 working days, air-shipping directly to San José (SJO).
Supply Chain De-risking & Full Turnkey Kitting
Costa Rican manufacturing entities often face procurement hurdles when sourcing active semiconductors and ultra-low ESR passives in fragmented volume tiers. VUKO solves component shortages by leveraging Shenzhen's tier-1 authorized supply pipeline, delivering turnkey BOM fulfillment with certified origin tracking, obsolescence forecasting, and drop-in alternate qualifications.
Transition Toward Harsh-Environment Smart HMI Panels
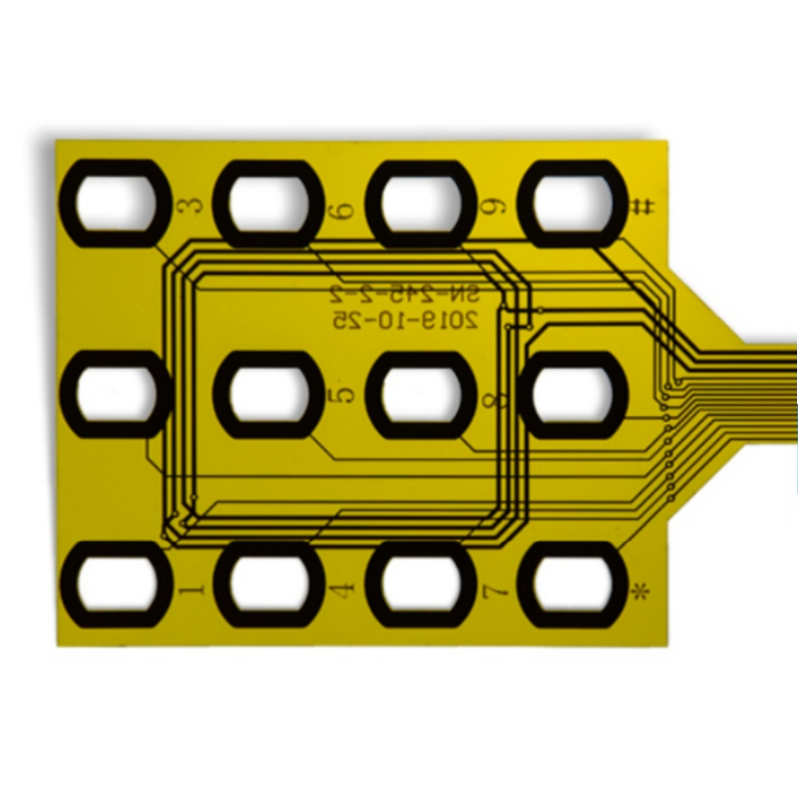
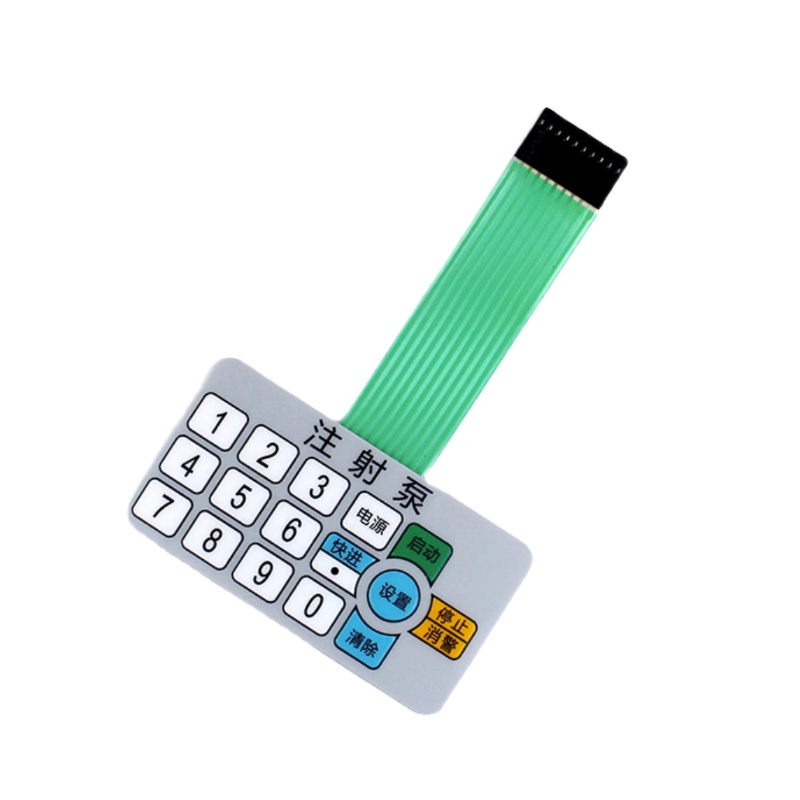
Traditional mechanical switches degrade rapidly under coastal salinity and constant tropical humidity. Costa Rican equipment builders are aggressively transitioning toward hermetically sealed IP67 tactile membrane switches, graphic overlays utilizing 3M 467/468MP adhesives, and embedded LED backlighting suited for humid sterilization or washdown sanitation regimes.
Enterprise Credentials
Why Engineering Teams Partner with Shenzhen VUKO Electronics
Combining complete electronics fabrication under one roof with uncompromised quality assurance and financial order protection.
Alibaba Verified & Trade Assurance
Over 14+ years of verified onsite credentials. Orders placed via Trade Assurance guarantee 100% on-time dispatch protection and secure Escrow escrow handling, removing cross-border trade friction for Costa Rican purchasing departments.
100% Multistage Quality Control
Every bare PCB is subjected to bare-board flying probe or bed-of-nails electrical testing. Turnkey PCBA undergoes inline Solder Paste Inspection (SPI), Automated Optical Inspection (AOI), 3D X-Ray for BGA/QFN void analysis, and functional bench test procedures.
Pre-Manufacturing DFM Engineering
Within 24 hours of file receipt, our senior engineering group executes deep Design for Manufacturability (DFM) reviews, checking copper balance, annular rings, trace-to-edge clearances, aspect ratios, and thermal relief configurations.
True Low-MOQ Turnkey Assembly
We eliminate pilot run barriers. Prototypes and pilot NPI batches start from just 5 pieces, scaling frictionlessly to monthly production schedules exceeding 100,000 units with unified BOM component consistency.
Procurement Guidance
Frequently Asked Questions for Costa Rica Importers
Direct answers regarding customs clearance, DUA logistics, Free Trade Zone compliance, and technical file handling.
How do you handle shipping, Incoterms, and customs import documentation into Costa Rica?
We routinely ship via express air courier (DHL Express, FedEx, UPS) directly into Juan Santamaría International Airport (SJO) in Alajuela or Tobias Bolaños (SYQ). Transit time from our Shenzhen factory is typically 4 to 6 business days. For commercial bulk cargo, consolidated air freight and ocean freight through Puerto Caldera (Pacific) or Port of Moín (Caribbean) are supported under DAP, FOB, or CIF Incoterms. We provide full commercial invoices, packing lists with precise HS codes (e.g., 8534.00 for bare PCBs, 8537.10 for PCBA), and Certificates of Origin to streamline your Agencia de Aduanas (customs broker) filing the DUA (Documento Único Aduanero).
Can VUKO ship directly to companies operating under Costa Rica's Free Trade Zone (Zona Franca) regime?
Yes. A significant volume of our shipments serves corporations in Coyol Free Zone, UltraPARK, and Global Park operating under Law 7210 (Régimen de Zona Franca). We coordinate directly with your designated logistics forwarding agent or internal customs compliance team to ensure commercial invoices are correctly declared for duty-exempt import status under local PROCOMER guidelines.
What engineering documentation is required to quote a complete turnkey High-TG HDI PCBA project?
To provide an itemized quote and perform a complimentary DFM analysis, please submit:
- Gerber Data: RS-274X or ODB++ format including drill files, layer stack-up definitions, and fabrication notes.
- Bill of Materials (BOM): Formatted in Excel with manufacturer names, complete Manufacturer Part Numbers (MPNs), reference designators, and approved alternative parts.
- Centroid / Pick-and-Place File: X-Y coordinates, rotation, and board side (top/bottom) data.
- Testing Directives: Functional test diagrams, firmware flash instructions, and conformal coating requirements (if applicable).
How do you safeguard electronics against moisture degradation during transit to Costa Rica?
Recognizing the high humidity conditions upon arrival in Costa Rica, all bare boards and PCBA modules are baked post-production to evacuate internal moisture, then hermetically heat-sealed inside multi-layer ESD-shielded vacuum barrier bags accompanied by active desiccant packs and calibrated Humidity Indicator Cards (HIC). This satisfies IPC/J-STD-033 standards, guaranteeing that boards arrive dry and ready for immediate SMT or enclosure integration.
Can you clone or reverse-engineer legacy electronic control boards used in industrial machinery?
Yes. Many industrial processing plants in Cartago and San José rely on imported machinery whose original OEM controller cards are discontinued. By sending a functional physical sample to our Shenzhen engineering lab, we can decapitate components, scan internal copper layers, reconstruct Gerber files and complete electrical schematics, and supply updated modern drop-in replacements with improved High-TG reliability.
Launch Your High-TG HDI PCBA Build Today
Send your Gerber files and BOM to our engineering desk. Receive an exhaustive DFM file check, component lead-time verification, and complete competitive quotation within 24 hours.