Integrated Overlays, Flexible Interconnects & Electronic Assemblies
Engineered to withstand rigorous wipe-down cycles, repetitive mechanical actuation, and harsh electro-mechanical operating environments throughout Massachusetts innovation corridors.
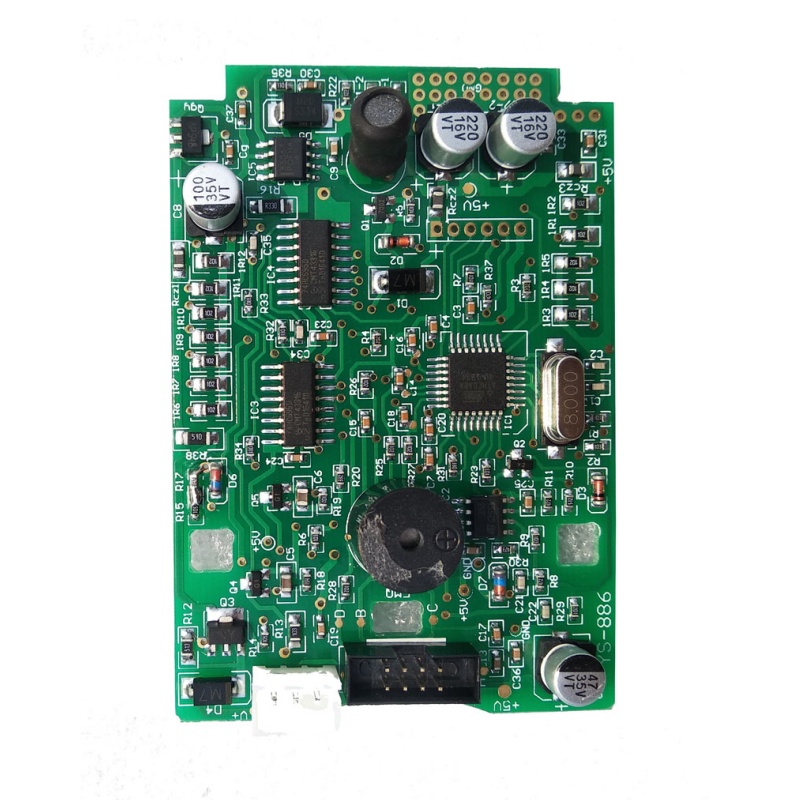
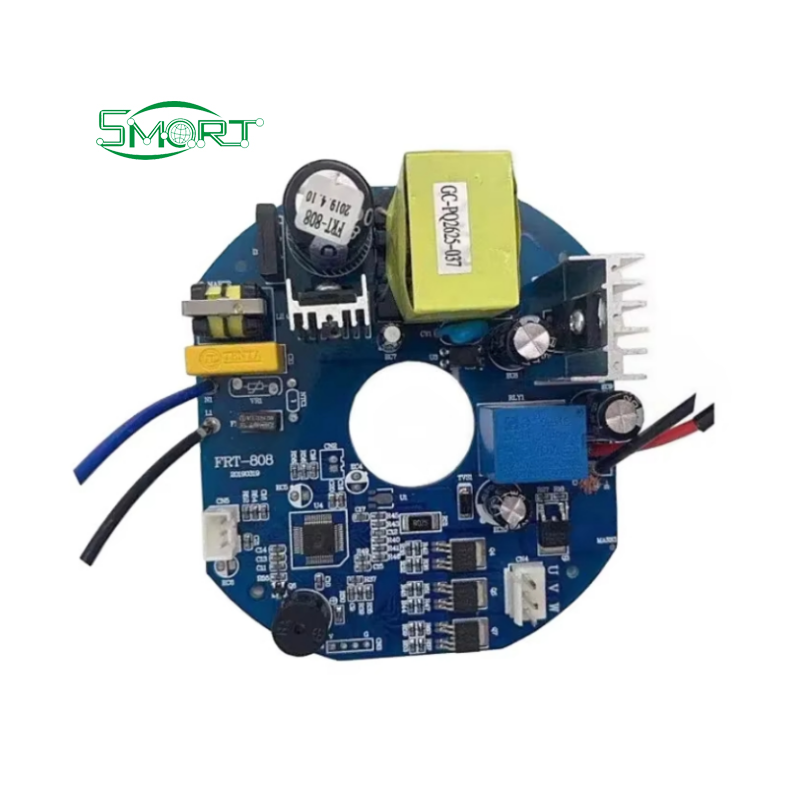
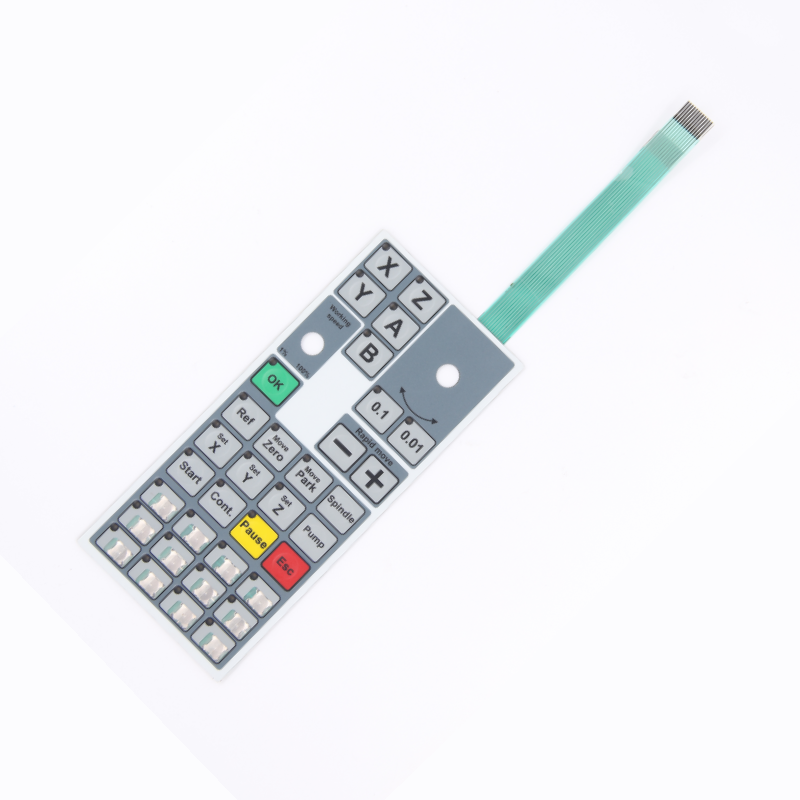
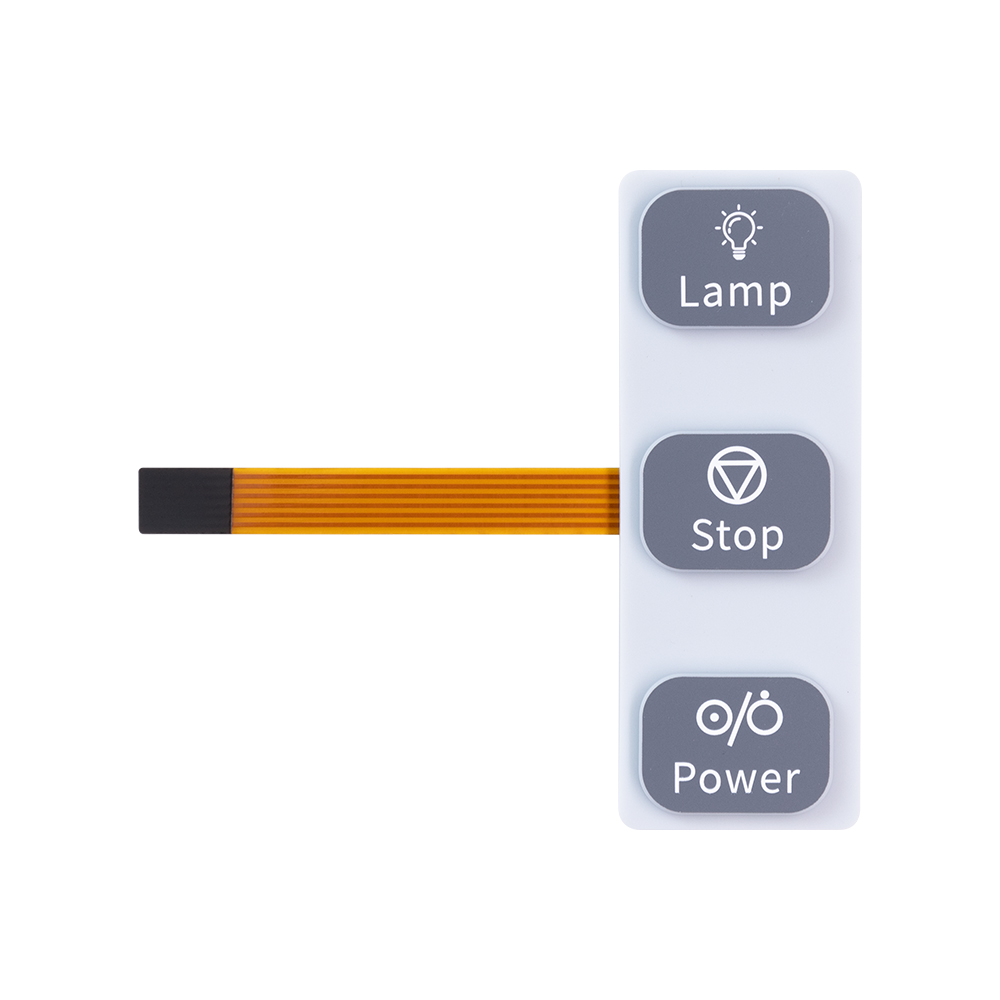
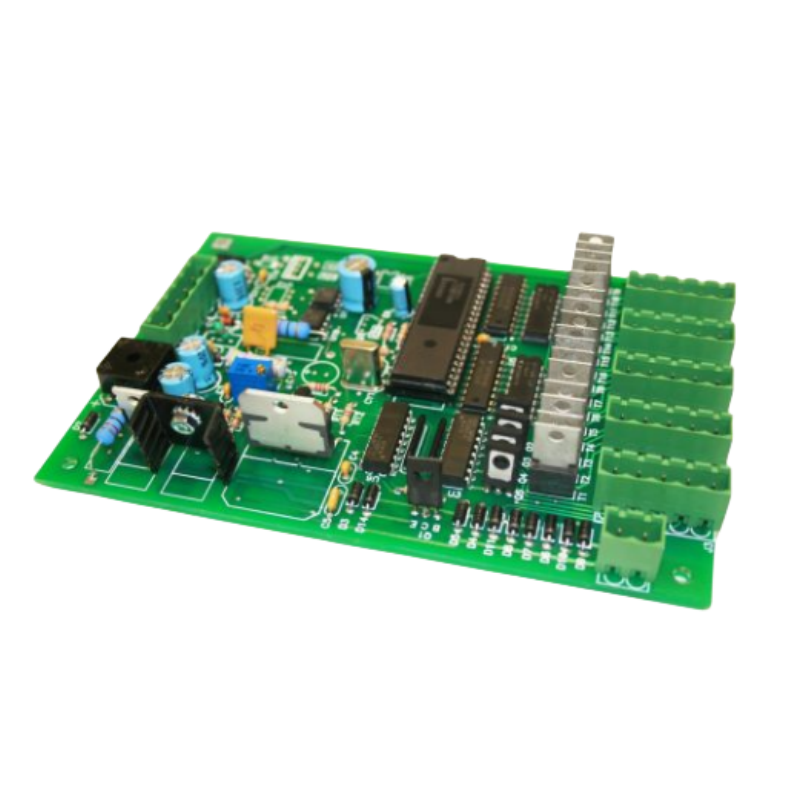
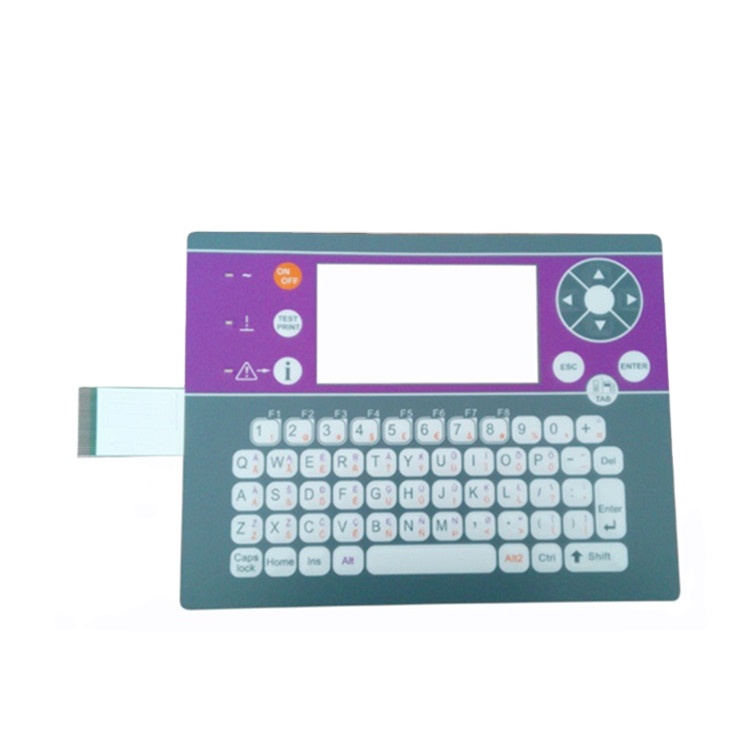
Precision Keyboard Overlays & HMI Assemblies for Boston's Advanced Hardware Ecosystem
As the Greater Boston metropolitan area solidifies its global leadership across biotechnology, medical device fabrication, analytical lab instrumentation, and defense robotics, the demand for resilient, chemically inert, and ergonomically calibrated human-machine interfaces (HMI) has grown exponentially. From research labs in Cambridge's Kendall Square to high-throughput automation corridors along Route 128 and Interstate 495, mechanical engineers and product designers face a critical challenge: finding a high-precision wholesale keyboard overlay factory in China that delivers medical-grade execution, sub-millimeter tolerances, and turnkey assembly reliability without the inflated costs of domestic intermediaries.
Shenzhen VUKO Electronics operates at the epicenter of the world's most consolidated electronics manufacturing cluster, bridging Tier-1 material science with responsive contract manufacturing. Unlike simple digital print shops, we operate a vertically integrated production infrastructure covering precision sub-surface screen and digital printing, laser die-cutting, embossing, metal dome array population, cleanroom adhesive lamination, and full PCBA/FPC integration. By uniting bare board fabrication, electronic component sourcing, SMT assembly, and custom faceplate manufacturing under a single roof, we eliminate multi-vendor friction for Boston hardware engineers moving swiftly from prototype validation to volume manufacturing.
Optical Sub-Surface Printing
Inks and graphic legends are deposited directly onto the second surface of transparent substrates. This ensures that harsh chemical washdowns, abrasive industrial particulate, and constant human thumb actuation will never erode labels, graphic branding, or operational iconography.
Selective Surface Texturing
Engineered UV-curable selective textures produce anti-glare, fine-matte finishes across user-facing surfaces while leaving clear, high-transparency display windows for LCDs, OLEDs, and seven-segment LED readouts with light transmission rates exceeding 91%.
Tactile Feedback Calibration
Utilizing high-cycle stainless-steel metal domes (nickel or gold plated) calibrated from 180g to 450g actuation forces, ensuring crisp tactile feedback even when operated by laboratory personnel wearing heavy nitrile gloves.
Polycarbonate (PC) vs. Biaxially-Oriented Polyester (PET) in High-Duty Applications
Selecting the optimal graphic substrate is fundamental to ensuring that keyboard overlays withstand the environmental stresses characteristic of Boston's cold coastal winters, aggressive sterilization protocols, and industrial floor vibrations. Our engineering team reviews your mechanical enclosure CAD and chemical exposure profile during the initial 24-hour DFM analysis to recommend the right balance of material properties.
| Performance Parameter | Autotex / MacDermid PET (Polyester) | Lexan / Sabic PC (Polycarbonate) | Antimicrobial Polyester (Microban) |
|---|---|---|---|
| Flexural Fatigue Life | > 5,000,000 actuations (Superior flex life) | ~ 100,000 actuations (Prone to stress cracking) | > 5,000,000 actuations (Ideal for medical keypads) |
| Chemical & Solvent Resistance | Exceptional resistance to alcohols, IPA, bleach, acetone | Moderate; vulnerable to aromatic hydrocarbons & ketones | Formulated for hospital disinfectants & quaternary cleaners |
| Operating Temperature | -40°C to +85°C (-40°F to 185°F) continuous | -40°C to +105°C (-40°F to 221°F) continuous | -40°C to +85°C continuous |
| Embossing Retention | Requires thermo-hydro forming for crisp retention | Easily cold/warm embossed; high dimensional stability | Heat-stabilized film retains tactile pillow & rim emboss |
| Best-Fit Boston Application | Biotech lab automation, marine monitors, robotics | Emergency stop faceplates, non-flexing bezels, HVAC | Point-of-care medical carts, surgical diagnostic consoles |
For demanding life sciences equipment, our factory utilizes authentic MacDermid Autotex XE and V650 grade textured polyester films. These substrates incorporate a proprietary hard-coat layer that resists micro-scratching from grit while preventing yellowing when exposed to ambient UV radiation in illuminated clinical environments.
High-Reliability Applications Across the Greater Boston Tech Ecosystem
Tailoring industrial design, ingress sealing, and tactile performance to the distinct regulatory and operating demands of Massachusetts hardware manufacturers.
Biotechnology & Analytical Lab Automation
Boston's premier pharmaceutical and sequencing device manufacturers require overlay keyboards that repel continuous wipe-downs with 70% isopropyl alcohol, dilute sodium hypochlorite, and laboratory reagents. Our sealed PET faceplates paired with 3M 468MP adhesives prevent liquid capillary ingress, maintaining sterile chamber integrity.
Autonomous Mobile Robots & Industrial Teach Pendants
Robotics startups throughout the Route 128 corridor demand ruggedized, impact-resistant keyboard overlays for handheld control units, warehouse automated guided vehicles (AGVs), and drone ground stations. Features include high-actuation metal domes, blind-feel rim embossing, and integral EMI/ESD aluminum shielding.
FDA-Compliant Clinical Diagnostic Equipment
Diagnostic imaging consoles, blood gas analyzers, and patient monitoring carts operating in hospital environments mandate completely flat, anti-microbial keyboard surfaces with zero crevices where pathogens might harbor. We provide Microban-treated graphic overlays with dead-front LED backlighting for intuitive workflow illumination.
Maritime Instrumentation & Coastal Defense Electronics
Deployed on oceanographic research vessels and coastal monitoring buoys, our IP67-rated silicone-gasketed membrane keypads resist dense salt fog, continuous humidity, and sub-zero New England winter freeze-thaw cycles without delamination or contact resistance degradation.
Key Trends Driving Keyboard Overlay Sourcing in New England for 2025–2026
Boston's engineering community is shifting rapidly away from clunky discrete mechanical pushbuttons toward sleek, unified, and ultra-durable solid-state HMI solutions. Hardware teams balancing rapid time-to-market with rigorous reliability metrics are gravitating toward several clear architectural patterns:
Capacitive Touch Overlays with Haptic Integration
Eliminating moving mechanical parts entirely, leading medical and cleanroom device developers in Massachusetts are specifying capacitive touch sensor layers printed behind glass or thick polycarbonate overlays, backed by piezoceramic actuators for tactile confirmation.
Dead-Front Secret-Until-Lit Graphics
High-end lab devices require clutter-free control surfaces. Utilizing calibrated translucent inks with precise opacity densities, warning symbols and secondary function keys remain invisible until illuminated from behind by surface-mount LEDs on the carrier PCBA.
FPC Tail Upgrades from Carbon Paste
To eliminate silver migration risk and high trace resistance over long interconnect runs, Boston OEMs increasingly demand Polyimide (PI) Flexible Printed Circuit (FPC) tails with gold-plated ZIF contacts, replacing traditional screen-printed silver ink flex leads.
End-to-End Manufacturing Prowess: From Shenzhen Factory to Boston Facility
Combining 14+ years of audited factory direct capability with seamless international shipping, strict IPC workmanship, and unmatched multi-technology integration.
Direct Shenzhen Manufacturer, Not a Trading Broker
As an Alibaba.com Onsite-Verified manufacturing enterprise with our own SMT lines, CNC drilling, screen-printing cleanrooms, and testing facilities in Shenzhen, we provide total transparency, direct engineer-to-engineer communication, and zero middleman markups.
Turnkey PCB + PCBA + Overlay Integration
Why juggle a graphic overlay printer in one region and a board assembler in another? We fabricate bare PCBs (rigid, HDI, aluminum metal-core), mount electronic components, program ICs, and bond the finished custom keyboard overlay in one synchronized manufacturing pipeline.
Agile Low MOQ Starting at Just 5 Pieces
Boston's vibrant accelerator ecosystem (Greentown Labs, MassChallenge, MIT engine spinouts) requires rapid physical prototyping. We support early-stage DVT and EVT hardware milestones with sample runs as small as 5 pieces before scaling seamlessly to 50,000+ units.
24-Hour DFM Engineering & Quotation Turnaround
Send your DXF, DWG, Adobe Illustrator vector art, Gerber RS-274X, or component BOM. Our English-speaking bilingual engineering team reviews mechanical tolerances, switch circuit matrixes, and trace routing, returning actionable feedback within 24 business hours.
Rigorous Multi-Stage Quality Assurance
Every membrane switch panel and assembled board undergoes 100% automated optical inspection (AOI), electrical open/short continuity testing on flying probe machines, actuation force testing, and environmental thermal cycling. All materials satisfy RoHS and UL 94V-0 flammability standards.
Reliable Express Air Freight Direct to Boston (BOS)
With established tier-one logistics partnerships across DHL Express, FedEx, and UPS Air, our finished production cartons clear US Customs effortlessly, reaching Boston, Cambridge, Quincy, Waltham, and Worcester within 3 to 5 business days after inspection release.
Frequently Asked Questions by Boston Hardware Engineers & Sourcing Managers
Addressing critical commercial, technical, and regulatory questions regarding keyboard overlays and HMI production in China.
What engineering design files are needed to quote and build a custom keyboard overlay?
How does VUKO ensure color fidelity and consistency with our brand guidelines in Massachusetts?
What adhesives are recommended for mounting overlays to cast aluminum or powder-coated plastic enclosures?
How are Boston-bound shipments packaged and protected against moisture and electrostatic discharge during air transit?
What are typical lead times for prototypes versus medium-volume production delivered to Greater Boston?
Can you integrate custom surface-mount LEDs and display windows into the overlay assembly?
Initiate Your Custom Keyboard Overlay Project Today
Connect directly with Shenzhen VUKO's senior HMI engineering team. Upload your artwork, mechanical enclosure drawings, or PCBA Gerber files for a comprehensive DFM audit, material consultation, and competitive wholesale factory quotation within 24 hours.
Inquire Now