Industrial Membrane Overlays, Flexible Interconnects & Electronic Assemblies
Direct factory supply from Shenzhen VUKO Electronics for Albanian industrial systems integrators, hardware developers, and panel builders.
The Albanian Market for Industrial Keyboard Overlays & HMI Systems
Navigating material selection, ingress protection standards, and cross-border supply chain integration between Shenzhen production lines and Albania's expanding industrial corridor.
Albania's domestic industrial base has entered a major modernization cycle. Fueled by European supply chain nearshoring initiatives, modernization of coastal maritime infrastructure around Durrës and Vlorë, intensive capital projects in mineral processing (chromium, copper, and ferrochrome), and modernization across municipal water and agricultural automation, the regional demand for robust Human-Machine Interfaces (HMI) has surged exponentially. Industrial equipment deployed across Albania faces rigorous operating realities: Mediterranean coastal environments laden with salt-fog and airborne particulate, intense seasonal temperature fluctuations between the alpine northern highlands and humid southern plains, and heavy mechanical vibration in mining extraction facilities. Standard off-the-shelf control panels and commercial membrane keyboards fail rapidly under these stressors, suffering from graphic delamination, UV yellowing, seal ingress, and intermittent switch contact resistance.
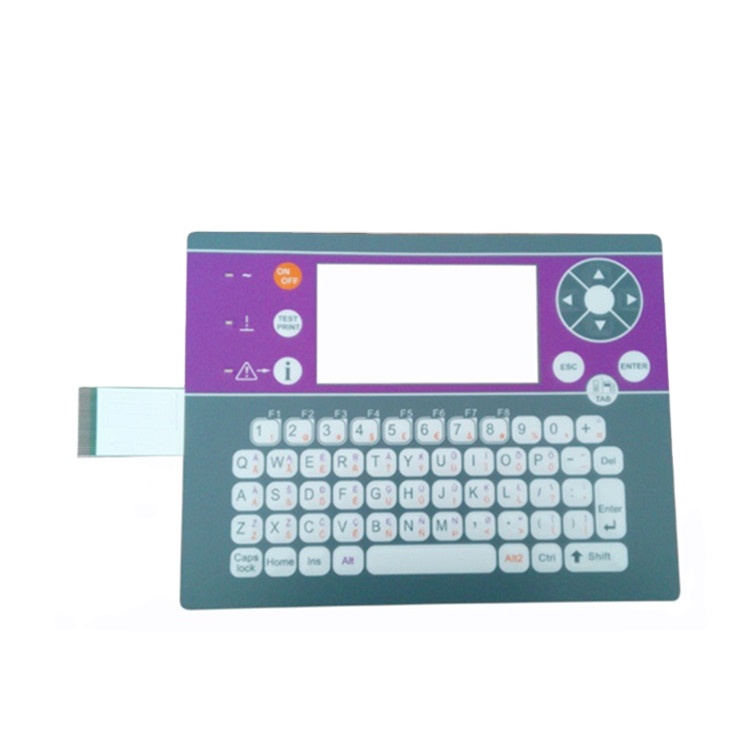
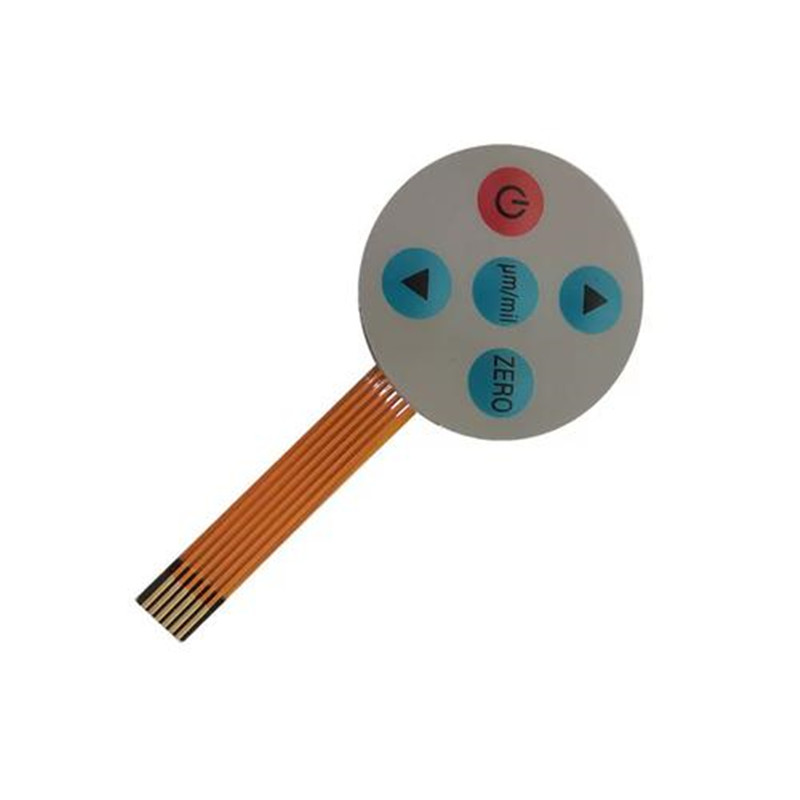
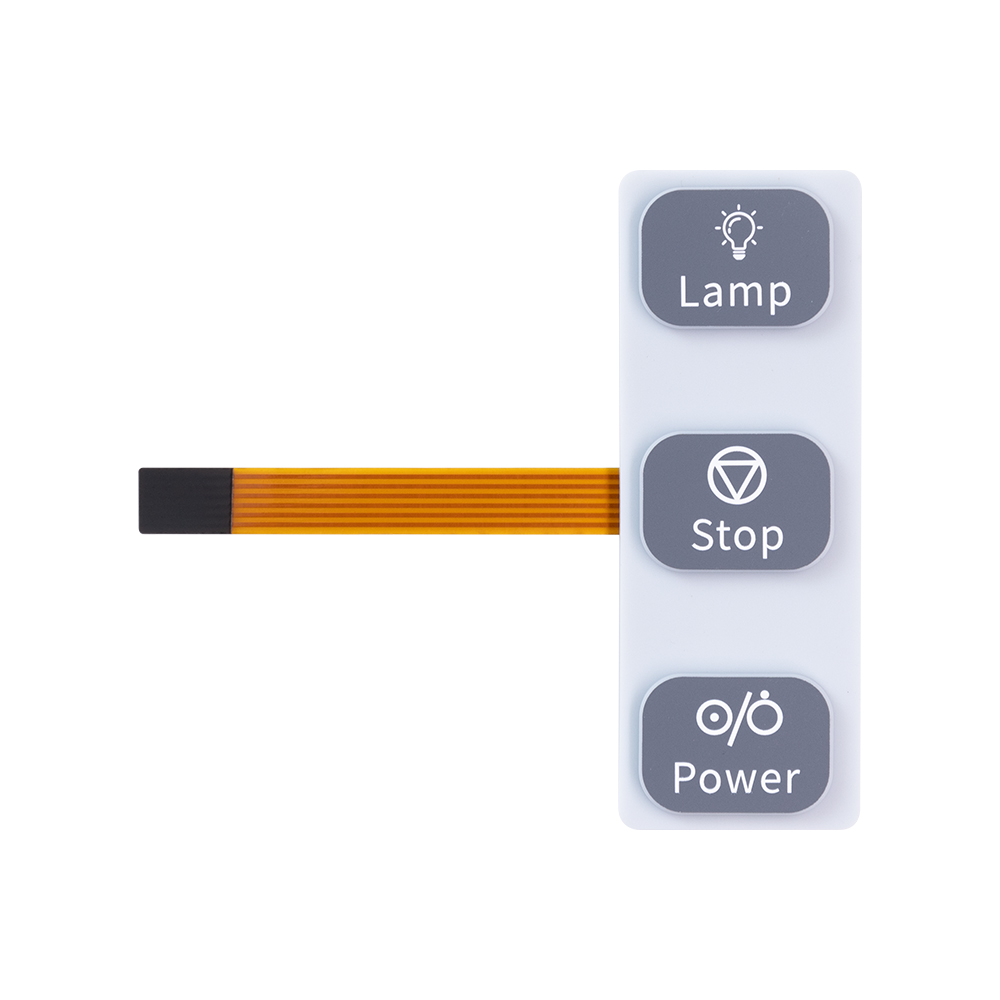
A custom-engineered keyboard overlay (or graphic overlay integrated into a multi-layer membrane switch matrix) serves as the primary environmental barrier and operational interface between human operators and the underlying electronics. For engineering teams and industrial procurement directors operating across Tirana, Durrës, Shkodër, and Elbasan, identifying dependable keyboard overlay factories & suppliers capable of delivering precision tolerances, industrial-grade substrate durability, and cost-effective low-to-medium volume manufacturing is a decisive operational imperative. Shenzhen VUKO Electronics Co., Ltd. provides the critical bridge: combining rapid engineering reviews, Class 10,000 cleanroom screen printing, precision die-cutting, automated surface-mount assembly on flexible polyimide circuits, and rigorous environmental testing under an ISO 9001 certified quality framework.
Substrate Engineering
Sub-surface reverse printing safeguards visual typography against chemical washdown and physical abrasions.
- Autotex® XE / EBG / EBA Polyester (PET): Unmatched flexural endurance (>5 million switch cycles). Formulated for UV resistance, outdoor longevity, and extreme chemical defense against industrial solvents, hydraulic fluids, and caustic cleaners.
- Sabic Lexan® 8010 Polycarbonate (PC): Exceptional clarity, optical grade LED/LCD display windows, high dielectric strength, UL 94V-0 or 94V-2 flame retardant ratings. Optimal for indoor control instrumentation.
- Anti-Glare & Anti-Microbial Coatings: Textures ranging from fine velvet to heavy grain, coupled with silver-ion antimicrobial top-coats for medical monitors and commercial food packaging machinery.
Environmental Sealing
Multi-layer perimeter pressure adhesive channels designed to achieve IP65, IP67, and NEMA 4X compliance.
- 3M 467MP / 468MP Adhesives: High-performance acrylic transfer tapes for smooth powder-coated metal, stainless steel, and rigid plastic enclosures. Outstanding shear resistance across -40°C to +150°C.
- 3M 300LSE Low Surface Energy Bonds: Engineered specifically for bonding to polypropylene, polyethylene, and powder-coated textured aluminum cabinets common in Albanian telecom nodes.
- Waterproof Perimeter Gaskets: Custom laser-cut silicone or closed-cell polyurethane foam barriers that block moisture penetration during high-pressure jet washdowns.
Tactile & Circuit Ergonomics
Crisp sensory actuation feedback tailored for glove-wearing machine operators and field technicians.
- Stainless Steel Metal Domes: Nickel-plated or gold-plated snap domes (4-leg, round, or oblong), actuation force calibrated from 250g to 500g, delivering decisive tactile confirmation.
- Pillow & Rim Embossing: Hydro-formed or hot-press tooling creates distinct tactile boundaries around keycaps, enabling blind key location in dimly lit industrial environments.
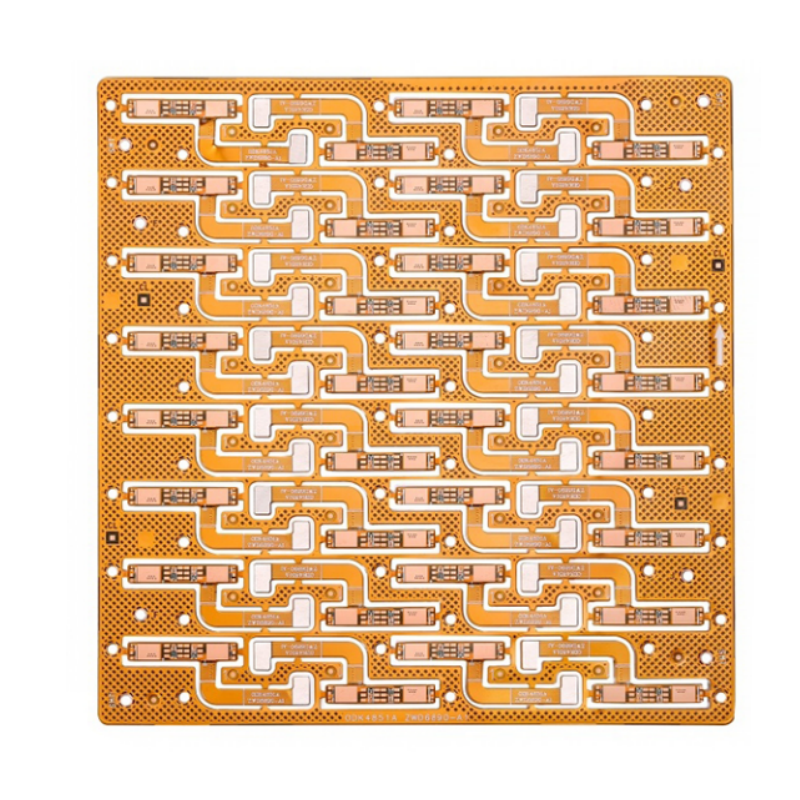
- FPC Copper vs. Silver Flake Circuits: Ultra-low trace resistance flexible printed circuits (FPC) with polyimide stiffeners, eliminating silver migration risks in sustained humid climates.
| Performance Parameter | Autotex® XE Polyester (Industrial) | Lexan® Polycarbonate (PC) | FPC Copper Membrane Switch | Silver Conductive Screen-Print |
|---|---|---|---|---|
| Flexural Fatigue Life | > 5,000,000 actuations | < 100,000 actuations (brittle) | > 10,000,000 actuations | > 1,000,000 actuations |
| Outdoor UV Stability | Excellent (Tested 2,000h Xenon Arc) | Degrades / Yellows unless UV-stabilized | Encapsulated beneath overlay | Encapsulated beneath overlay |
| Chemical / Solvent Resistance | Resistant to acids, alkalis, alcohols, fuels | Prone to stress cracking with solvents | Inert copper encased in polyimide | Susceptible to silver migration over time |
| Loop Trace Resistance | N/A (Graphic overlay substrate) | N/A (Graphic overlay substrate) | < 1.0 Ω (High electrical efficiency) | 10 Ω - 150 Ω (Length dependent) |
| Standard Thickness Range | 0.13 mm - 0.28 mm | 0.125 mm - 0.50 mm | 0.057 mm - 0.20 mm | 0.075 mm - 0.125 mm (PET base) |
| Operating Temperature | -40°C to +85°C | -30°C to +105°C | -40°C to +125°C | -20°C to +70°C |
Industrial & Infrastructure Applications in the Albanian Market
Field-tested hardware configurations engineered to withstand the unique environmental and mechanical demands of Albania's economic hubs.
Port of Durrës & Coastal Marine Systems
Marine electronic control consoles, cargo crane hoist pendants, and bilge pump controllers require complete immunity to saline humidity, sea spray, and direct sun exposure. Using UV-inhibited Autotex XE polyester combined with high-tack 3M 468MP waterproof gaskets guarantees IP67 seal integrity, preventing corrosion of internal contacts.
Mineral Processing & Heavy Metallurgy
From the chrome mining reserves in Bulqizë to smelting plants in Elbasan, heavy machinery is subjected to airborne slag particulate, intense acoustic shock, and abrasive handling. Our embossed metal dome overlays provide tactile click feedback that can be felt effortlessly through heavy operator work gloves, encased in thick anti-scratch polycarbonate.
Smart Energy Metering & Substation SCADA
Albania's national grid operator (OSHEE / OST) is upgrading municipal transformers and remote telemetry units (RTUs). Our overlays integrate transparent LCD windows with low-birefringence clarity, anti-glare finishes, and custom EMI/RFI shielding grids that suppress electromagnetic interference from high-voltage switchgear.
Healthcare & Clinical Laboratory Devices
Modern clinics and hospital labs across Tirana utilize specialized diagnostic centrifuges, patient monitoring terminals, and blood gas analyzers. These HMI surfaces feature seamless, crevice-free overlays printed with anti-microbial silver-doped lacquers that endure daily sterilization using ethanol, bleach, and quaternary ammonium compounds.
Emerging Engineering & Sourcing Trends in Albania
Key design vectors driving HMI engineering changes across Southeast Europe through 2026 and beyond.
1. Transition from Mechanical Pushbuttons to Integrated HMI Glass & Membrane Panels: Historically, Albanian electrical cabinets relied on bulky 22mm panel-mount pushbuttons and incandescent pilot lamps. System integrators are rapidly shifting toward thin-profile membrane overlays and capacitive touch switches that integrate embedded SMD micro-LEDs directly within the circuit layers. This migration shrinks cabinet depth by over 60%, decreases assembly labor, and seals the front bezel against moisture ingress.
2. Adoption of Flexible Printed Circuit (FPC) Tails over Silver Flake Wiring: In the sub-Mediterranean climate of central Albania, diurnal temperature cycling creates condensation within unsealed enclosures. Silver conductive paste, when subjected to moisture and continuous DC voltage bias, is susceptible to silver dendrite migration, causing catastrophic short circuits. Tier-1 Albanian developers are increasingly mandating copper-etched FPC circuit layers for all high-reliability applications, taking advantage of VUKO's combined FPC and membrane switch fabrication capabilities.
3. Nearshoring and Fast-Track Prototype Sourcing: As European manufacturing groups establish satellite contract facilities in Albania (leveraging competitive regional logistics and proximity to the EU via Italy and Greece), the requirement for fast engineering iterations has become paramount. Product managers require DFM design verification in 24 hours, functional rapid prototypes within 5 to 7 business days via international air express, and seamless transition to mass production runs with zero tooling mismatch.
The VUKO End-to-End Manufacturing Workflow
Gerber & Art DFM
Color space match (Pantone/RAL), embossing profile feasibility, LED pad isolation checks.
Cleanroom Printing
Class 10,000 sub-surface multi-pass screen printing; optical window lacquer coating.
Die Cut & Emboss
High-precision CNC digital cutting or matched hardened steel die forming for keycaps.
Automated Lamination
Dome placement, spacer bonding, and 3M adhesive stack lamination under controlled pressure.
100% E-Test & Ship
Continuity, insulation resistance (>100MΩ @ 100V DC), tactile force verification, express dispatch.
Frequently Asked Questions for Albanian Sourcing Teams
Essential technical, commercial, and logistics facts for importing custom keyboard overlays and membrane keypads into Albania.
What design files and documentation are required to quote a custom keyboard overlay?
For an accurate and rapid quotation (within 24 hours), please provide:
1. Vector Graphic Artwork: Adobe Illustrator (.AI), CorelDraw (.CDR), or editable high-resolution PDF with typography outlined, defining all graphic elements and color assignments using Pantone Matching System (PMS) or RAL color codes.
2. Mechanical / CAD Drawing: DXF, DWG, or STEP files showing overall panel dimensions, outer cut tolerance (±0.15mm standard), cutouts, transparent LCD/LED display window placements, and embossing profiles (rim, pillow, or dome embossing).
3. Circuit Schematics (for complete membrane switches): Circuit pinout, connector pitch (e.g., 2.54mm or 1.0mm FFC/FPC), LED polarity, and tactile snap dome requirements (diameter and actuation force in grams).
How does VUKO ensure color fidelity and exact matching with our branded enclosures?
We utilize precision spectrophotometers to measure color values (CIE L*a*b* coordinates) during production. Formulations of Marabu® and Nazdar® industrial screen printing inks are matched directly against physical Pantone Formula Guides or client-supplied color chips under standardized D65 lighting booths. For large OEM contracts, we produce hard-proof sample overlay coupons for your engineering approval before running the complete production run.
What are the shipping routes, lead times, and customs clearance protocols for Albania?
Shipments from our Shenzhen facility are commonly routed via:
• Air Express (DHL, FedEx, UPS): 4 to 6 business days directly to Tirana International Airport (TIA - Rinas) or designated customs clearance terminals. Ideal for prototypes, pilot runs, and urgent spare batches.
• Consolidated Air Cargo or Ocean Freight: 25 to 35 days arriving at the Port of Durrës for heavy volume box builds, complete assemblies, and regular quarterly scheduled orders.
All export documentation includes detailed Commercial Invoices, Packing Lists with precise HS Codes (typically 8537.10 or 8538.90 for membrane switch assemblies), and Certificates of Origin to facilitate smooth clearance through Albanian Customs Authority (Dogana Shqiptare).
Can VUKO deliver complete assemblies including PCB/PCBA, plastic housings, and cable harnesses?
Yes. Beyond pure graphic overlays and membrane keypads, VUKO is a full-stack electronics manufacturing services (EMS) provider. We build rigid FR4 PCBs (1-12+ layers), flexible printed circuits (FPC), perform high-speed SMT placement, solder through-hole components, assemble display units, and integrate the complete keyboard overlay onto custom aluminum backing plates or injection-molded plastic bezels. This eliminates multi-vendor coordination risks and delivers a pre-tested, plug-and-play HMI module directly to your assembly line.
What is your Minimum Order Quantity (MOQ) and sample lead time?
We actively support engineering research, device prototyping, and low-volume high-mix industrial machinery. Our minimum order quantity for custom prototype membrane switches and graphic overlays starts at just 5 pieces. Prototyping lead times typically range from 5 to 7 working days post-artwork confirmation. Medium to large batch production runs (500 to 10,000+ units) are normally manufactured in 12 to 18 working days.
Are VUKO membrane switches and overlays compliant with European CE, RoHS, and REACH directives?
All materials—including PET/PC film substrates, conductive silver and carbon inks, 3M bonding adhesives, polyimide coverlays, and solder pastes—comply fully with EU RoHS (Directive 2011/65/EU and amendment 2015/863) and REACH (EC 1907/2006) standards. Full material declarations, flame-retardant certification (UL 94V-0), and independent SGS/TÜV test reports can be supplied upon request for your qualification dossier.
Why Global Hardware Innovators Choose Shenzhen VUKO Electronics
Integrating modern Chinese supply chain agility with stringent international quality assurance standards.
Shenzhen Supply Chain Density
Located at the center of the world's premier electronics manufacturing ecosystem in Shenzhen, Guangdong.
- Immediate access to genuine international brand materials (3M, Sabic, MacDermid Autotype, Nicomatic, Bergquist).
- In-house tooling, CNC laser cutting, screen stencil making, and precision stamping under one unified management system.
- Rapid turnkey component sourcing for microcontrollers, LEDs, buzzers, and connectors without broker markups.
Comprehensive In-House QC
Every production batch undergoes exhaustive multi-point electrical, physical, and environmental verification.
- Actuation & Life Cycle Testing: Automated pneumatic testers cycle tactile metal domes up to 1,000,000+ presses to evaluate contact degradation.
- Automated Optical Inspection (AOI): High-resolution optical scanners verify overlay text printing, registration accuracy, and pinhole-free ink opacity.
- Environmental Chamber Validation: Thermal shock (-40°C to +85°C) and relative humidity testing (95% RH @ 60°C) to detect adhesive delamination early.
Direct Engineer-to-Engineer Support
Zero communication friction with fluent English-speaking technical project managers dedicated to your account.
- Comprehensive Design-for-Manufacturability (DFM) reviews completed within 24 hours of file receipt.
- Proactive recommendations on material substitution to lower production costs while increasing field life.
- Flexible international payment structures backed by Alibaba Trade Assurance for complete transaction safety.
Launch Your Custom Keyboard Overlay Project
Whether you require a rapid prototype of 10 graphic overlays or regular volume manufacturing of IP67 tactile membrane switch panels for the Albanian market, our engineering department is standing by to evaluate your mechanical drawings, optimize your stack-up, and deliver a competitive quote.