High-Reliability Human-Machine Interfaces & PCB Assemblies
Engineered to resist coastal salt fog, intense UV radiation, and heavy humidity cycles across St. John’s, English Harbour, and Codrington.
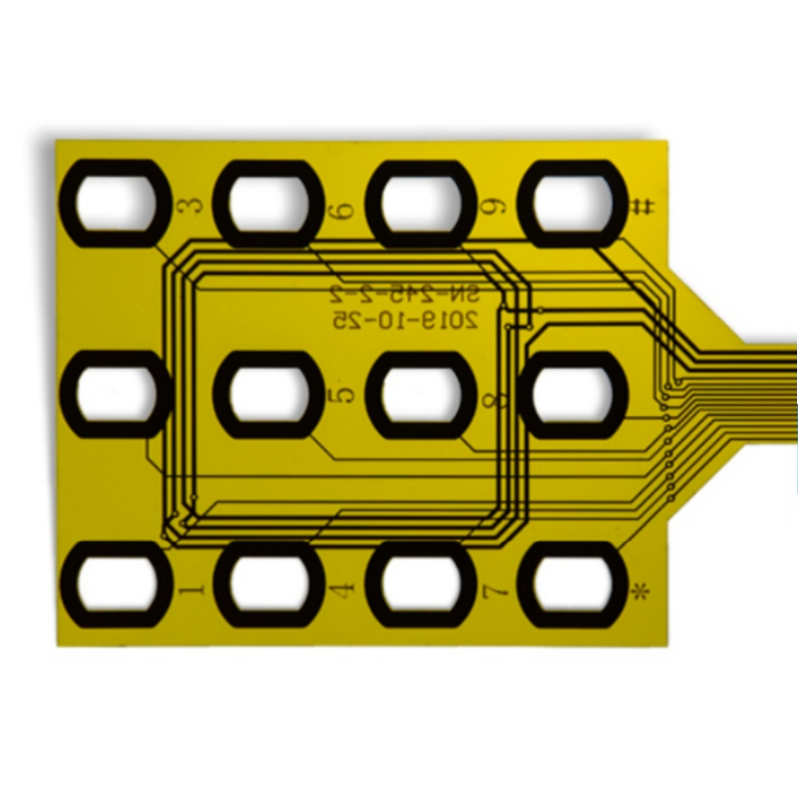
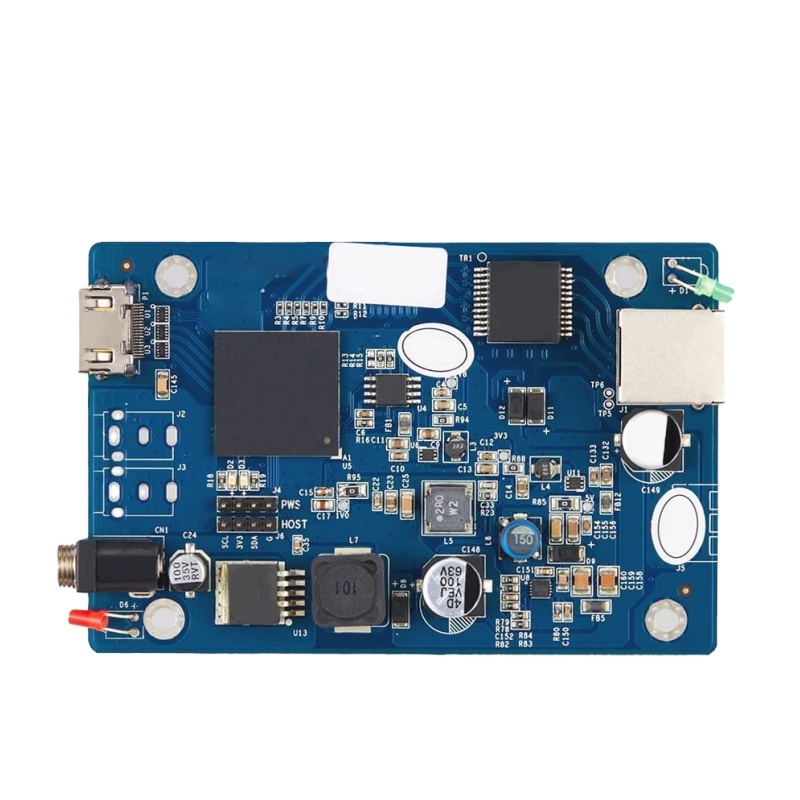
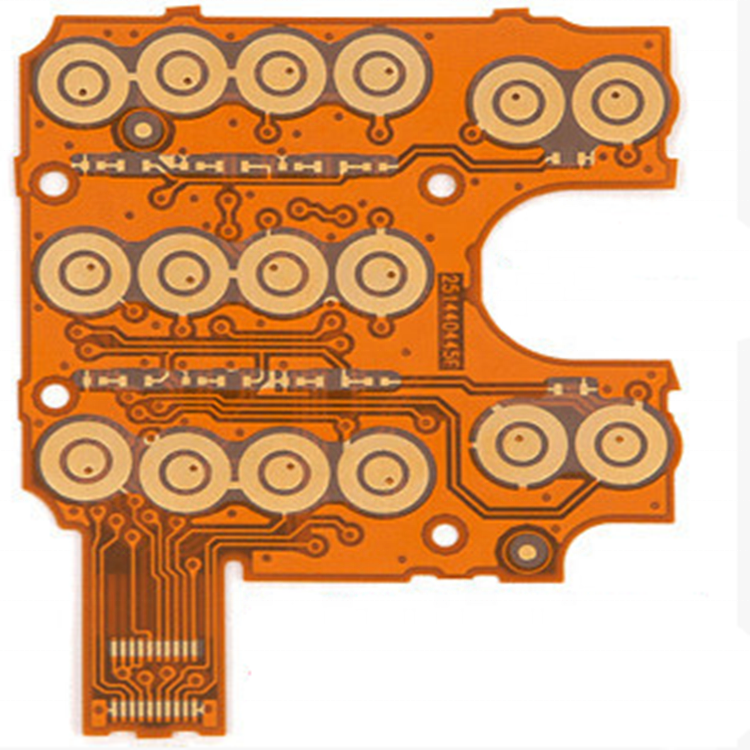
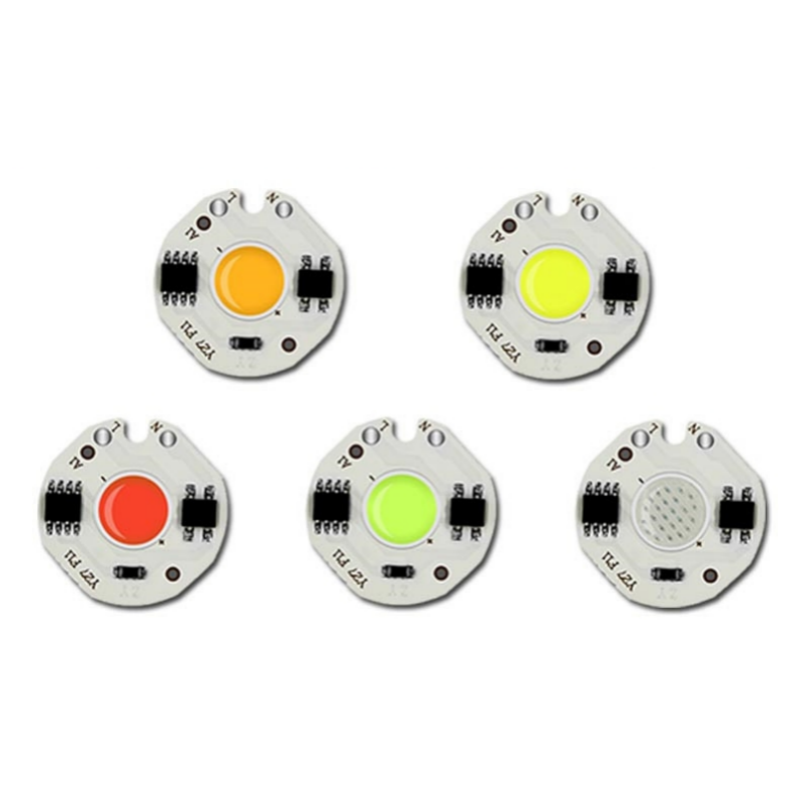
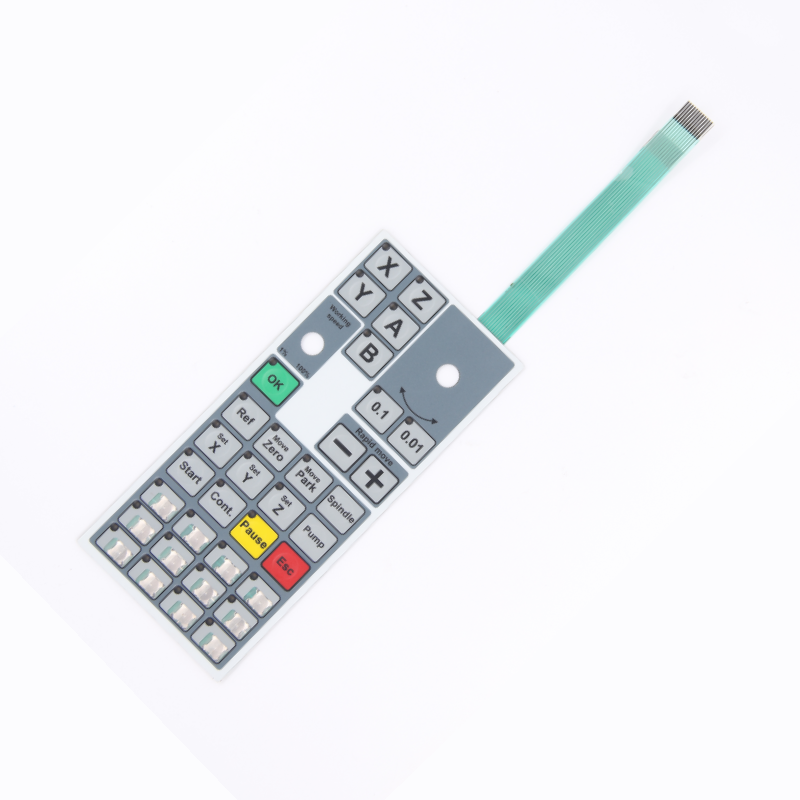
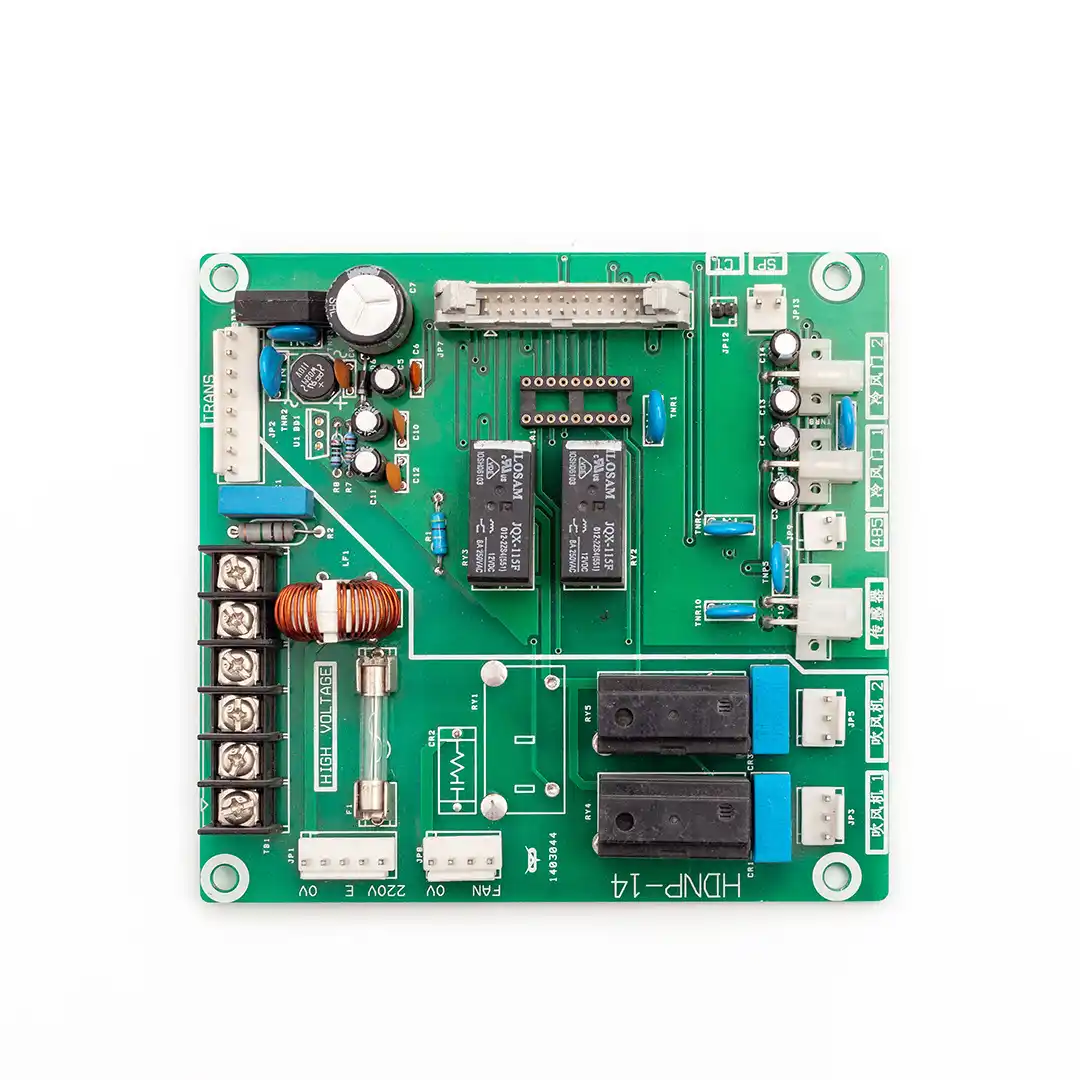
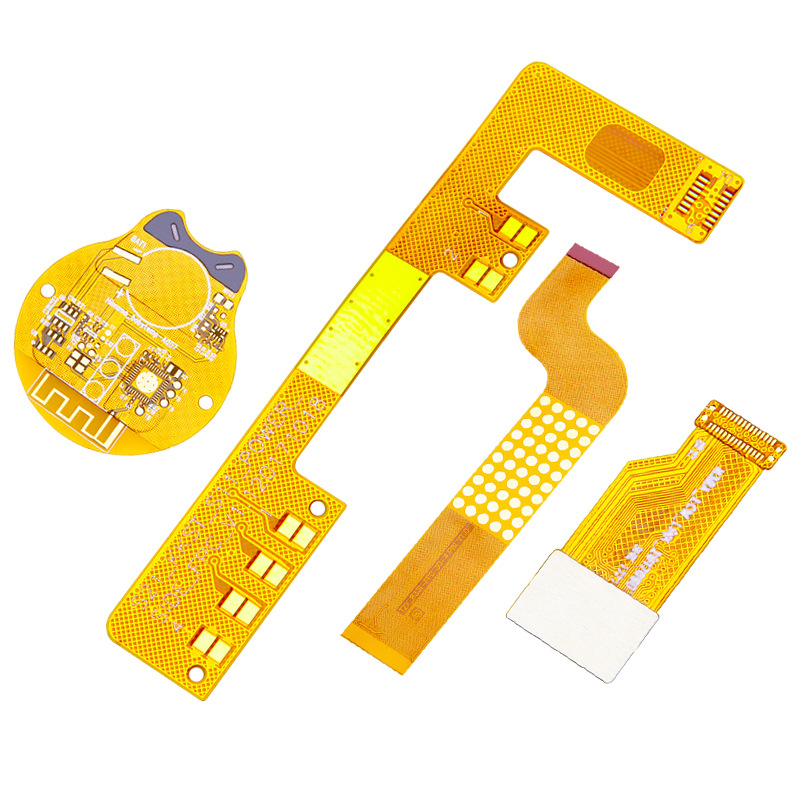
Overcoming Tropical Coastal Challenges: Human-Machine Interfaces in the Eastern Caribbean
Deploying electronic user interfaces in Antigua and Barbuda presents unique environmental stressors unlike continental operating conditions. Surrounded by the Atlantic Ocean and the Caribbean Sea, the twin-island nation experiences constant relative humidity averaging 75% to 88%, continuous high-saline coastal atmospheric loading, high ambient solar UV radiation, and intense tropical storm fronts. Conventional commercial-grade membrane keypads constructed with standard PET and low-grade conductive silver inks inevitably suffer premature failure due to silver electromigration, adhesive delamination, and graphic overlay embrittlement.
To ensure prolonged operational integrity across yacht harbors, resort automation nodes, and desalination facilities, Shenzhen VUKO Electronics implements stringent architectural defenses specifically designed for tropical maritime and coastal environments:
1. Anti-Silver Migration Barrier
Moisture combined with ionic salt particles triggers silver dendrite growth between tightly spaced conductive traces. We engineer our keyboards with wider track spacing (≥0.5mm), apply dielectric encapsulation overpasses, or utilize pure etched copper Flexible Printed Circuits (FPC) with ENIG gold plating to eliminate migration risks permanently.
2. Marine-Grade Adhesive Formulations
High ambient heat combined with coastal humidity causes standard pressure-sensitive adhesives to soften, creep, or wick moisture. VUKO specifies genuine 3M™ 300LSE and 200MP acrylic adhesive stacks, providing unmatched shear strength on low-surface-energy plastics, anodized aluminum, and powder-coated enclosures.
3. Sub-Surface UV-Resistant Inks
Ultraviolet index levels in Antigua routinely exceed 11+. To prevent solar discoloration, fading, and micro-cracking of the graphic overlay, we utilize premium Autotex XE polyester films coupled with UV-cured sub-surface screen printing that guarantees long-term tactile flex and optical clarity.
Antigua and Barbuda Industry Application Scenarios
Explore how our custom membrane keyboards, silicone switch panels, and PCBA solutions empower critical sectors across the islands.
Yachting & Marine Navigational Cockpits
With English Harbour and Falmouth Harbour serving as the premier mega-yacht hubs of the Caribbean, marine electronics demand complete resistance to direct sea spray, wash-downs, and diesel fuel vapours. Our IP67/IP68 tactile membrane switches serve in helm console panels, anchor windlass controls, bilge pump automation, and depth sounder displays, featuring tactile metal domes that provide reliable positive feedback even when operated by crew wearing wet rigging gloves.
Luxury Resort & Eco-Hotel Automation
Antigua’s hospitality sector—including world-renowned properties from Dickenson Bay to Half Moon Bay—relies on elegant, tamper-resistant access keypads, intelligent bedside guestroom master consoles, and pool/spa mechanical automation. We manufacture ultra-slim capacitive touch panels and graphic overlays featuring antimicrobial coatings, custom brand typography, and quiet acoustic actuation that seamlessly blend luxury interior design with rugged environmental tolerance.
Solar PV Microgrids & Island Utilities
As Antigua and Barbuda expands clean energy initiatives, solar inverter plants, commercial lithium-iron-phosphate (LiFePO4) storage hubs, and seawater reverse osmosis (SWRO) desalination facilities require robust operator interface consoles. Our membrane panels and custom PCBAs feature wide operating temperature ratings (-30°C to +85°C), chemical-resistant venting membranes to prevent internal condensation pressure build-up, and high electromagnetic shielding (EMI/ESD protection).
Comparative Engineering Guide: Marine & Island Applications
A rigorous engineering benchmark helping procurement engineers select the optimal material stack for high-salinity and tropical UV environments.
| Subsystem Component | Standard Commercial Grade | VUKO Marine/Tropicalized Specification | Performance in Antigua Environment |
|---|---|---|---|
| Graphic Overlay Film | Standard Gloss Polycarbonate (PC) | Autotex XE UV-Stabilized Textured PET | Immune to Solar Yellowing & Micro-Fissures |
| Conductive Trace Circuit | Standard Screen-Printed Silver Paste | Enclosed Silver Dielectric or Etched Copper FPC | Zero Silver Migration in >85% Relative Humidity |
| Perimeter Ingress Protection | Non-sealed or single adhesive layer (IP40) | Continuous Channel Gasket Seal (IP67/NEMA 4X) | Withstands Direct High-Pressure Salt Spray |
| Tactile Dome Material | Mild nickel-plated carbon domes | Stainless Steel (SUS301) Gold-Flash Plated Domes | >1,000,000 Actuations; Corrosion-Proof |
| Substrate Mounting Adhesive | Standard domestic acrylic tape | Genuine 3M™ 468MP or 300LSE High-Shear Adhesive | Resists Coastal Thermal Cycling (22°C to 45°C) |
| Circuit Termination Tail | Unreinforced standard silver flexible tail | Polyimide (PI) Reinforced Tail with ENIG Contacts | Oxidation-Proof Insertion into Host Motherboards |
Emerging Technological Trends in Antigua & Barbuda
Key growth trajectories influencing embedded hardware procurement and human-machine interface design in the Eastern Caribbean basin.
1. Rapid Modernization of Maritime Telemetry & Charging
With yacht regattas, international sailing weeks, and marinas expanding shore-power electrification, there is an accelerating demand for smart charging station HMIs, automated pedestal billing interfaces, and vessel-to-dock communications. Equipment deployed at the water’s edge requires fully sealed, scratch-proof membrane switch panels that withstand constant sea wash, diesel exhaust residues, and direct tropical sunshine.
2. Decentralized Renewable Microgrids & Water Desalination
The transition toward localized solar PV generation, micro-hydro, and modern reverse-osmosis desalination complexes in both Antigua and Barbuda requires high-uptime embedded controls. Engineers are transitioning away from bulky mechanical push-buttons that corrode and bind with salt crystals to low-profile, smooth-surface membrane keypads that can be easily sanitized and rinsed down without risk of electrical shorts.
3. Smart Port Infrastructure & Logistics Modernization
With major capital upgrades at St. John's Deep Water Harbour and V.C. Bird International Airport, automated logistics, cargo crane cabins, refrigerated container monitoring units, and biometric security gateways require reliable human-machine controllers. These installations require integrated PCBAs, back-lit tactile switches, and high-contrast night-vision overlays capable of uninterrupted duty cycles.
Why International Buyers Trust Shenzhen VUKO Electronics
Combining world-class manufacturing infrastructure in Shenzhen with end-to-end turnkey engineering support for overseas project teams.
14+ Years Alibaba-Verified Supplier
Onsite audited manufacturing facilities in Shenzhen, offering audited production processes, Alibaba Trade Assurance order protection, and established global shipping logistics directly into Antigua and Barbuda.
Comprehensive One-Stop Ecosystem
Eliminate multiple supplier conflicts. From custom bare PCB fabrication (FR4, High-TG, Aluminum MCPCB) to turnkey PCBA assembly, BOM sourcing, flexible circuits (FPC), and finished membrane switch panels all produced under one quality regime.
24-Hour DFM & Engineering Review
Our senior hardware engineering team reviews your Gerber files, BOM component availability, key layout, and environmental requirements within 24 hours, highlighting impedance, clearance, and thermal issues before fabrication.
Low MOQ & Agile Prototyping
We welcome prototype and small-batch pilot runs starting from just 5 pieces. Refine your membrane switch tactile feel, backlighting uniformity, and mechanical integration before committing to high-volume production tooling.
Certified Quality Assurance
ISO9001 certified manufacturing, UL 94V-0 flame retardancy compliance on laminates, lead-free RoHS and REACH certified materials. Each membrane switch undergoes 100% electrical continuity, resistance, and dome tactile force inspection.
Seamless Caribbean Logistics
Export-grade vacuum packing and moisture-barrier electrostatic bagging. Experienced in courier dispatch via DHL, FedEx, and air freight consolidation to V.C. Bird International Airport (ANU) with verified commercial invoices and HS documentation.
Frequently Asked Questions for Buyers in Antigua & Barbuda
Essential guidance on lead times, engineering file preparation, customs clearance, and marine specifications.
How do you ensure membrane switch keypads survive high salinity and humidity in Antigua?
What engineering design files are required to obtain a firm quotation and DFM feedback?
What are your minimum order quantities (MOQ) and sample prototyping lead times?
How are shipments managed and delivered to Antigua and Barbuda?
Can VUKO reverse-engineer or clone obsolete membrane keypads for legacy marine or resort equipment?
What payment terms and transaction security mechanisms are available?
Start Your Custom Membrane Switch or PCBA Project Today
Consult directly with our Shenzhen engineering specialists. Submit your vector artwork, Gerber archives, or BOM for a comprehensive DFM manufacturability evaluation and rapid quotation within 24 hours.
Send an Inquiry