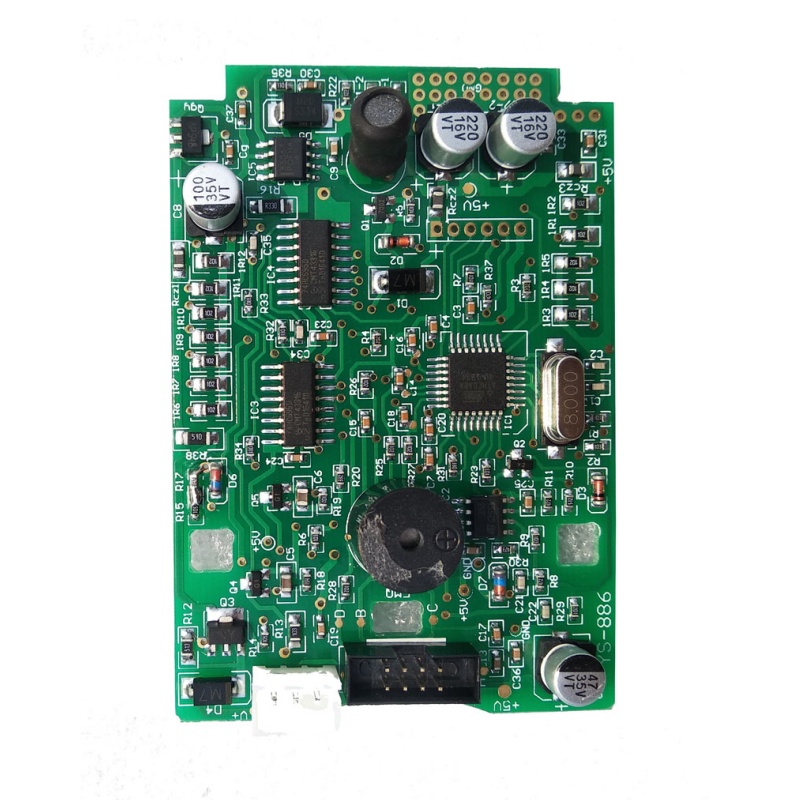
Featured Component Solutions
Engineered Hardware for High-Humidity & Marine Operations
Direct from our Shenzhen manufacturing center: high-reliability interfaces, sensor sub-assemblies, and active electronic modules optimized for deployment across Betio and the South Tarawa economic zone.
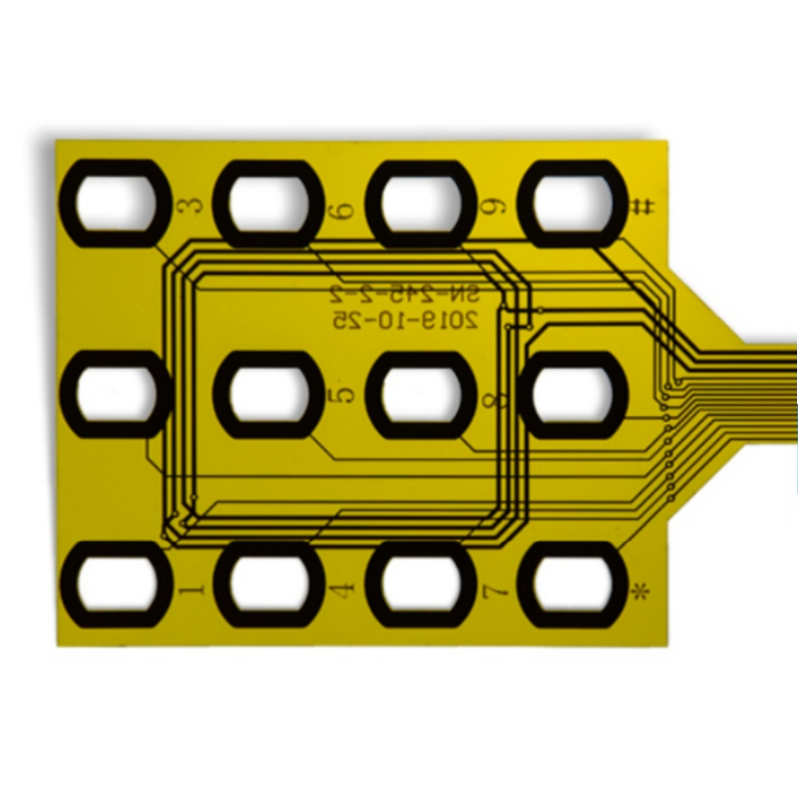
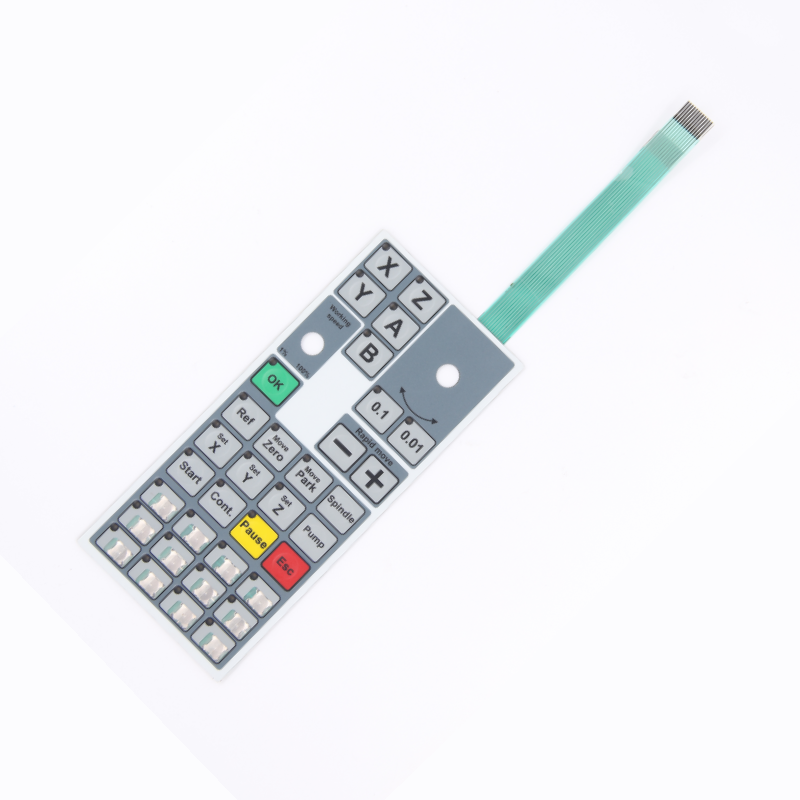
Industrial Analysis
Engineering Human-Machine Interfaces for Betio's Atoll Geography
A technical assessment of material choices, environmental challenges, and supply chain logistics for equipment deployed on South Tarawa.
Betio, serving as the commercial and port epicentre of the Republic of Kiribati, presents one of the most uniquely demanding operating environments on Earth for electrical and mechanical control systems. Surrounded by the open Pacific Ocean, industrial hardware, fisheries infrastructure, water desalination equipment, and local telecommunications infrastructure are subjected continuously to an atmosphere saturated with airborne sodium chloride (marine salt spray), ambient relative humidity routinely exceeding 85%, and elevated ultraviolet radiation indices. Conventional mechanical keyboards, open pushbuttons, and unsealed elastomer keypads inevitably succumb to contact oxidization, internal corrosion, and structural delamination within months of deployment.
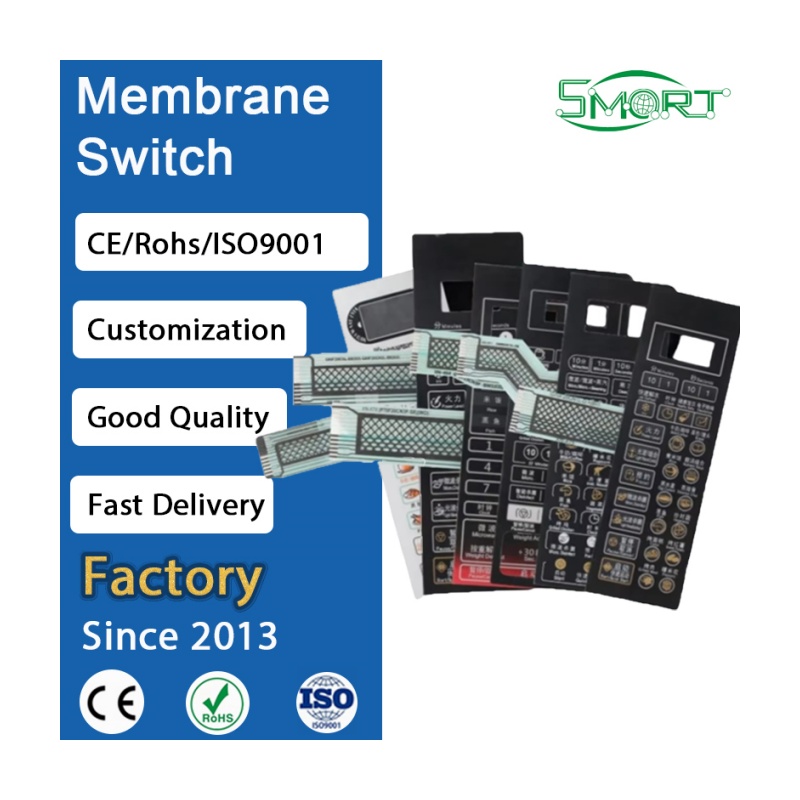
In response to these specific atoll vulnerabilities, modern electronic product designers and procurement directors serving Betio have shifted towards sealed, low-profile membrane switches and hybrid capacitive interfaces. Unlike legacy electro-mechanical switch assemblies that require continuous mechanical apertures through the enclosure wall, a properly engineered membrane keypad establishes a monolithic, hermetically sealed barrier. By combining specialized biaxially oriented polyethylene terephthalate (PET) substrate layers, sealed perimeter adhesive rings (utilizing high-grade acrylic adhesives like 3M 467MP/468MP), and anti-corrosive silver carbon circuit printings, these interfaces resist both fluid ingress and accelerated electrochemical migration.
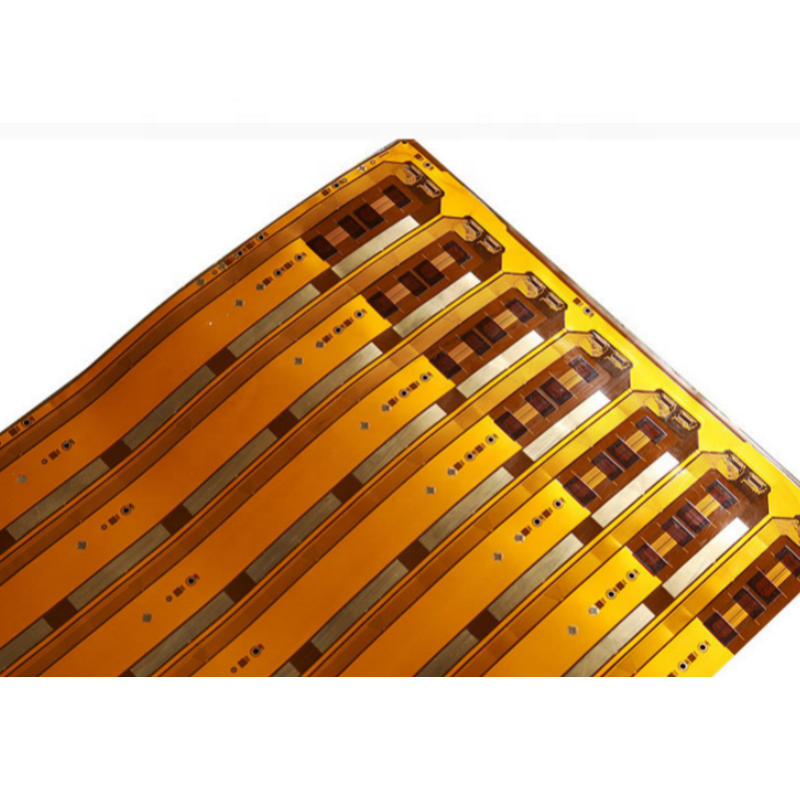
The manufacturing ecosystem requires meticulous adherence to Design for Manufacturing (DFM) rules. In particular, silver ink traces printed directly onto flexible polyester substrates are inherently susceptible to silver migration (dendritic short-circuiting) when exposed to moisture condensation and direct electrical bias. Top-tier international manufacturers circumvent this failure mechanism either by applying complete carbon-paste dielectric overcoats or by migrating mission-critical projects to flexible printed circuits (FPCs) with rolled annealed copper coated in immersion gold (ENIG). For project managers in Betio managing ports, municipal power distribution, or marine processing, specifying these precise technical parameters is vital to guaranteeing multi-year operational uptime.
| Specification Parameter | Standard Commercial Grade | Maritime Industrial Grade (Betio Standard) | Extended Life Harsh-Environment |
|---|---|---|---|
| Base Overlay Material | Standard Polycarbonate (PC) | Autotex / Autoflex Textured PET | UV-Resistant Hardcoated Polyester |
| Ingress Protection (IP) | IP40 – IP54 | IP65 – IP67 (Continuous Perimeter Seal) | IP68 Hermetic Gasket Bonded |
| Circuit Substrate | Silver Ink on PET Film | Silver Ink + Carbon Dielectric Protective Mask | Polyimide (PI) Flex PCB with ENIG Finish |
| Actuation Lifespan | 500,000 Cycles | 1,000,000 Cycles (Stainless Steel Dome) | 5,000,000+ Cycles (Capacitive Sensing) |
| Salt Spray Resistance | ASTM B117 < 24 Hours | ASTM B117 96+ Hours Compliant | ASTM B117 240+ Hours Marine Grade |
| Operating Temperature | -10°C to +55°C | -20°C to +70°C | -40°C to +85°C Industrial Wide-Temp |
Market Directory
Top 10 Membrane Keypad Manufacturers & Suppliers Serving Betio
Vetted global fabricators capable of meeting the logistical, technical, and environmental requirements of the South Pacific region.
#1 Full-Stack OEM
Verified Manufacturer
Shenzhen VUKO Electronics Co., Ltd.
Headquartered in the global electronics center of Shenzhen, VUKO provides a unified end-to-end manufacturing footprint. Specializing in integrated solutions, VUKO engineers custom membrane switches, rigid-flex PCBs, metal-dome arrays, and full turnkey SMT assemblies under a single roof. Their fast-turn prototypes start from an accessible 5-piece MOQ, accompanied by comprehensive 24-hour DFM engineering reviews.
#2 Global Tier
Aerospace / Medical
Nelson-Miller Inc.
A long-standing global player formed from the merger of Nelson Nameplate and Miller Dial, Nelson-Miller manufactures high-reliability membrane keypads, capacitive switches, and rugged graphic overlays for severe outdoor environments. Their systems are widely deployed in aerospace navigation and marine diagnostic hardware requiring extended UV resistance.
#3 Custom HMI
Industrial Precision
Epec Engineered Technologies
Epec specializes in build-to-print custom electronic assemblies with a specific emphasis on harsh-duty human-machine interfaces. Providing complete environmental gasketing, embedded LED backlighting, and copper-flex circuit backplanes, their manufacturing models cater effectively to remote infrastructure programs requiring long MTBF intervals.
#4 Specialized Tech
Medical / Maritime
GGI Solutions
Renowned for printed electronics and advanced interface modules, GGI designs specialty tactile keypads with integrated electromagnetic interference (EMI) shielding. Their systems are suitable for commercial vessel retrofits calling into Betio Harbor that require high resistance to electrical noise and salt water mist.
#5 Precision Interface
Industrial Automation
Dyna-Graphics Corporation
Specializing in custom membrane keypads, rubber keypad assemblies, and touchscreen panels, Dyna-Graphics offers proprietary sealing configurations that protect tactile switches from wash-downs, chemical cleanings, and high ambient moisture exposure characteristic of South Pacific fish processing facilities.
#6 Sensor Integration
High Volume OEM
Xymox Technologies, Inc.
Xymox is recognized for mass-scale manufacturing of conductive printed electronics and high-durability polyester membrane circuits. Their screen-printing capabilities deliver precise trace impedance and robust carbon switch contacts suitable for integration into regional solar charge controllers and telecommunications enclosures.
#7 Graphic Overlays
Chemical Resistant
Lustre-Cal Corporation
Offering specialized expertise in industrial overlays and rugged membrane keypads, Lustre-Cal focuses on sub-surface digital and screen printing onto polycarbonate and polyester films. This guarantees that operational legends and key labels will not scratch off or degrade under heavy ultraviolet sunlight exposure in the central Pacific.
#8 Medical / Marine
Custom Design
Pannam Imaging
A division of Conductive Technologies, Pannam designs custom membrane switches, rubber keypads, and integrated display windows. Their engineering protocols include extensive life-cycle cycle testing and environmental chamber exposure testing to validate performance under severe humidity swings.
#9 Printed Electronics
Flexible Sensors
Butler Technologies, Inc.
Butler Technologies brings extensive engineering insight to wearable sensors, flexible heating elements, and user interfaces. Their membrane keypads feature precise embossing profiles (rim and pillow embosses) providing unmistakable tactile feedback to technicians wearing protective work gloves.
#10 Advanced HMI
European Standards
Quad Industries
Operating out of Europe with global shipping reach, Quad Industries leads in capacitive touch control assemblies, membrane switches, and printed electronic surfaces. Their hybrid integration pairs smart display logic directly behind sealed graphic skins to maximize interface density in constrained consoles.
Market Trends
Emerging HMI and Control Hardware Trends in Betio
How technological modernization, renewable power, and climate-resilience requirements are shaping electronics procurement across Tarawa Atoll.
Off-Grid Solar Integration
With South Tarawa actively expanding decentralized solar-plus-storage mini-grids, inverter manufacturers require dust-tight, UV-stable keypad interfaces capable of remaining exposed to ambient tropical sunlight for decades without yellowing or cracking.
Fisheries & Cold-Chain Telemetry
Tuna fishing fleets and cold-storage processing terminals operating out of Betio Port are modernizing legacy electromechanical relays with digital membrane panels integrated with BLE / satellite IoT tracking motherboards.
Desalination Automation
Freshwater management is existential on atolls. Reverse-osmosis desalination units require IP66/IP67 membrane controls resistant to caustic mineral scaling, chlorine exposure, and direct salt water splashing during maintenance operations.
Integrated Modular Sourcing
Due to isolated air-freight and ocean shipping legs to Bonriki International Airport and Betio Port, procurement teams are abandoning fragmented vendor chains in favor of single-source turnkey partners supplying keypads, PCBs, and passive BOM assemblies simultaneously.
Field Engineering
Localized Application Scenarios in Betio and Kiribati
Examining field-proven implementations where sealed membrane panels and specialized PCBAs maintain uptime.
Betio Port Crane & Winch Pendants
Stevedoring operations at the Betio commercial container wharf subject handheld crane controllers to frequent rain squalls and sea-spray. Custom tactile membrane keypads integrated over rigid aluminum backplates provide operators with crisp tactile feedback through wet gloves while sealing internal electronics to an IP67 rating.
Atoll Solar-Powered Water Pumping
Decentralized groundwater monitoring and pumping stations across Tarawa utilize microcontroller boards connected to membrane touchpads. These panels feature integrated transparent LCD cutouts and LED indicators, allowing local technicians to adjust flow rates and verify salinity readings without opening sealed NEMA enclosures.
Fisheries Refrigeration Control Panels
Refrigerated commercial container storage facilities in Betio run continuously under high condensing humidity. Replacing traditional rocker switches with sealed poly-dome membrane matrices prevents salt crystallization around switch contacts, eliminating intermittent open-circuit faults.
Factory Direct Capabilities
Why Engineers Choose Shenzhen VUKO Electronics
Complete turnkey hardware manufacturing from the center of the world's electronics supply chain.
One-Stop Manufacturing
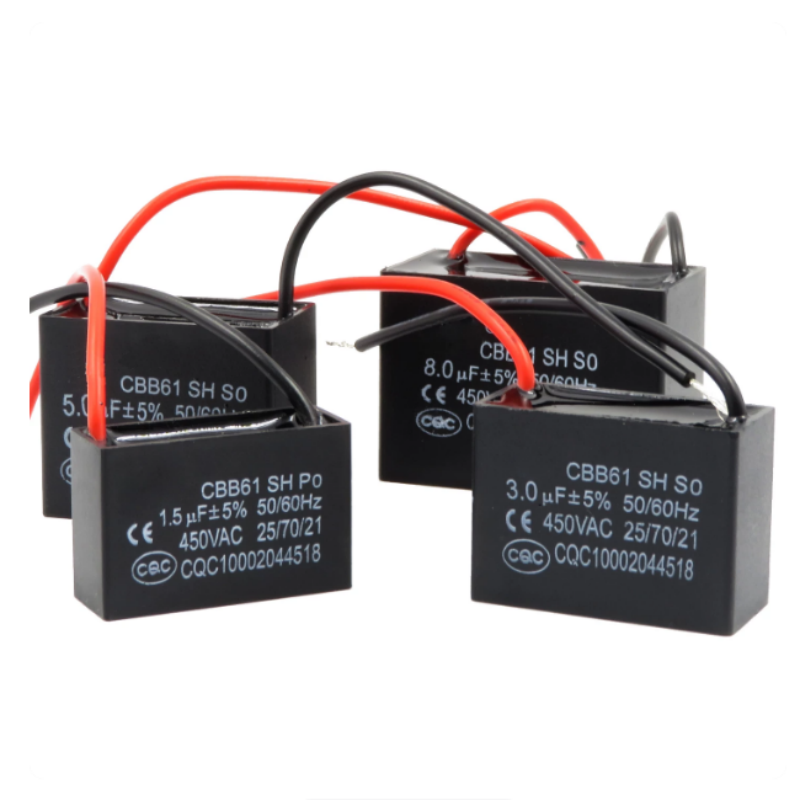
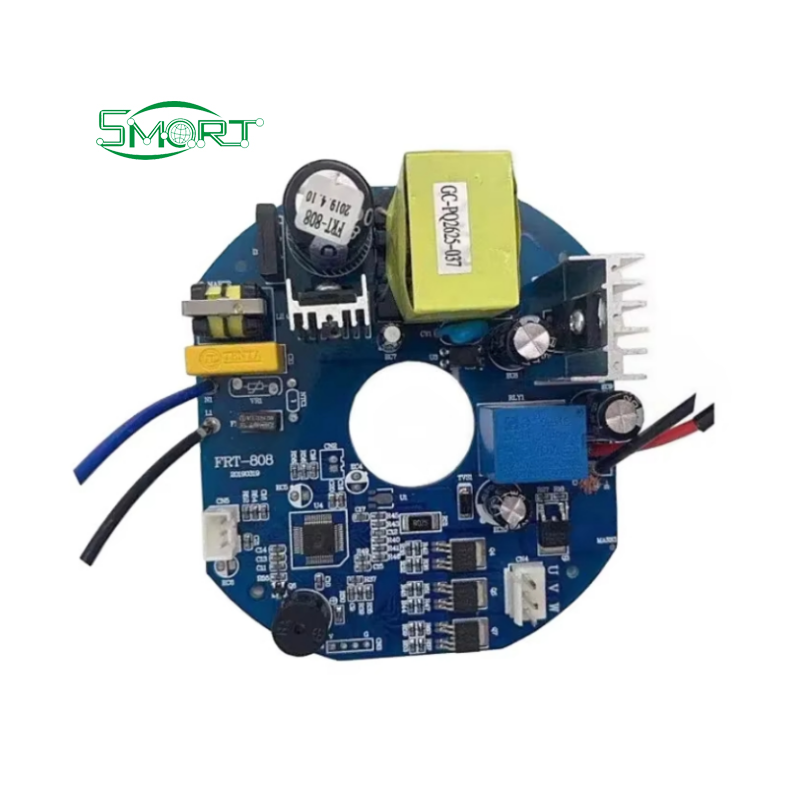
Eliminate multi-vendor friction. We fabricate bare PCBs (FR-4, High-TG, Aluminum Core, Flexible FPC), procure complete active BOMs, assemble via automated SMT/DIP lines, and produce custom membrane switches under a single management team.
Rigorous Inspection & QC
Every board and membrane tail is subjected to full flying-probe or fixture electrical testing (E-test), automated optical inspection (AOI), and actuation force validation. We supply RoHS compliant and UL 94V-0 certified flame retardant materials.
Fast DFM & Low 5-Piece MOQ
Our experienced engineering team evaluates your Gerber files, BOM lists, and graphic panel artwork within 24 hours. We identify trace spacing risks, thermal relief issues, and component lead-time bottlenecks before initiating production.
Export & Freight Reliability
Backed by over 14 years of international export experience on Alibaba.com and Trade Assurance payment protection, we coordinate direct courier (DHL, FedEx, UPS) and consolidated freight shipments directly to Kiribati ports without administrative delay.
Procurement Guide
Frequently Asked Questions for Betio Procurement Managers
Essential answers regarding design requirements, freight logistics, environmental protection, and custom orders.
How can membrane switches be protected against Betio's extreme salt spray and humidity?
To resist accelerated maritime corrosion, we recommend specifying: (1) An IP67 perimeter adhesive gasket using 3M 467MP/468MP acrylic adhesive; (2) UV-resistant Autotex textured polyester (PET) overlays rather than standard polycarbonate (PC); (3) Carbon-paste overcoats on all printed silver conductors or transitioning to an ENIG-plated Polyimide Flexible Printed Circuit (FPC) tail to eliminate silver migration risks entirely.
What engineering files are required to obtain a fast quotation and DFM review?
For custom membrane switches, provide your vector artwork (AI, CDR, or DXF/DWG) detailing dimensions, colors (Pantone/RAL codes), key embossing profiles, window positions, and tail pinouts. For full turnkey PCB/PCBA builds, submit your Gerber files (RS-274X format), NC drill files, centroid pick-and-place files, and a comprehensive BOM with exact manufacturer part numbers.
What is the minimum order quantity (MOQ) for prototypes shipping to Kiribati?
Our standard prototyping threshold starts from just 5 pieces for custom bare PCBs, turnkey PCBA assemblies, and custom membrane switch panels. This allows regional engineering teams and local system operators in Betio to conduct full field-testing and fit checks prior to committing capital to mass production runs.
How are electronics packaged to survive transit across the tropical Pacific?
All finished assemblies undergo vacuum sealing in anti-static ESD shielding bags with integrated desiccant packs and humidity indicator cards. Outer shipping cartons are heavy-duty, double-walled corrugated fiberboard, internally lined with shock-absorbent custom foam padding to prevent puncture and moisture ingress throughout multi-leg transit.
Can you clone or reverse-engineer legacy control panels from aging vessel or plant equipment?
Yes. If original Gerber files or schematics are missing due to the age of installed marine or port machinery, our reverse engineering division can extract circuit schematics, trace routing, and artwork directly from a physical sample or high-resolution scanning, re-generating modern digital manufacturing files for production.
What logistics methods are available for delivering shipments into South Tarawa?
For urgent prototype batches and repair kits, express air courier (DHL, FedEx, UPS) routes via regional Pacific transport hubs directly into Bonriki International Airport (TRW). For larger commercial production quantities, consolidated ocean freight can be routed to the Port of Betio with full customs documentation, commercial invoices, and packing manifests supplied.
Start Your Production Run
Ready to Build Rugged, Industrial-Grade Hardware for Betio?
Send us your design parameters, CAD drawings, or BOM list today. Our Shenzhen engineering hub will deliver a thorough Design for Manufacturing (DFM) assessment and transparent factory quotation within 24 hours.