Architectural & Marine
Precision-engineered components, integrated sub-assemblies, and specialized PCBA modules qualified for severe environmental operating parameters across New Zealand.
Bridging global manufacturing efficiency with the hyper-demanding engineering specifications of Christchurch's premier tech clusters.
Across Canterbury plains, SMD assemblies drive autonomous telemetry units, dairy yield analyzers, and multi-spectral soil probes. These boards undergo thermal shock cycling and polyurethane conformal coating to survive cyclic humidity, sub-zero winters, and agricultural chemical runoff without trace corrosion or dielectric breakdown.
Centering around Christchurch's dedicated aerospace precinct, engineering requirements insist on outgassing-compliant substrates, ENIG/ENEPIG surface finishes, and zero-voiding under BGA components via 3D Automated X-ray Inspection (AXI) to guarantee mission-critical performance at sub-orbital altitudes.
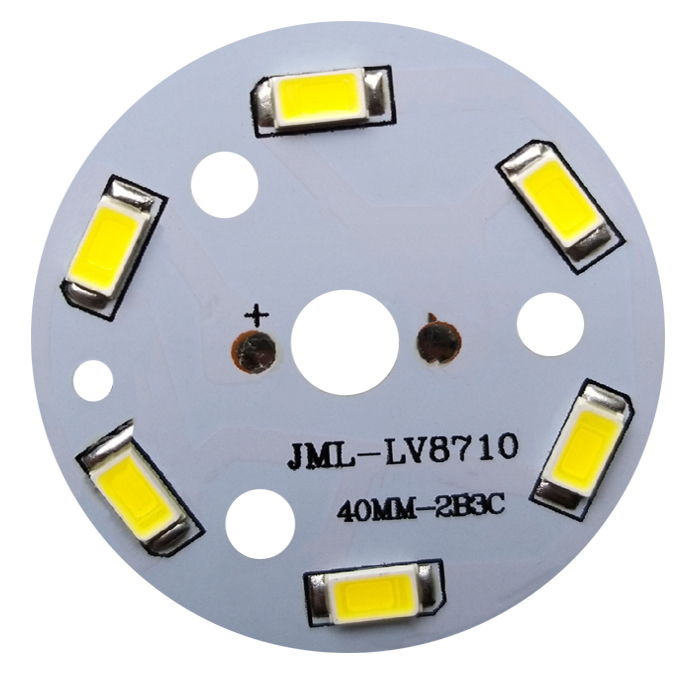
Christchurch boasts a legacy of heavy industrial power electronics. Our heavy-copper (2oz to 6oz) multi-layer fabrications and metal-core aluminum boards dissipate immense thermal loads generated by commercial induction heating, micro-hydro generators, and heavy-equipment motor drives.
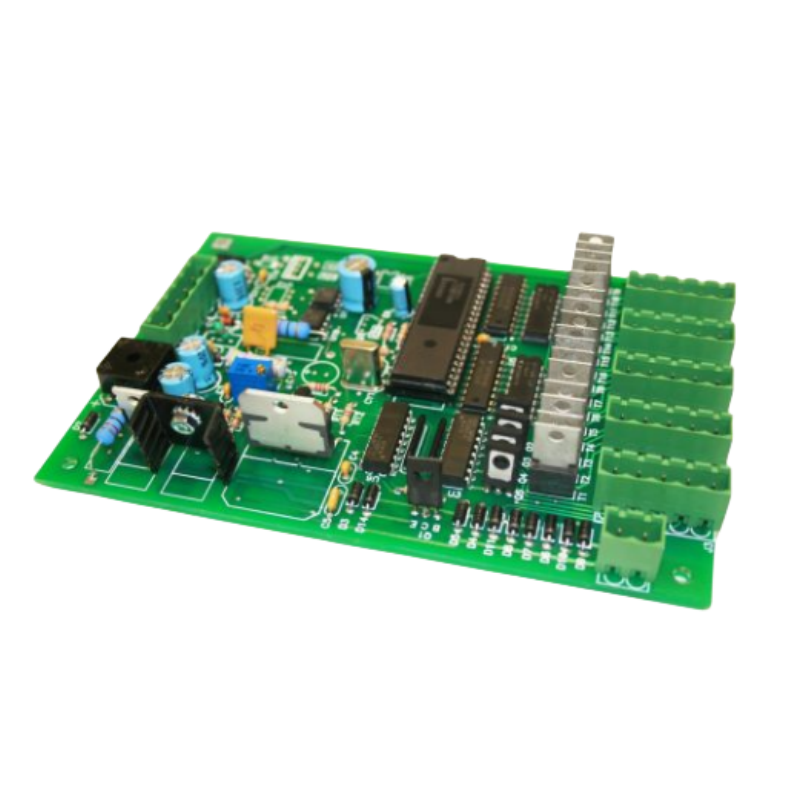
Hardware manufacturers across Hornby, Burnside, and Middleton face significant local capacity constraints for mid-to-high volume surface-mount production. Our Shenzhen production infrastructure provides Christchurch hardware developers with full access to high-speed modular pick-and-place lines capable of mounting complex multi-die chips, fine-pitch BGAs (0.35mm pitch), CSPs, and micro-footprint 01005 passives.
By combining high-TG FR-4 rigid laminates with multi-layer polyimide flexible tails (FPC), local engineers eliminate space-consuming wire harness modules and board-to-board connectors. This architecture improves resistance to the constant vibrations common in mobile agricultural machinery and maritime navigation platforms.
Inquire Now
How cutting-edge surface-mount design rules are shifting across New Zealand's South Island engineering community.
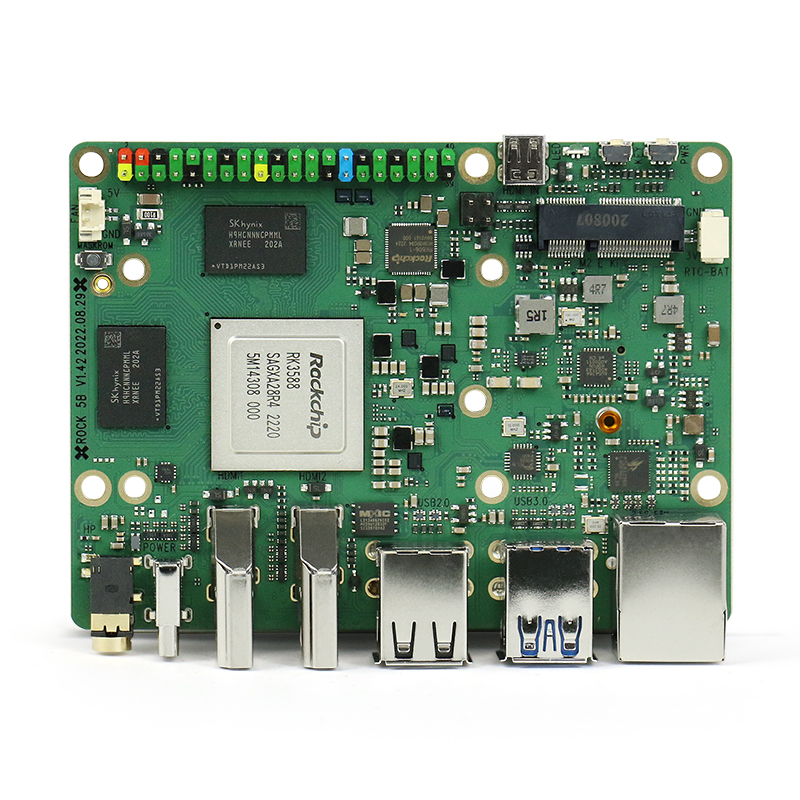
The proliferation of Edge AI hardware, such as the RK3588 octa-core ecosystem, necessitates Any-Layer HDI PCB stack-ups with micro-via laser drilling (down to 0.075mm). Christchurch designers are rapidly phasing out traditional through-hole vias on complex processors to manage signal integrity, reduce EMI emissions, and shorten high-frequency trace lengths.
Geographic isolation means South Island manufacturers cannot afford unforeseen end-of-life (EOL) announcements or prolonged silicon lead-times. Forward-looking procurement models emphasize complete BOM scrubbing during the initial DFM check, pre-identifying drop-in pin-compatible alternate active ICs and passive component packages.
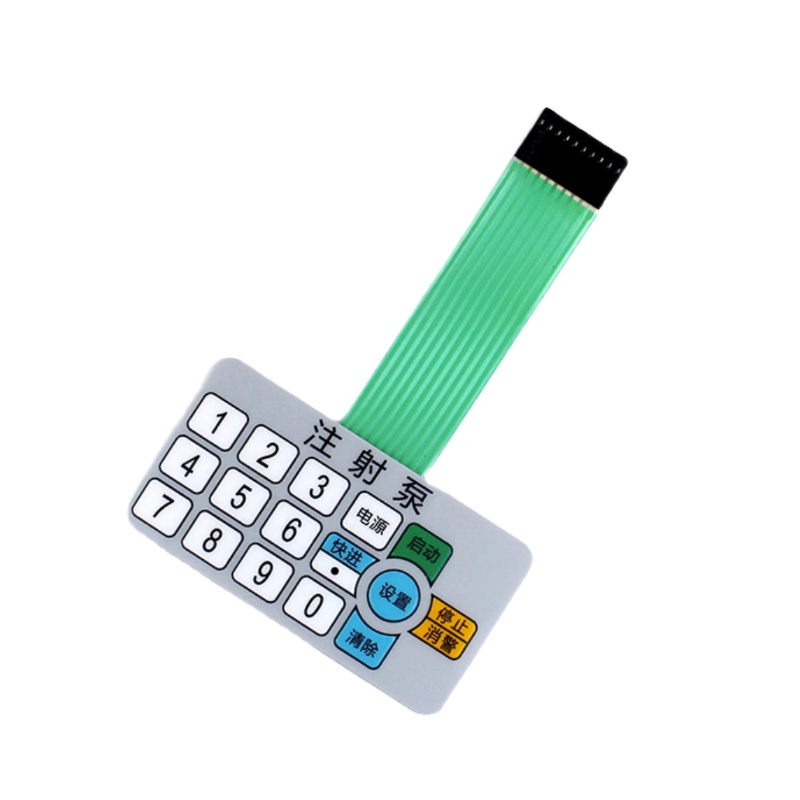
Christchurch-designed field monitors and food processing systems demand cleanability and weather endurance. The market has moved decisively toward IP65/IP67 rated front panels that merge waterproof tactile membrane switches, graphic backdrops, status micro-LEDs, and EMI shielding into unified plug-and-play surface assemblies.
Clear comparison parameters to guide component buyers, production managers, and hardware architects in making defensible supplier selections.
| Evaluation Parameter | Domestic NZ Small-Batch Assembly | Standard Generic Exporters | Shenzhen VUKO Electronics Turnkey |
|---|---|---|---|
| Prototyping MOQ | Low (1–5 boards), but high unit setup cost | Strict minimums (500–1000 pcs) | Flexible prototype from 5 pcs to mass volume |
| Component Sourcing Scope | Customer consigned or local distributors | Limited domestic China market access | Complete Turnkey: Tier-1 franchised + Huaqiangbei hub |
| DFM & Engineering Review | High skill, but manual & time-intensive | Automated check only, missing BOM obsolescence | Dedicated engineer review <24h (BOM, layout, impedance) |
| Specialized Substrates | Limited internal fabrication (often outsourced) | Standard FR4 focus; rigid-flex delayed | FR4, Aluminum MCPCB, Rigid-Flex, Polyimide FPC, Rogers |
| Inspection & Quality Rigor | Visual & bench test; optional X-ray | Basic flying probe, variable AOI thresholds | 100% AOI, E-Test, SPI, 3D X-Ray for BGA, functional jigs |
| Transit to Christchurch (CHC) | Local road/courier (1–2 days) | Postal air packet (10–20 days) | Express DHL/FedEx (3–5 working days to CHC airport) |
Combining world-class manufacturing scale with bespoke customer support and comprehensive process transparency.
Before copper is exposed or stencils laser-cut, our engineering team thoroughly reviews your Gerber RS-274X, drill patterns, centroid coordinates, and Bill of Materials. We identify copper balance anomalies, thermal relief deficiencies, and footprint land pad discrepancies, eliminating expensive assembly faults before line setup.
Located in Shenzhen—the central node of global electronics manufacturing—we rapidly secure authentic silicon, passive networks, and mechanical hardware. We maintain rigorous incoming material screening, anti-counterfeit microscopic verification, and moisture-barrier handling (MSL 3/4/5) to ensure factory-fresh solderability.
Every multilayer rigid and flexible board passes through precision CNC mechanical or UV laser drilling, electroless panel plating, inner-layer AOI, automated soldermask lamination, and ENIG/HASL chemical baths. Continuous micro-sectioning and thermal stress testing guarantee via reliability and inter-layer adhesion.
Direct technical answers addressing international customs, compliance certifications, shipping timelines, and payment protections.
Eliminate component sourcing bottlenecks, reduce layout iterations, and secure predictable volume pricing. Connect directly with our Shenzhen engineering hub for technical DFM verification and project quotation within 24 hours.