Featured Industrial Switches & Integrated Electronics
Precision-fabricated interface assemblies, motor drivers, passive modules, and flexible interconnects verified for harsh environmental compliance, thermal stability, and prolonged mechanical longevity.
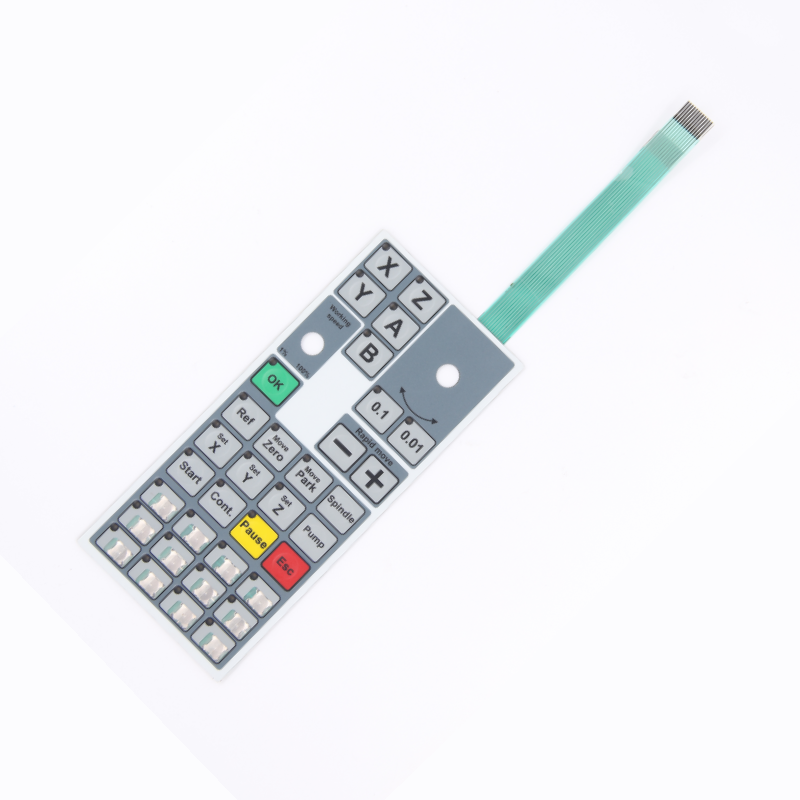
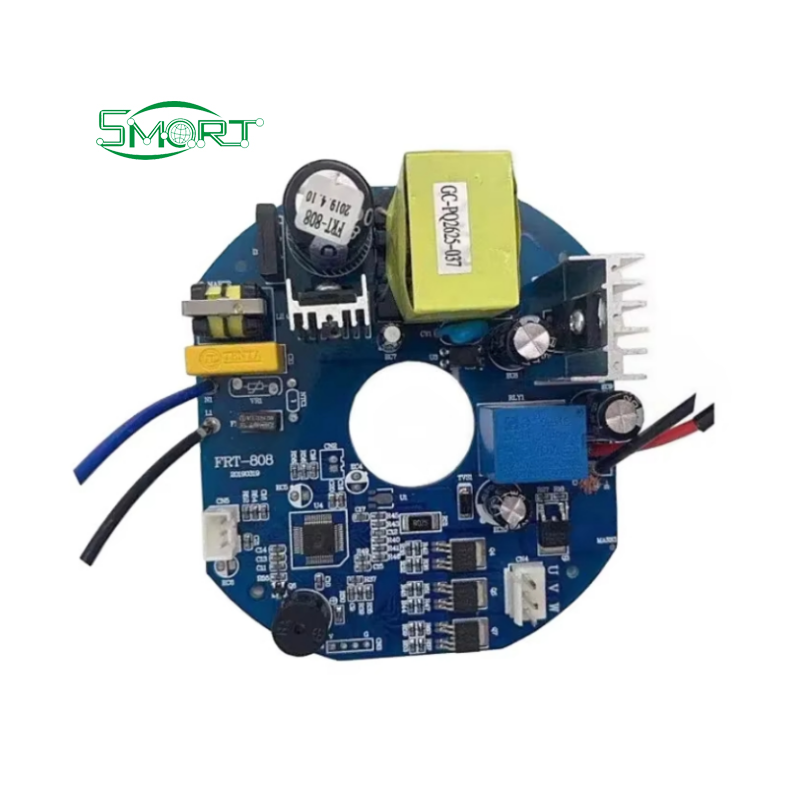
Engineering Architecture & Layer Stratification of Industrial Membrane Switches
In modern mission-critical applications—ranging from medical ventilation systems and automated PLC control cabinets to aerospace ground stations and high-vibration off-highway vehicles—the Human-Machine Interface (HMI) serves as the primary gateway for operational continuity. An industrial-grade membrane switch is far more than a decorative graphic overlay positioned above basic momentary contacts; it is a meticulously engineered, multi-strata optoelectronic micro-assembly designed to withstand millions of continuous actuations while completely hermetic against chemical ingress, electrostatic surges, and drastic thermal expansion differentials.
At Shenzhen VUKO Electronics Co., Ltd., our manufacturing methodology enforces strict adherence to physical layer optimization. A typical heavy-duty industrial switch comprises between five and nine laminated tiers, each performing an indispensable mechanical or electrical function:
Primary Multi-Tier Stack Architecture: Graphic Overlay (Autotype Autoflex EB/EBA or Bayer Makrolon) → Overlay Acrylic Bonding Adhesive (3M 467MP / 468MP) → Tactile Spring Actuator Layer (SUS301 Stainless Steel Snap Domes with Selective Nickel or Gold Plating) → Micro-Punched Dielectric Spacer Cavity → Circuit Substrate (Screen-Printed Micro-Flake Silver Paste with Protective Carbon Crossover or Chemically Etched Polyimide FPC) → Rear High-Cohesion Structural Adhesive (3M 300LSE / VHB Foam for Low Surface Energy Plastics or Powder-Coated Metal Enclosures).
The selection of the graphic overlay film determines the environmental boundary limit of the entire device. Polycarbonate (PC) provides exceptional optical clarity and higher mechanical impact strength at a reduced cost; however, it rapidly degrades under prolonged UV exposure and exhibits vulnerability to petroleum solvents and cyclic flexural fatigue. Consequently, for demanding outdoor and chemical exposure, our engineering standard specifies biaxially oriented polyethylene terephthalate (PET)—such as MacDermid Autotype Autoflex EB. PET provides superior flex-life resilience exceeding 5,000,000 cycles, exceptional resistance to chemical cleaning agents (including IPA, bleach, and ketone derivatives), and superior dimensional stability across extreme temperature ranges from -40°C to +85°C.
Material Science & Structural Engineering Specification Matrix
To assist systems architects and hardware procurement teams in making informed, risk-mitigated technical selections, the following engineering table synthesizes critical parameter comparisons across substrate selections and circuit topologies:
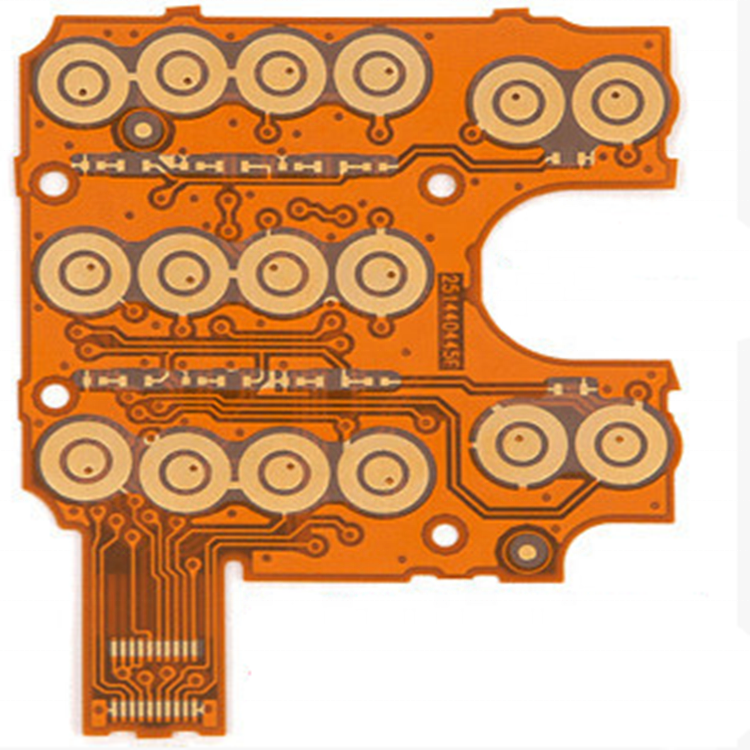
| Engineering Attribute | Standard Silver PET Circuit | Polyimide (FPC) Flex Circuit | FR-4 Rigid PCB Backer Matrix |
|---|---|---|---|
| Conductor Metallurgy | Screen-printed micro-particulate silver flake resin matrix (≤0.05 Ω/sq) | Rolled Annealed (RA) or Electro-Deposited (ED) Copper (0.5 oz - 2 oz) | Standard IPC Class 2/3 Electro-Deposited Copper Clad Laminate |
| Contact Resistance | <100 Ω (dependent on trace length and routing density) | <1.0 Ω (optimal for ultra-low voltage digital logic signals) | <0.1 Ω (ideal for direct power driving and heavy sensor integration) |
| Component Soldering (SMD) | Low-temp conductive silver epoxy bonding (LEDs, resistors) | High-temp lead-free reflow soldering (0201 passives, microcontrollers, QFNs) | Full turnkey SMT / THT automation with automated optical inspection (AOI) |
| Tail Interconnect Pitch | 1.0 mm, 1.27 mm, 2.54 mm pitch with Amphenol / Nicomatic crimp housings | 0.5 mm, 0.8 mm, 1.0 mm ZIF / LIF Zero-Insertion-Force gold fingers | Board-to-board pin headers, terminal blocks, spring terminals |
| Flexural Endurance | Moderate static bend radius (R ≥ 5.0 mm; avoid dynamic hinge flexing) | Exceptional dynamic bend endurance (R ≥ 1.0 mm; >1,000,000 continuous flexes) | Rigid substrate; zero flexural tolerance (structural backing role) |
| Silver Migration Immunity | Requires complete carbon overprint encapsulation and anti-moisture vents | Complete inherent immunity; pure copper traces sealed with polyimide coverlay | Complete inherent immunity; standard LPI solder mask passivation |
Shenzhen VUKO Electronics: Turnkey Manufacturing Advantages & Cleanroom Precision
Operating from Shenzhen's high-tech industrial cluster—the epicenter of global electronics innovation and rapid supply-chain consolidation—Shenzhen VUKO Electronics Co., Ltd. has accumulated over 14 consecutive years of premier export verification on Alibaba.com. We bridge the critical gap between conceptual hardware prototyping and scaled, high-reliability serial fabrication.
Unlike conventional printing workshops that outsource their printed circuit board assembly or rigid-flex manufacturing to downstream contractors, VUKO operates fully unified vertical manufacturing infrastructure under ISO 9001 certified quality oversight. Our state-of-the-art facilities consolidate automated silk-screen printing, precision laser cutting, CNC digital punching, automated tactile metal-dome placement, surface-mount technology (SMT) lines, and Class 10,000 cleanroom environments. This end-to-end integration delivers measurable competitive advantages:
24-Hour DFM Engineering Audits
Every Gerber package, mechanical CAD drawing, and overlay vector file undergoes meticulous Design-for-Manufacturability (DFM) review within 24 hours, mitigating trace spacing errors, venting issues, and impedance mismatch risks before tool fabrication.
Class 10,000 Cleanroom Laminating
Optical window clarity and bubble-free switch action demand an immaculate production environment. All overlay printing, transparent adhesive mounting, and display window laminations occur in climate-regulated Class 10,000 cleanrooms.
Turnkey PCB, PCBA, & FPC Convergence
We solve the multi-vendor challenge. Whether your interface links directly to a BLDC motor control PCBA, requires embedded LED backlighting, or interfaces with specialized heat sinks and sensor modules, we supply everything under one unified purchase order.
Rigorous 100% Quality Screening
Eliminate field failures with 100% automated electrical continuity testing, insulation resistance verification (>100 MΩ at 100V DC), tactile actuation force Profiling (180g to 450g), and automated optical inspection (AOI) for trace fidelity.
Rapid Prototyping from 5 Pieces
Scale without punitive minimum order penalties. We support engineering validation testing (EVT) and design validation testing (DVT) with prototyping volumes starting as low as 5 units before ramping up to multi-thousand-piece monthly runs.
Global Compliance & Traceability
Our raw laminates, conductive adhesives, and curing chemistry comply fully with RoHS and REACH environmental mandates. Flame retardant materials meeting UL 94V-0 criteria ensure unhindered customs clearance across North American and European borders.
Future Industrial Procurement Trends: 2025–2030 Technology Trajectory
The industrial interface landscape is undergoing unprecedented disruption driven by Industrial Internet of Things (IIoT) architectures, ergonomic touch ergonomics, and edge computing requirements. Global procurement directors and lead hardware engineers are moving rapidly beyond traditional electromechanical panels toward intelligent, highly integrated HMI modules. Five dominant technological trajectories define the forthcoming procurement cycle:
1. Transition Toward Capacitive Touch Under Glass / Thick Polycarbonate
While mechanical stainless steel tactile domes remain the gold standard for heavy vibration and tactile feedback when operated with industrial gloves, capacitive touch sensing interfaces printed directly on PET or FPC substrates are capturing extensive market share in medical devices, food processing machinery, and cleanroom hardware. Sealed seamless surfaces eradicate dust cavities and ingress pathways, allowing aggressive chemical washdowns and steam sanitation without compromising system reliability.
2. In-Mold Electronics (IME) and Structural 3D Mechatronics
Traditional flat membrane assemblies mounted via PSA (Pressure Sensitive Adhesive) onto sheet metal housings are being augmented by In-Mold Electronics. IME combines screen-printed functional circuitry and micro-components with 3D thermoforming and plastic injection molding. The outcome is a consolidated, ultra-thin, highly aerodynamic single-piece structural part with embedded capacitive switches, illumination guides, and antenna circuits—reducing mechanical part counts by up to 70% and drastically trimming assembly labor.
3. Optical Waveguide Backlighting & Micro-LED Convergence
Uneven backlight distribution and bulky incandescent bulbs have been entirely replaced by ultra-thin optical light guide films (LGF) and side-firing SMD Micro-LEDs directly mounted on flexible circuits. Modern industrial specifications mandate uniform luminance across complex key arrays, combined with multi-color status annunciation (RGB dead-front icons that remain invisible until activated) to minimize operator cognitive fatigue during high-stress industrial operations.
4. Antimicrobial and Anti-Reflective Nano-Structured Overlays
Post-pandemic healthcare environments and shared food automation kiosks demand surface coatings that continuously neutralize microbiological pathogens without degrading mechanical clarity. Next-generation PET overlay films incorporate covalently bonded silver ions and zinc pyrithione nanoparticles throughout the polymer matrix. Concurrently, advanced anti-glare (AG) and anti-reflective (AR) surface texturing ensure display window readability under direct high-noon solar glare (>10,000 lux outdoor ambient illumination).
5. High-Integrity EMI/RFI Shielding for Variable Frequency Drive Environments
Industrial machinery heavily utilizes Variable Frequency Drives (VFDs), high-voltage brushless DC servo motors, and inductive switching contactors. Unshielded control panels act as unintentional antennas, introducing electrical noise into digital logic buses. Progressive procurement teams now mandate integrated solid aluminum foil or selective screen-printed grid-pattern silver/carbon EMI shielding planes connected directly to system chassis ground, preventing spurious reset commands and erratic capacitive touch events.
Strategic Procurement Guide: Avoiding Catastrophic HMI Deployment Failures
A failed membrane switch in the field often halts million-dollar manufacturing lines or jeopardizes medical treatments. Sourcing managers and component engineers must look beyond the initial quotation price and scrutinize the following high-risk engineering failure modes:
Silver Migration Mitigation: When silver-printed circuits are subjected to continuous DC voltage biases in humid environments, silver ions detach from the anode and migrate electrochemically toward the cathode along microscopic moisture films, creating dendritic whiskers that produce catastrophic short circuits. Shenzhen VUKO guarantees long-term dielectric isolation by printing a complete void-free carbon overcoat over all silver traces, coupled with hydrophobic perimeter adhesive gaskets (e.g., 3M 300LSE/468MP) that create a hermetic boundary against ambient moisture penetration.
Actuation Force vs. Ergonomic Cycling: The tactile snap response of a membrane switch depends on dome geometry (four-leg versus round domes), diameter (typically 6 mm to 12 mm), and spring force rating (typically 220 g to 450 g). While a heavy 400 g dome prevents accidental actuation in heavy-machinery vibration settings, it can cause repetitive strain fatigue in intensive data entry setups. VUKO works directly with your mechanical engineering team to tune actuation forces and specify nickel- or gold-plated domes rated for 1,000,000 to 5,000,000 duty cycles.
Frequently Asked Questions: Industrial Membrane Switch Procurement
Comprehensive engineering, tooling, and commercial guidance addressing the most frequent technical inquiries presented by global original equipment manufacturers (OEMs):
To provide an engineering review and commercial quote within 24 hours, we require: (1) Vector artwork for the graphic overlay detailing Pantone (PMS) or RAL color codes, font vectors, and window cutouts; (2) Mechanical dimensional drawings (DXF, DWG, or STP) displaying key locations, embossing profiles, outer contours, tail exit geometry, and pinout assignments; (3) Schematic or circuit netlist detailing switch intersections, LED polarities, integrated resistors, and connector tail pitch (e.g., 1.0mm, 2.54mm); and (4) Environmental requirements (IP rating targets, UV exposure, chemical contact).
Achieving true ingress protection requires continuous perimeter adhesive sealing combined with specialized moisture-barrier venting channels. We employ premium 3M acrylic transfer adhesives (such as 3M 467MP, 468MP, or 300LSE for low surface energy plastics) around the entire border perimeter, maintaining a minimum 3.0 mm unbroken seal ring. Internal venting between switch cavities prevents dome "pillow effect" (trapped air pressure resisting actuation under temperature changes) while directing breathability either into the customer enclosure or through hydrophobic ePTFE Gore membrane filters.
Polycarbonate offers ease of processing, excellent optical transparency, and is economical for indoor instruments where keys are flat or non-embossed; however, its switch actuation flex life is typically limited to 50,000 to 100,000 cycles before micro-cracking occurs. In contrast, Biaxially Oriented Polyester (PET, such as Autotype Autoflex) delivers exceptional flex fatigue resilience exceeding 5,000,000 actuations without stress whitening, provides superior chemical resistance against industrial solvents, and exhibits far superior thermal stability across -40°C to +85°C operating ambients.
Yes. On standard silver-printed PET layers, we bond miniature 0603 or 0805 SMD LEDs and passives using structural electrically conductive silver epoxy, encapsulated under UV-cured potting epoxy for mechanical shock and vibration protection. For high-density layouts, miniature microcontrollers, capacitive touch ICs, or ultra-fine pitch connectors, we build the membrane switch upon a flexible polyimide (FPC) or rigid FR-4 PCB circuit layer, allowing standard automated SMT reflow soldering and comprehensive automated optical inspection (AOI).
For custom engineering prototypes, hard steel dies are avoided by utilizing precision digital laser cutting and high-resolution digital UV printing, significantly lowering NRE tooling fees. Prototyping batches (5 to 20 units) are typically fabricated, assembled, electrically tested, and dispatched within 7 to 10 business days following mechanical CAD sign-off. High-volume production tooling (utilizing precision male/female steel die punch tools) typically requires 12 to 15 business days for fabrication and qualification.
Orders can be processed directly via Alibaba.com Trade Assurance, providing buyers with end-to-end payment security, strict shipment schedule oversight, and contract compliance guarantees. Furthermore, we maintain commercial carrier contracts with DHL Express, FedEx, and air/sea freight logistics networks to deliver door-to-door delivery with real-time tracking across North America, Europe, Australia, and Asia.
Initiate Your Engineering Consultation & Custom Quotation
Accelerate your project schedule with Shenzhen VUKO Electronics. Upload your design files, graphic layouts, or sample BOMs to receive a comprehensive Design for Manufacturability (DFM) review and formal competitive quotation within 24 hours.