14+
Years International Verified Exporting
< 24h
Engineering DFM Review & Quotation
100%
Electrically Tested (E-Test / AOI)
IP67
Sterilization & Fluid Ingress Barrier
Manufacturing Capabilities
Advanced Electronics & Interface Solutions for Toulouse OEM Hardware
Comprehensive electromechanical manufacturing engineered for clinical diagnostics, aeronautics medical kits, and smart digital health systems.
Engineering High-Reliability Medical Interfaces for the Toulouse MedTech & BioTech Ecosystem
The Occitanie region, anchored by the metropolitan industrial engine of Toulouse, represents one of Europe's fastest-growing ecosystems for advanced clinical technology, biotechnology, and integrated aerospace-grade medical devices. Renowned globally as the European capital of aerospace engineering through Airbus and CNES, Toulouse has simultaneously fostered an elite bio-health corridor spearheaded by the Oncopole campus, the Pierre Fabre research centers, and the University Hospital Complex (CHU de Toulouse). Medical device OEMs situated within this regional corridor design instruments under stringent operational conditions where cross-contamination risks, chemical degradation from aggressive hospital-grade virucidal detergents, and electromagnetic interference (EMI) are critical engineering hurdles.
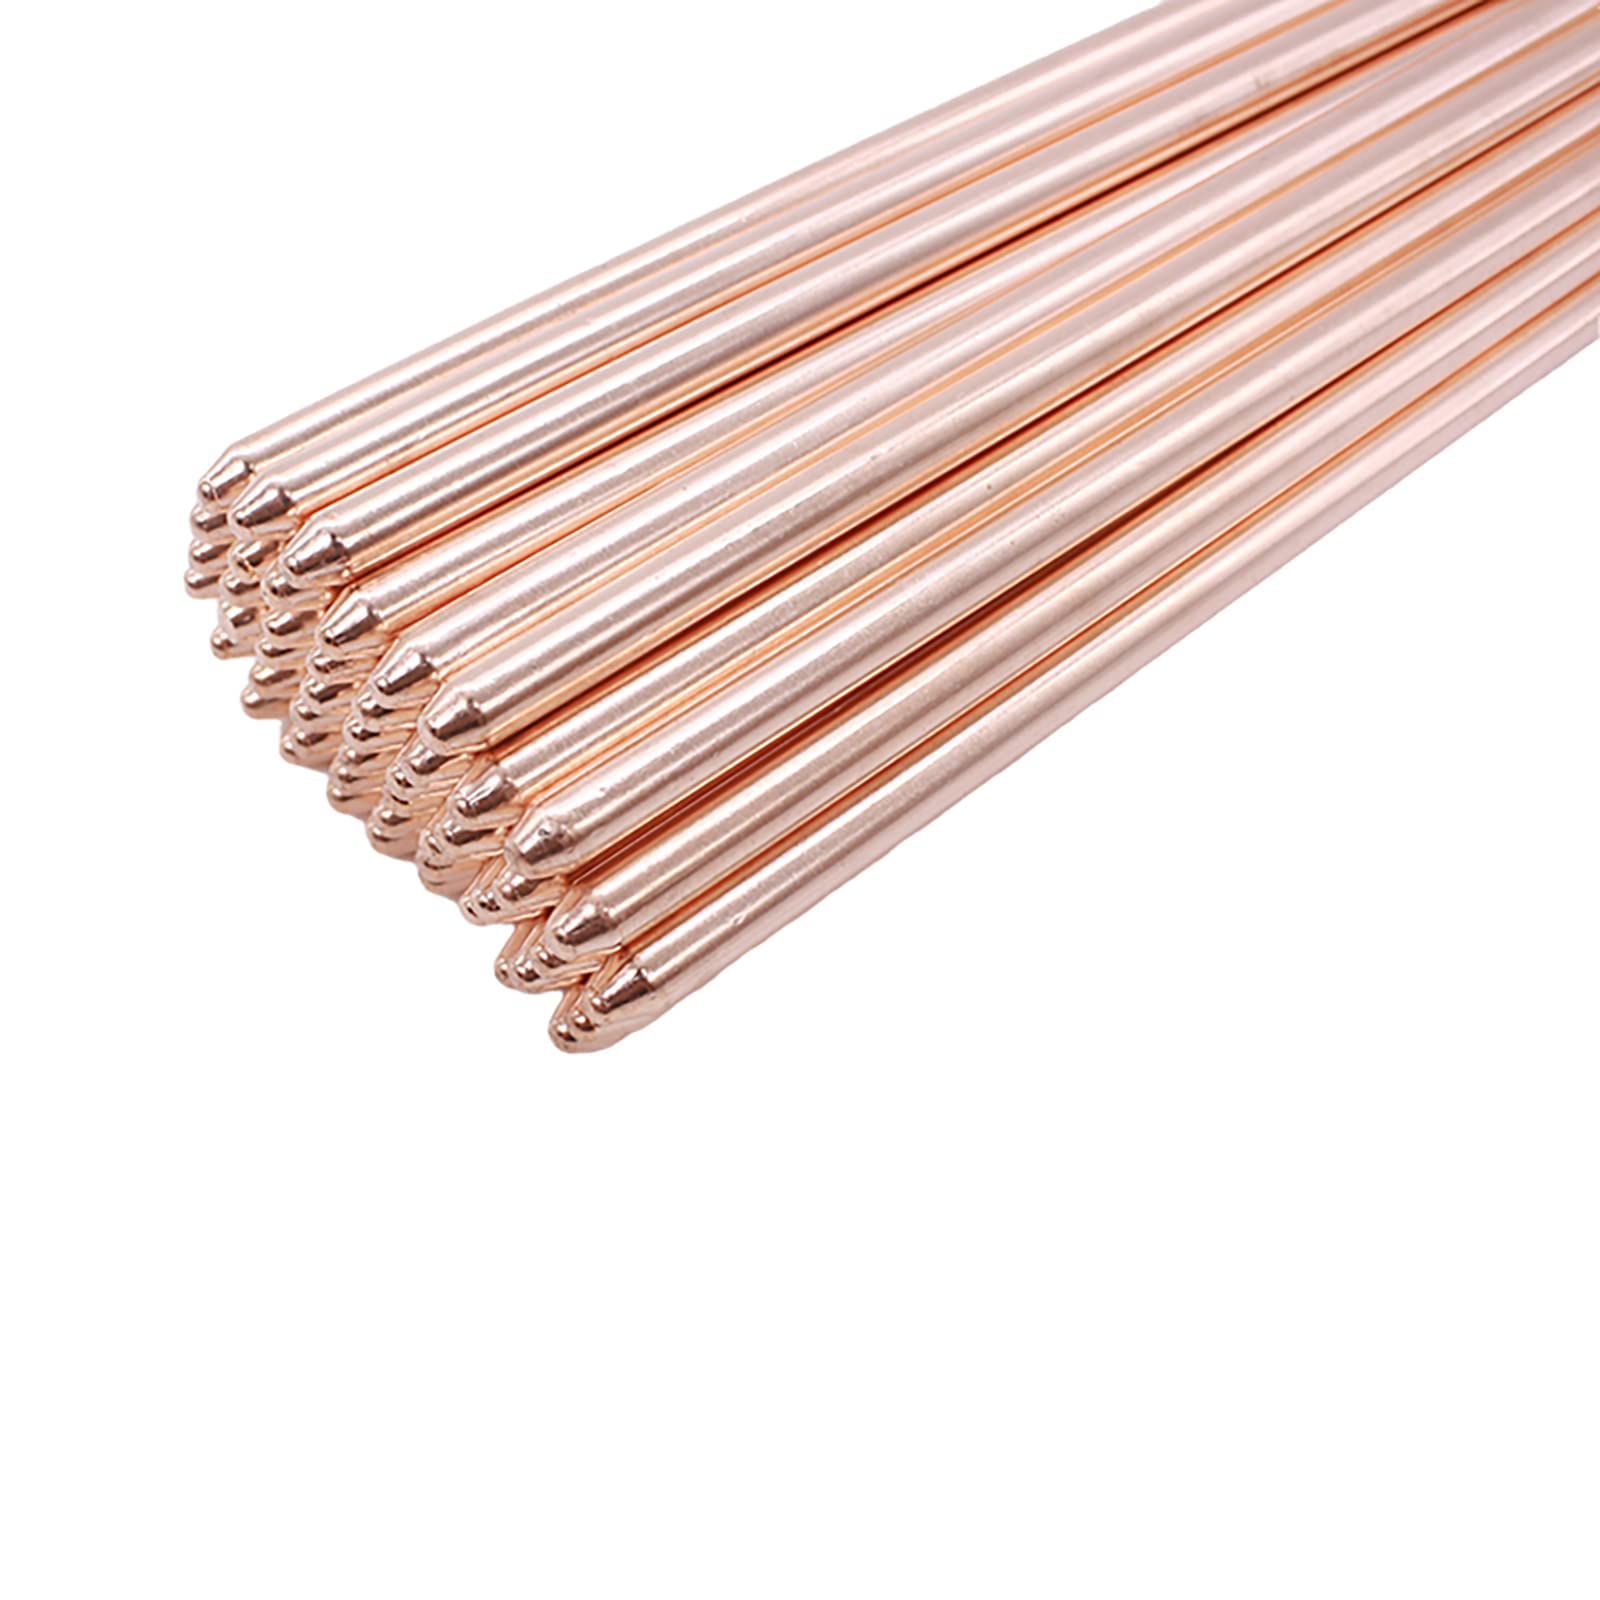
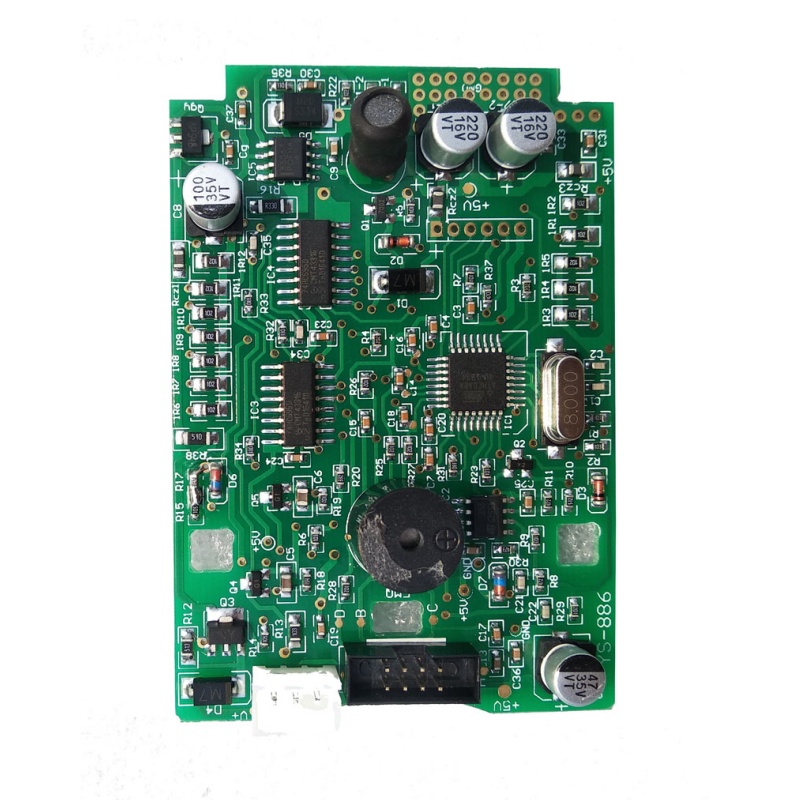
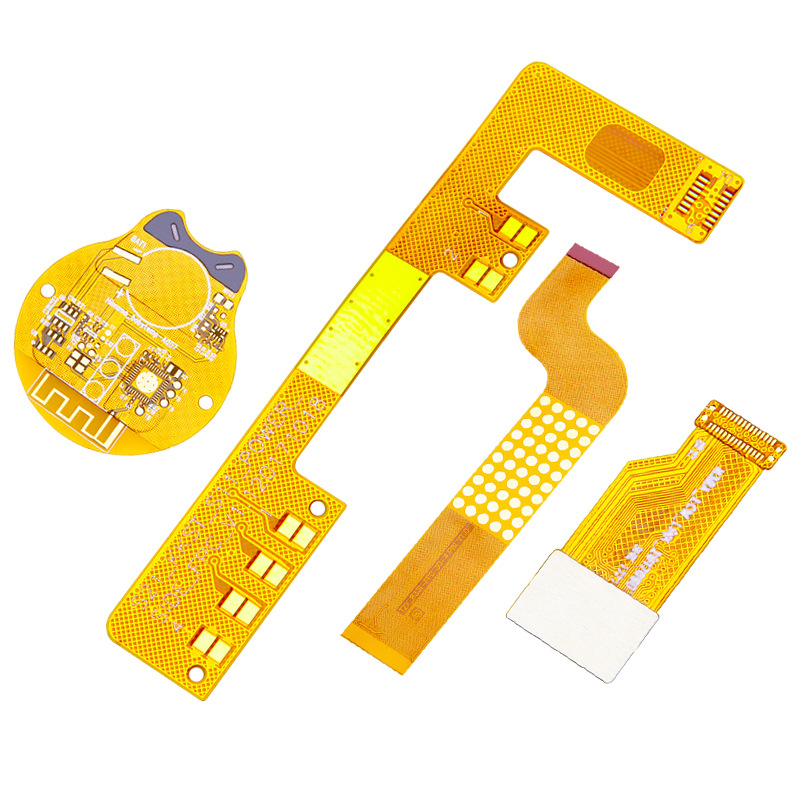
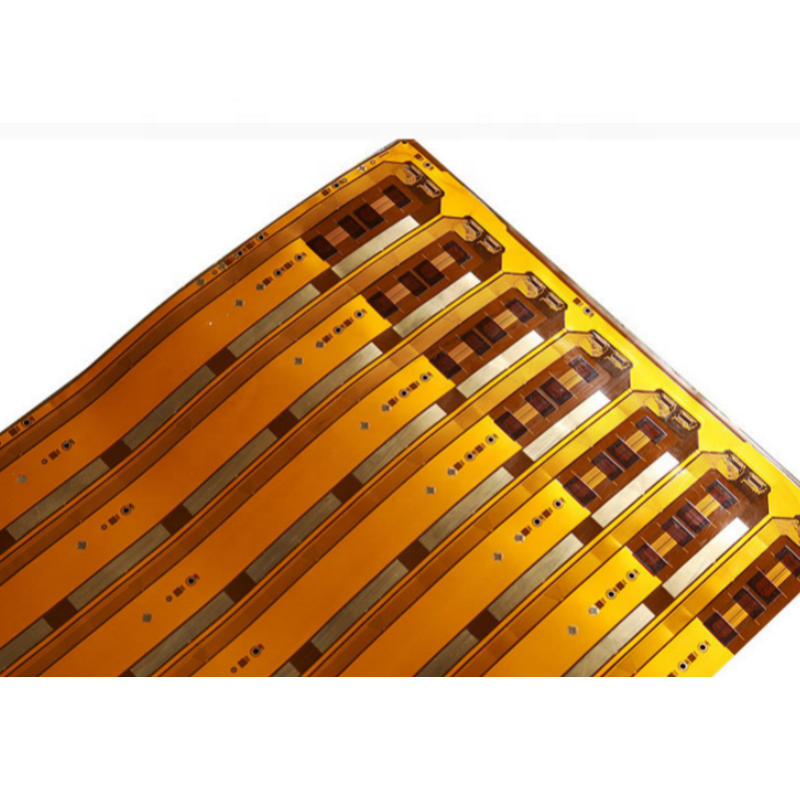
Shenzhen VUKO Electronics Co., Ltd. delivers mission-critical HMI solutions and advanced electronic assemblies engineered specifically to support medical equipment designers across Toulouse, Blagnac, Labège, and Castres. As a CE-certified, ISO 9001-aligned manufacturer backed by more than 14 years of direct international OEM exporting, VUKO bridges high-precision micro-manufacturing with full compliance under the European Medical Device Regulation (EU MDR 2017/745). From multi-layer antimicrobial tactile membrane switches to high-density flex-rigid circuits (FPC) and Peltier-driven thermal control sub-assemblies, our engineering infrastructure delivers the reliability demanded by surgical operating theatres, point-of-care (POC) diagnostics, and aeromedical evacuation pods.
Material Science & Chemical Resistance: Meeting Hospital Sterilization Demands
Standard commercial membrane interfaces rapidly delaminate and suffer optical hazing when subjected to standard clinical sanitation protocols in French medical institutions. Medical hardware deployed in Toulouse hospitals requires daily exposure to oxidizing detergents, quaternary ammonium compounds, hydrogen peroxide vapor (HPV), and isopropyl alcohol (IPA 70%). At VUKO, our medical membrane overlays are precision-fabricated utilizing biaxially oriented textured polyester films (Autotex® / XE Series with antimicrobial silver-ion integration) and medical-grade polycarbonate substrates.
These specialized front overlays present an impenetrable physical barrier (rated to IP65, IP67, and optional IP68) that prevents liquid ingress into the underlying silver conductive traces or tactile metal dome contacts. The graphic surface incorporates UV-cured chemical-resistant inks printed in Class 10,000 cleanroom environments, preventing degradation caused by chlorine-releasing biocides or autoclave condensation cycles common in French paramedical operations.
Technical Benchmark: Medical-Grade vs. Standard Commercial Membrane Switches
| Performance Specification | Commercial Grade Interface | VUKO Medical-Grade Interface (Toulouse Supply) | Clinical Advantage (EU MDR Compliance) |
|---|---|---|---|
| Overlay Material | Standard Graphic PC / PET | Autotex® XE / Antimicrobial Silver-Ion PET | Prevents bio-film colonization; resistant to hospital bleach |
| Ingress Protection (IEC 60529) | IP40 - IP54 | IP65, IP67, up to IP68 Submersible | Complete sealing against blood, bodily fluids, and washdown |
| Tactile Actuation Life | < 500,000 cycles | > 1,000,000 to 5,000,000 cycles (Gold/Nickel Dome) | Maintains tactile feedback through years of intensive emergency use |
| Shielding (EMC / EMI) | Unshielded / Optional Carbon | Continuous Aluminum Foil or Printed Silver Grid | Complies with EN 60601-1-2 medical EMC disturbance thresholds |
| Circuit Substrate | Screen-printed Silver Ink on PET | Silver Ink on PET or High-TG Polyimide FPC | Ultra-low circuit resistance; avoids micro-cracking in mobile units |
| Operating Temperature | -10°C to +50°C | -30°C to +85°C | Supports aeromedical aviation and portable ambulances |
Localized Industrial Application Scenarios Across Toulouse & Occitanie
Engineering teams across Toulouse's tech clusters leverage VUKO's custom electronic assemblies and tactile membrane switches across four primary medical sectors:
Point-of-Care & In-Vitro Diagnostics (IVD)
Toulouse BioTech bioparks develop high-throughput centrifuges, blood analyzers, and automated pipetting systems. These devices require seamless, flat capacitive touch panels or sealed tactile keypads with integrated LED backlighting and clear display windows that can be disinfected between patient sample runs without damaging internal electronics.
Surgical Theatres & Oncopole Clinical Suites
Endoscopic surgical consoles, ultrasonic cavitation scalpels, and electrosurgical generators deployed at CHU de Toulouse demand ultra-reliable tactile feedback. Surgeons operating with thick surgical gloves rely on distinct snap-ratio metal domes (250g to 450g actuation force) to prevent unintended key triggers during critical procedures.
Aeromedical & Mobile Emergency Evacuation Systems
With Toulouse hosting premier aeromedical transport providers, medical monitoring equipment must endure severe altitude pressure differentials, vibration resonance, and extreme temperatures. Our rigid-flex and high-temperature polyimide FPC circuits prevent solder-joint fatigue under high G-forces during helicopter and fixed-wing patient transit.
Technological & Regulatory Trends Driving Toulouse's Medical HMI Sector
As the European Union intensifies regulatory oversight and French medtech startups accelerate artificial intelligence integration, the demand for human-machine interfaces is undergoing a structural transformation across three distinct vectors:
1. The Shift to MDR 2017/745 Traceability and Full Material Disclosure
Hardware developers across Occitanie can no longer procure generic, unverified input devices. Medical Device Regulation (MDR) requires end-to-end bill-of-materials (BOM) transparency, ISO 10993 cytotoxicity validation, and RoHS/REACH compliance documentation. VUKO directly assists European quality compliance directors by providing exhaustive Certificates of Conformance (CoC), material flame ratings (UL 94V-0), and electrical test records for every manufactured lot, mitigating costly audit bottlenecks with notified bodies.
2. Convergence of Tactile Feedback and Capacitive Touch (Hybrid Panels)
Modern clinical diagnostic devices are transitioning from pure mechanical buttons to elegant, wipeable touch surfaces. However, clinical users continue to demand physical, positive feedback for critical functions like emergency stops or infusion rate confirmations. VUKO leads this trend by engineering hybrid panels: combining capacitive touch sensor matrices on flexible PET with integrated tactile metal domes, embedded surface-mount LEDs, and dead-front graphic printing that illuminates only active functional states.
3. Integration of Active Thermal Management in Compact Biomedical Modules
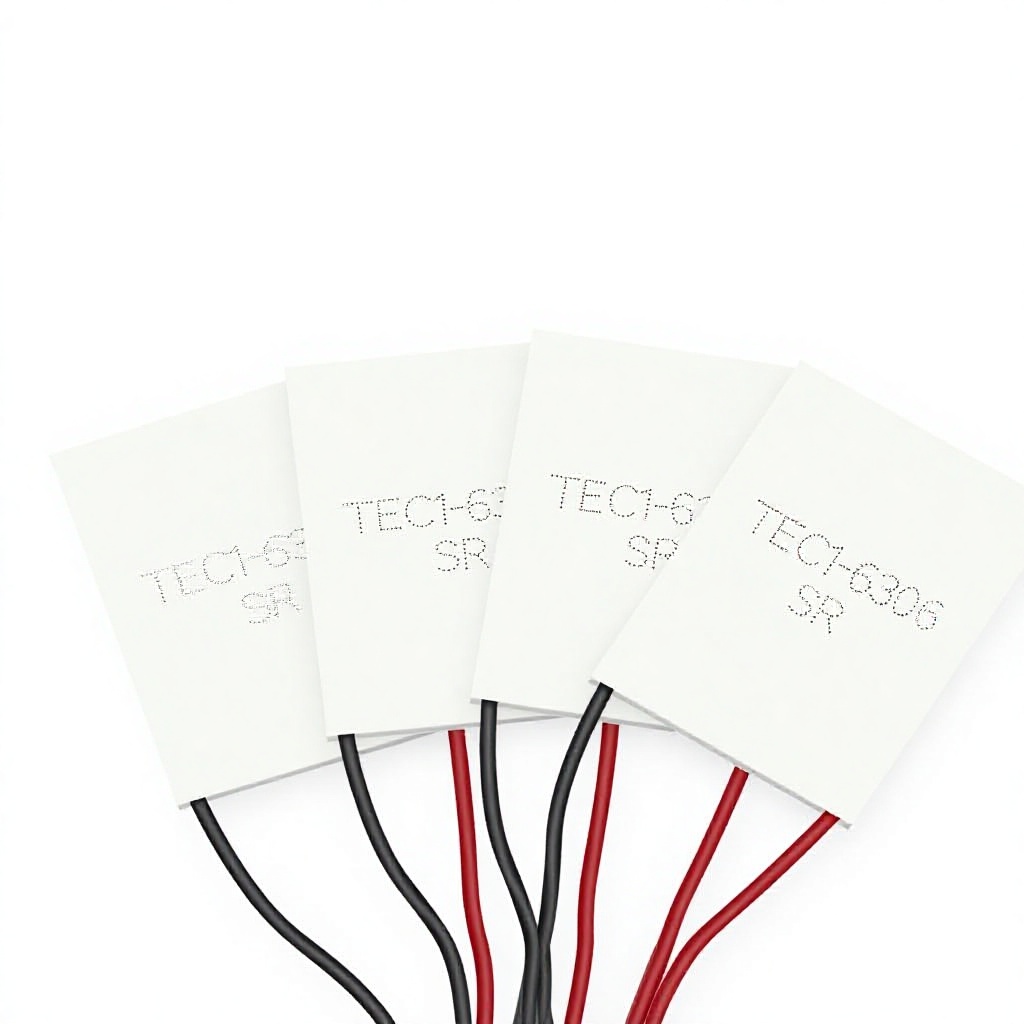
Next-generation DNA sequencers, PCR thermal cyclers, and point-of-care blood cooling devices engineered in Toulouse require precision micro-cooling directly adjacent to electronic logic boards. By pairing our thermoelectric Peltier modules (such as the TEC1 series) and flat copper heat pipes with customized aluminum core PCBs (MCPCB), VUKO offers an integrated thermal-mechanical-electrical package that stabilizes optical sensors and biological reagents without bulky external heat sinks.
Why Toulouse OEMs Partner with Shenzhen VUKO Electronics
Navigating global electronics supply chains requires agility, engineering depth, and uncompromised manufacturing standards. Shenzhen VUKO Electronics Co., Ltd. provides European procurement teams with direct factory-floor advantages:
Engineer-Led DFM Review Within 24 Hours
Before issuing quotes, our senior engineering team reviews your Gerber files, BOM component part numbers, and mechanical switch stack-ups. We catch design-for-manufacturability issues, trace spacing hazards, and obsolete components early, eliminating costly revisions.
Full Turnkey PCBA & BOM Sourcing
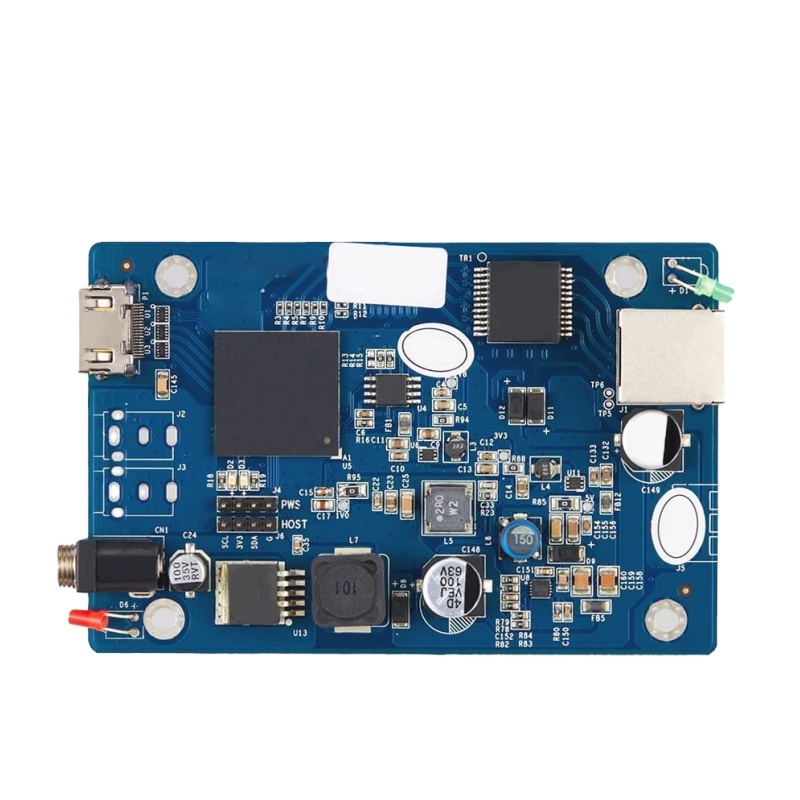
We source authentic components directly from certified global distributors for ICs, passives, and discrete micro-sensors. Combined with automated SMT placement, DIP wave soldering, and functional jig testing, we provide a complete plug-and-play assembly under one roof.
Flexible MOQ from 5 Pcs to Full Volume
Innovation thrives on agile iteration. Unlike large contract manufacturers who reject small pilot runs, VUKO supports MedTech startups and university laboratories in Toulouse with custom prototype quantities starting from just 5 pieces, scaling to tens of thousands seamlessly.
Frequently Asked Questions: Medical Membrane Switches & PCB Assemblies (Toulouse Market)
Q: How does VUKO ensure CE and RoHS compliance for medical hardware shipped to France?
Every membrane switch panel and assembled PCB produced for European buyers is manufactured using compliant base materials, lead-free surface finishes (such as ENIG or Lead-Free HASL), and RoHS-certified non-hazardous inks and laminates. Detailed declaration documents and chemical compliance dossiers are provided with each production batch to support your notified body audits.
Q: Can our team order rapid prototypes before committing to mass production tooling?
Yes. We offer rapid laser-cut and digitally printed prototype runs starting from just 5 pieces. This allows your mechanical and biomedical engineers in Toulouse to validate enclosure fit, tactile force, visual clarity, and connector flex tail routing prior to high-volume die-tooling investments.
Q: What design files are required to initiate an engineering quotation?
For custom membrane switches, we require vector artwork (PDF, AI, or CorelDraw) indicating Pantone/RAL colors, embossing profiles, and graphic windows, accompanied by mechanical CAD drawing (DXF/DWG) for tail routing and circuit layout. For complete PCBA modules, please submit standard RS-274X Gerber files and an Excel BOM with exact manufacturer part numbers.
Q: What is the typical transit lead time from Shenzhen to Toulouse-Blagnac Airport (TLS)?
Following our rapid 5-to-10 day prototype fabrication cycle, express air cargo shipments via our logistics partners (DHL, FedEx, UPS) typically arrive in Toulouse within 3 to 5 business days, complete with international airway tracking and customs clearance support.
Q: How do your switches achieve reliable IP67 moisture sealing against fluid spills?
We incorporate high-adhesion 3M acrylic adhesive transfer films (such as 3M 467MP/468MP or 3M 300LSE for low surface energy plastics) around the complete outer perimeter of the switch assembly. This gasket barrier isolates the inner tactile metal domes and silver conductive traces from fluids, biohazards, and internal humidity.