Solid-State Illumination
Engineered for high duty-cycles, ingress resistance, and seamless electromechanical integration across international hardware standards.
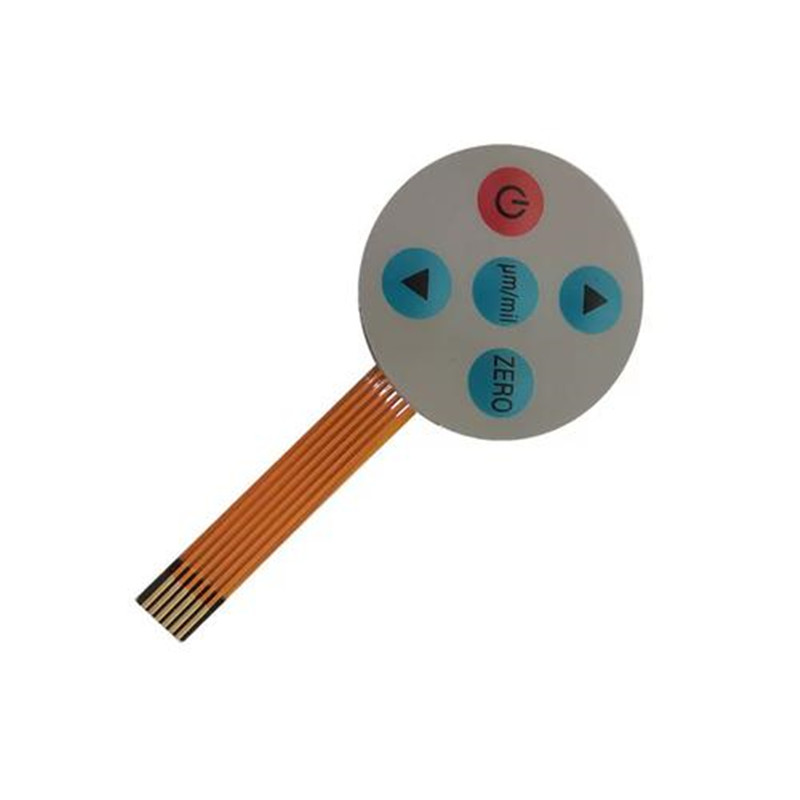
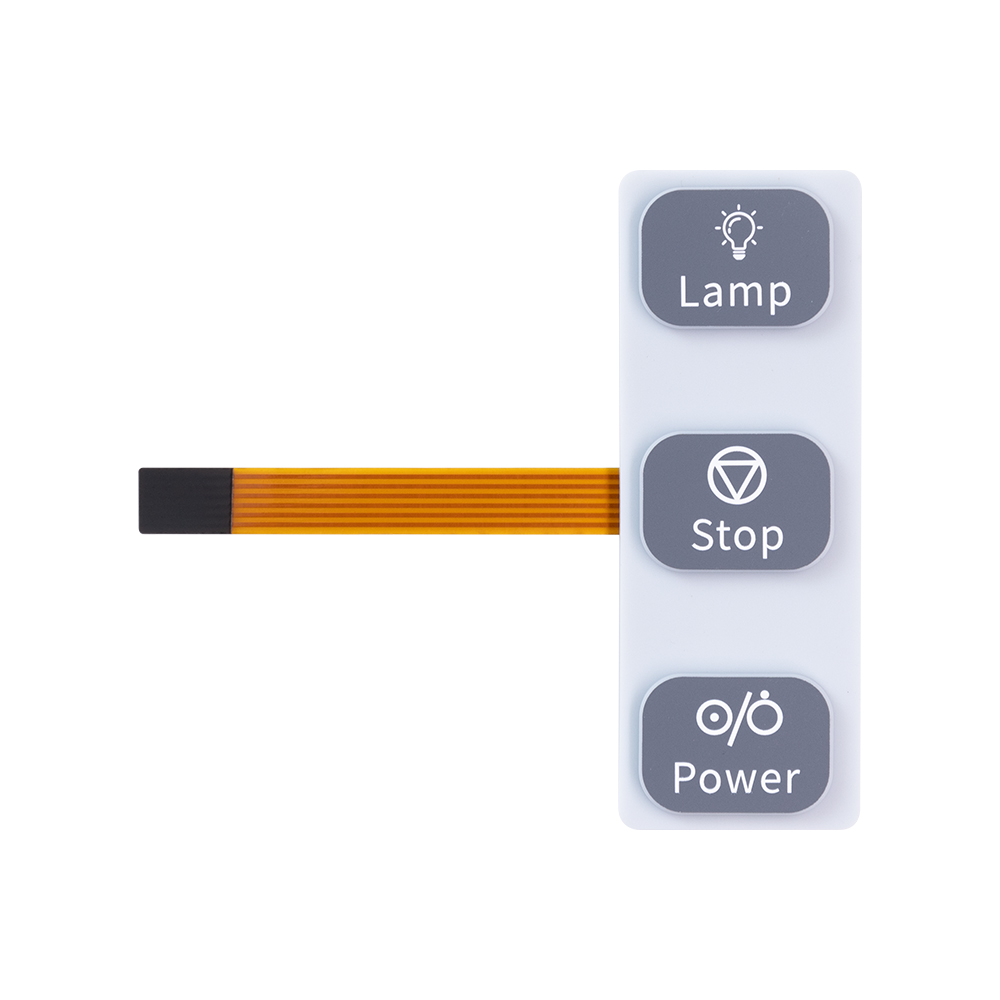
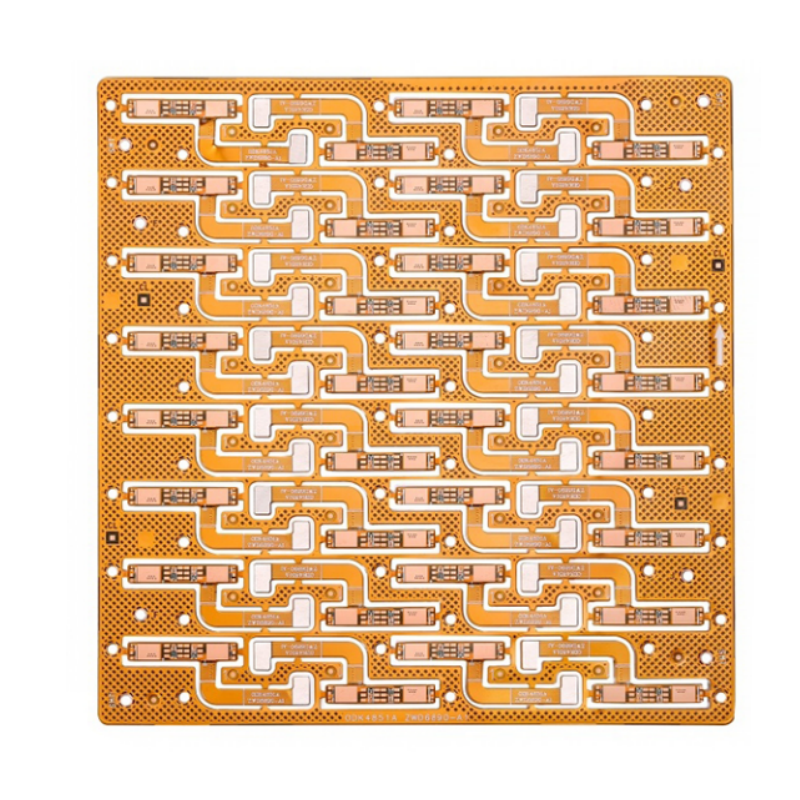
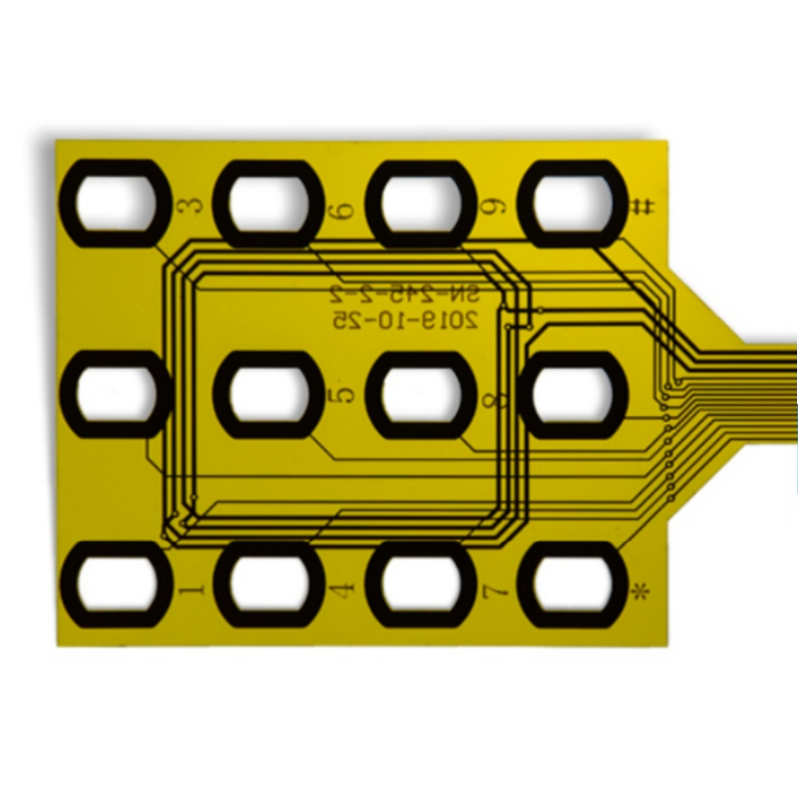
In modern industrial instrumentation, human-machine interface (HMI) surfaces are frequently exposed to physical abrasion, chemical solvents, wide thermal cycling, and continuous mechanical deflection. A standard consumer-grade interface quickly suffers from silver migration, trace fracture, or graphic delamination. Serving clients throughout the Kingston industrial landscape, VUKO Electronics engineers membrane keypads built upon a sophisticated multilayer composite architecture.
The foundation typically begins with an Autotype or transparent polyester (PET) graphic overlay, treated with fine-texture, antiglare, or hardcoat chemical finishes (resistant to isopropyl alcohol, commercial sanitizers, and hydrocarbons). Beneath the graphic layer, high-grade 3M adhesive transfer systems (such as 3M 467MP or 468MP) provide high-shear strength bonding, preventing bubble formation under atmospheric shifts. For the critical switching core, nickel-plated or gold-plated stainless steel metal domes are precisely fixed inside spacer matrices, delivering positive tactile feedback (actuation forces variable from 250g to 500g) while sustaining over one million actuations without micro-cracking.
Unlike basic silver-paste screen printing on flimsy substrates, our top-tier configurations deploy Flexible Printed Circuit (FPC) tails using copper-clad Polyimide (PI). Copper-etched traces prevent trace resistance degradation and guarantee zero risk of silver dendrite short-circuits under continuous Caribbean humidity. The terminal tail features tailored connector pitches (such as 1.0mm, 1.27mm, or 2.54mm locking ZIF/LIF terminals), reinforced with polyimide, FR4, or stainless steel backer stiffeners to endure repetitive vibration and assembly insertion stress.
How our custom flexible interfaces and ruggedized PCBAs perform within demanding environments across key Kingston operational sectors.
Keypads on terminal crane controls, weighbridges, and container yard telemetry interfaces operate under high airborne salt fog and intense UV exposure. Our UV-stabilized outdoor overlays and IP67 rim-sealed gaskets completely isolate internal conductive switches from coastal corrosion.
Processing units, bottling telemetry, and brewing equipment demand routine washdown cycles with caustic cleaning detergents. Our non-porous PET membranes withstand steam cleanings and chemical washdowns without graphic bleaching or liquid permeation into the logic circuits.
Diagnostic laboratory devices, dental control units, and patient monitoring consoles throughout Kingston hospitals rely on smooth, antimicrobial-coated membrane touchpads. Flush surface designs eliminate biological particulate traps, making rapid disinfection effortless.
Unattended payment systems, automated gate controls, and petroleum pump terminals demand anti-vandal, high-actuation keypads. We incorporate internal ESD shielding layers (aluminum foil or carbon grid) that discharge up to 15kV, shielding motherboard microcontrollers.
High temperatures inside tropical outdoor utility enclosures cause typical elastomer switch buttons to degrade. Our membrane keypads remain functionally rated between -30°C and +80°C, offering steady tactile snap and long-term circuit stability in clean energy infrastructure.
Across the Caribbean economic corridor, industrial operations are modernizing legacy infrastructure through IoT-enabled monitoring, predictive maintenance nodes, and smart power management systems. This digital transformation introduces three decisive trends for Kingston procurement managers and hardware design teams:
1. Shift Toward Hybrid FPC Interfaces: The Caribbean's humid climate accelerates galvanic degradation when conventional silver-printed ink contacts are operated in high duty-cycle environments. As a result, engineering teams are transitioning directly to Polyimide-based FPC substrate keypads with gold-plated contact pads. Although marginally higher in initial tooling, FPC variants deliver virtually zero failure rates and dramatically lower whole-life replacement costs.
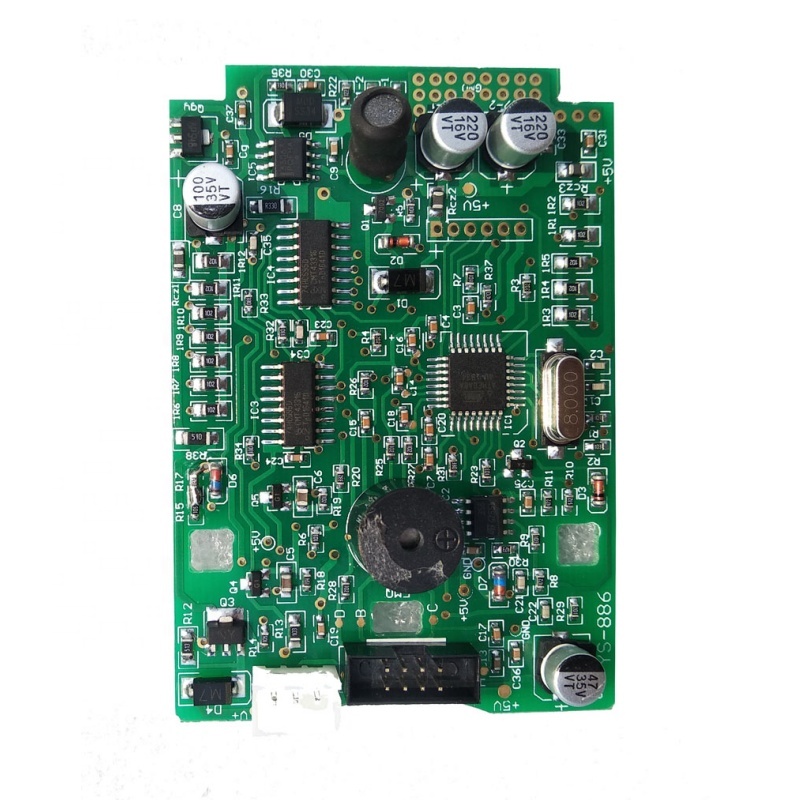
2. Consolidation of HMI and SMT Backplanes: OEMs are eliminating unnecessary wire harnesses between front-panel switches and back-end logic boards. By pairing a tactile membrane interface directly to our custom rigid-flex or surface-mount PCBA modules, developers cut assembly times by over 40%, shrink enclosure depth, and bypass fragile board-to-wire assembly steps.
3. Demand for Turnkey Component Sourcing and Rapid DFM: Managing multiple offshore vendors for raw PCBs, metal domes, graphic printing, and passives strains Caribbean supply chains. Kingston engineering enterprises increasingly rely on single-source partners capable of delivering verified bare boards, turnkey SMT assembly, circuit cloning, and enclosure gasket lamination with comprehensive design-for-manufacture (DFM) verification completed prior to fabrication.
Direct from our high-density electronics manufacturing hub in Shenzhen to your loading docks in Kingston.
Over 14 consecutive years of verified export manufacturing. Secure transaction handling through Alibaba Trade Assurance ensures full capital and on-time shipment security.
Direct supply line access to authentic active ICs, passive chips, connectors, and LED indicators. Rapid identification of obsolete or long-lead parts with vetted drop-in alternates.
Automated Optical Inspection (AOI), Flying Probe electrical tests, key actuation force gauges, insulation resistance testing (>100MΩ at 100VDC), and complete functional test fixture builds.
Rapid R&D sample batches starting from just 5 pieces. Smooth scalability into hundreds of thousands of production units with consistent color, tactile, and dimensional fidelity.
Essential technical, logistics, and tooling answers to guide your custom flexible membrane keypad order.
Get a comprehensive Design for Manufacturability (DFM) review, material stack-up consultation, and an accurate quote within 24 hours. Send your design parameters or schedule an engineering consultation with our technical specialists.
Ready to review drawings, mechanical tolerances, or BOM specs?
Send an Inquiry