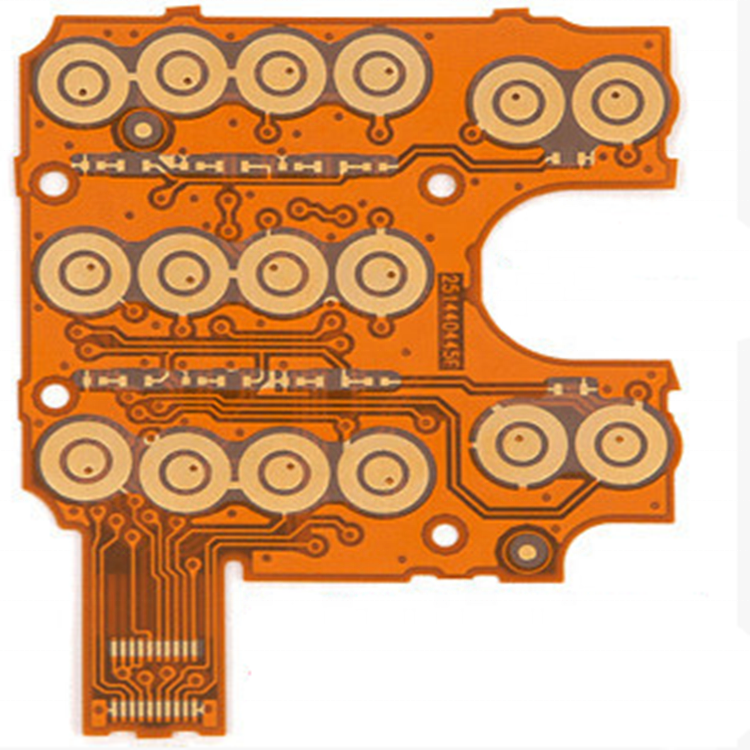
Enterprise Hardware Stack
Industrial-Grade Switches & Precision Electronics
Direct from our Shenzhen ISO 9001 certified manufacturing facilities to engineering firms, ocean technology clusters, and system integrators in St. John’s, Mount Pearl, and Conception Bay South.
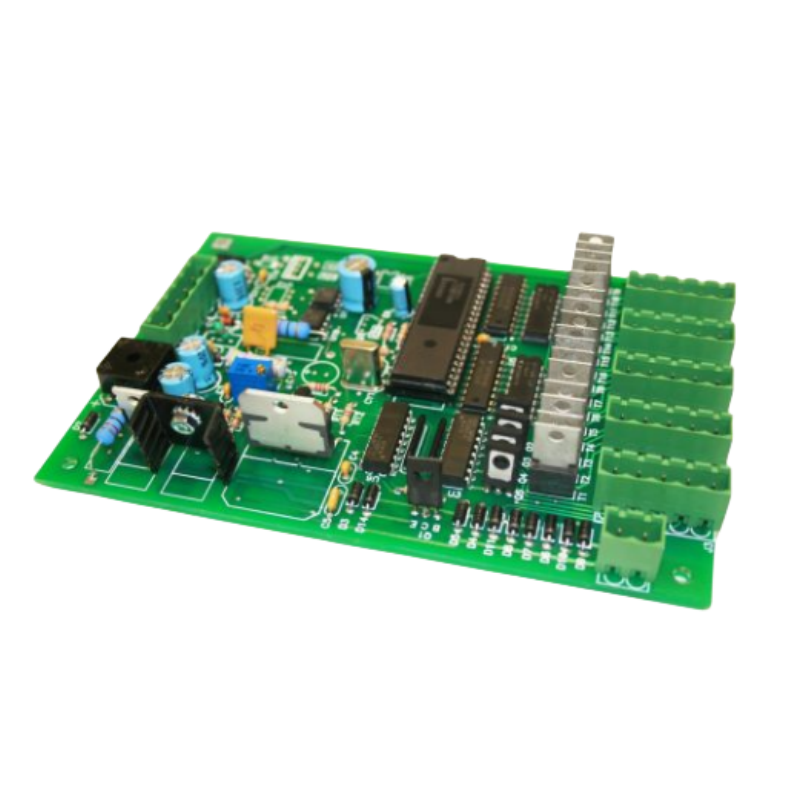
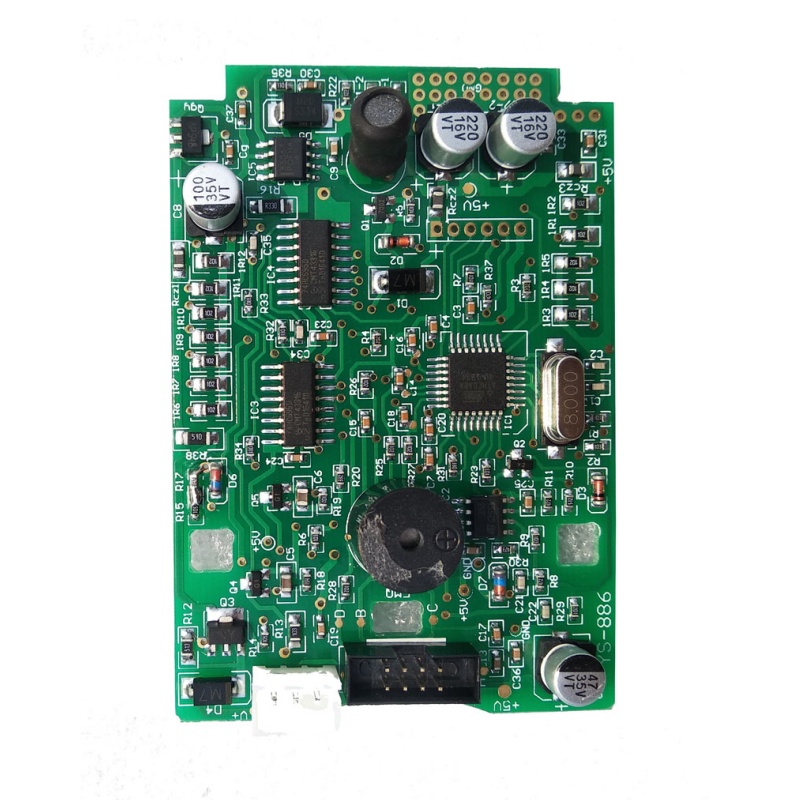
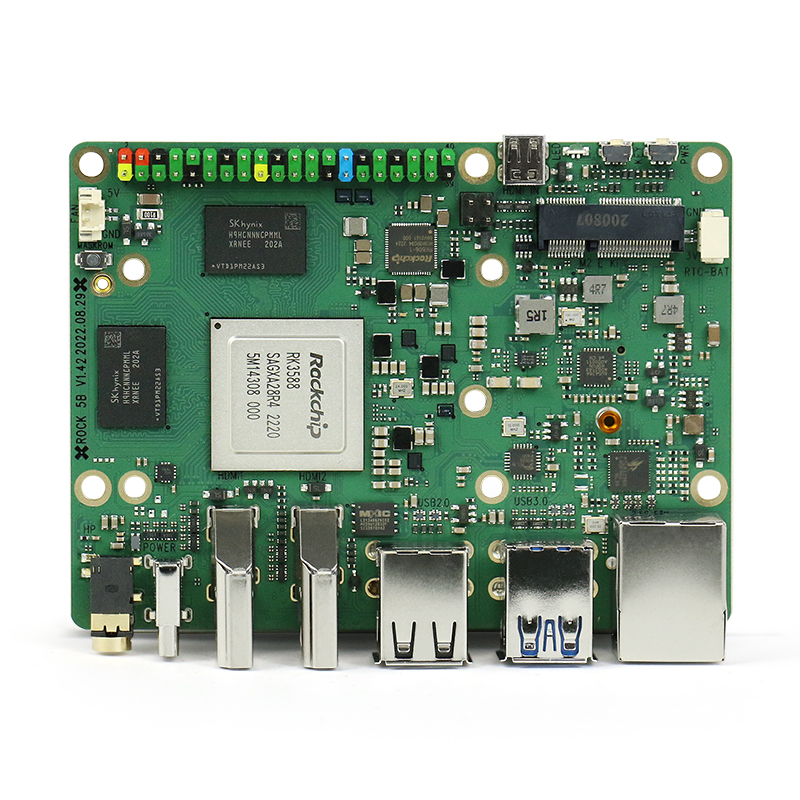
14+
Years Global OEM & Export Track Record
5 Pcs
Ultra-Low MOQ for Rapid NPI Prototypes
<24h
DFM Engineering Review & Quotation Turnaround
100%
Flying Probe, E-Test, AOI & Actuation Life Verified
Engineering Demands in the St. John’s Market: Cold-Ocean, Marine, and Subsea HMI
The capital city of Newfoundland and Labrador, St. John’s, stands as one of the world's preeminent hubs for marine engineering, offshore energy exploration, oceanographic science, and subsea robotic innovation. From maritime institutes along the Avalon Peninsula to offshore platforms operating in the brutal Jeanne d’Arc Basin, electronic user interfaces are subjected to conditions that conventional consumer keypads cannot survive. The convergence of sub-zero North Atlantic temperatures, persistent salt-fog corrosion, high mechanical shock from sea vessel thrusters, and stringent hermetic sealing mandates requires membrane keypad switch manufacturing with zero tolerance for mechanical or dielectric fatigue.
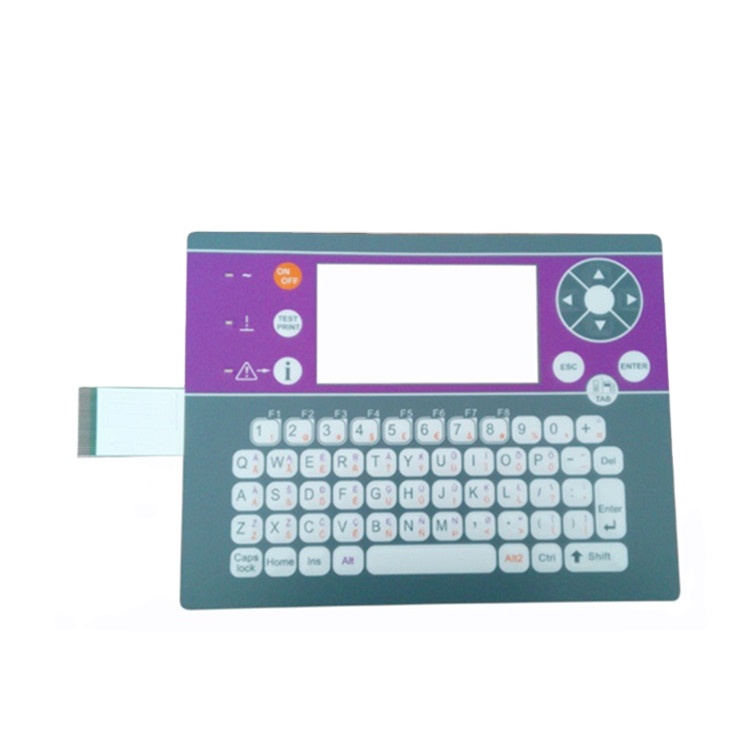
Local procurement managers, electrical engineers, and hardware project leads across St. John’s face a structural bottleneck: domestic Canadian fabrication runs often carry prohibitive NRE tooling charges and inflexible volume minimums, while unvetted overseas brokers fail to provide verifiable material certifications, accurate impedance controls, or ingress resistance validation. Shenzhen VUKO Electronics Co., Ltd. solves this dilemma by bridging tier-one Shenzhen electronics fabrication scale with specialized cold-ocean engineering support. By delivering tailored membrane switch assemblies built on robust polyimide (FPC) or silver-printed polyester (PET) backers, VUKO equips St. John’s high-tech marine operators with ruggedized Human-Machine Interfaces (HMIs) built to military, maritime, and subsea criteria.
Information Gain Insight: While typical membrane switch suppliers quote standard 20°C operating ratings, offshore installations in the Grand Banks encounter cyclical thermal swings from -35°C to +40°C. Standard acrylic transfer adhesives suffer glass transition embrittlement below -10°C, causing overlay delamination and moisture capillary suction. VUKO specifies sub-zero modified 3M 467MP/468MP and 3M 300LSE adhesive stacks rated down to -40°C, preventing seal compromise during maritime freeze-thaw cycles.
Hermetic Ingress Sealing (IP67/IP68)
Continuous perimeter gasket venting routed toward controlled dessicant chambers prevents salt fog, seawater spray, and washdown chemicals from penetrating silver trace matrices.
Tactile Feedback in Gloved Use
Stainless steel metal domes with snap-ratio actuation forces (350g–500g) and embossed poly keys give maritime operators decisive tactile confirmation even through heavy neoprene gloves.
Subsea ROV & Console Resilience
Autotex XE UV-resistant textured films coupled with anti-microbial coatings prevent yellowing, crazing, and chemical breakdown under offshore UV index and engine solvent exposure.
Localized Industrial Applications: Where St. John’s Integrates VUKO HMIs
Hardware development in St. John’s is characterized by specialized, high-reliability industrial deployment. The geographical, climatic, and industrial reality of Newfoundland dictates precise engineering specifications across multiple key sectors:
1. Autonomous Underwater Vehicles (AUVs) and Oceanographic Probes
Research institutes along Logy Bay Road and technology parks in Mount Pearl produce world-class seabed mapping robots, gliders, and acoustic positioning sensors. When surface field crew pre-configure telemetry parameters on open vessel decks, the local input panels cannot allow water droplets to simulate capacitive touches. VUKO delivers dual-technology panels combining high-reliability tactile metal-dome membrane switches with FPC tails that mate directly into hermetically sealed subsea pressure vessels via watertight bulkheads.
2. Offshore Supply Vessels (OSV) & Rig Deck Controls
In harsh marine environments like the Hibernia, Hebron, or White Rose offshore oil fields, auxiliary pumps, winches, and navigation bridge transceivers demand non-sparking, intrinsically safe user consoles. VUKO engineers explosion-proof low-voltage membrane keypads with embedded static shielding layers (aluminum foil or carbon-mesh ground planes) that dissipate Electrostatic Discharge (ESD > 15kV) before spikes can penetrate sensitive microcontroller PCBA boards.
3. Labrador Mining & Remote Cold-Weather Extraction
Labrador’s iron ore facilities and remote northern infrastructure require human interfaces capable of operating in unheated mining cabs and mobile crushing plants. Membrane switches engineered with polycarbonate (PC) become fragile in extreme cold; therefore, VUKO utilizes high-flex biaxially-oriented polyester (PET) graphics overlays that retain flexibility down to -40°C without micro-cracking across millions of actuations.
4. Commercial Fisheries & Aquaculture Processing Equipment
Seafood packaging plants throughout Eastern Canada utilize high-pressure, caustic hot-water sanitization cycles daily. Traditional electromechanical switches rapidly accumulate bio-film and fail due to seal degradation. Our flush, seamlessly laminated membrane surfaces with chemical-resistant overlay films (resistant to bleach, isopropyl alcohol, and sodium hydroxide) provide a cleanable, crevice-free surface that maintains hygiene while eliminating water ingress risks.
| Performance Parameter | Standard Commercial Membrane | VUKO St. John’s Cold-Ocean Grade | Engineering Benefit |
|---|---|---|---|
| Operating Temperature | 0°C to +50°C | -40°C to +85°C continuous | Prevents frozen trace micro-fractures in offshore winter |
| Adhesive Lamination | Standard Water-Base Acrylic | 3M 467MP / 3M 300LSE Structural | Zero edge lifting under salt-fog and thermal cycling |
| Circuit Substrate | Screen-Printed Silver on PET | Flexible Printed Circuit (FPC) Cu/PI | Drastically lowers contact loop resistance (<0.5Ω vs 100Ω) |
| Ingress Protection | IP40 - IP54 (Dust resistant) | IP67 to IP68 certified | Withstands pressurized saltwater washdowns |
| Switch Actuation Life | 500,000 actuations | 1,000,000 to 5,000,000 cycles | High-nickel stainless steel snap domes provide longevity |
| ESD Protection | None / Basic spacer | Full Carbon/Alu Shield Layer (>15kV) | Shields sensitive PCBA MCU from spark damage |
Technological & Procurement Trends Shaping the St. John’s HMI Market
The hardware development landscape in Atlantic Canada is undergoing rapid modernization, fueled by venture capital in blue tech, federal ocean supercluster initiatives, and the migration toward Internet of Things (IoT) edge telemetry. Three major technical shifts are directly altering how local engineering teams specify and procure membrane keypads:
1. Migration from Silver Ink to FPC Substrates
While screen-printed conductive silver paste on polyester is cost-effective for indoor controls, marine vibration and thermal expansion induce microscopic silver migration (electromigration). St. John’s developers are systematically upgrading to copper-clad Polyimide Flexible Printed Circuits (FPC) as the backer layer, ensuring zero silver migration and enabling SMD micro-LEDs to be soldered with high reliability.
2. Hybrid Turnkey Integration: HMI + PCBA Assembly
Hardware teams no longer want to source membrane overlays from one printing house, bare PCBs from another, and mount SMD drivers at a local assembly shop. The trend leans overwhelmingly toward turnkey box-build solutions where VUKO laminates the graphic keypad directly onto the rigid FR-4 backer or aluminum core board, complete with surface-mounted controllers, connectors, and conformal coatings.
3. Low-Volume High-Mix (HMLV) Prototyping Flexibility
Because ocean innovation projects produce specialized exploratory batches (ranging from 10 to 500 units annually), hardware designers are penalised by rigid domestic setups. VUKO champions digital overlay proofing, laser steel-die plotting, and a baseline 5-piece MOQ, accelerating New Product Introduction (NPI) cycles for Memorial University spin-outs and local commercial R&D teams alike.
Precision Manufacturing Flow: From Artwork Proof to IP67 Seal
Traceable manufacturing safeguards every single membrane switch, PCB, and turnkey PCBA delivered to St. John’s. Below is our verified cleanroom assembly cycle:
01. Laser Film Exposure
Digital artwork color matching & laser plotting.
02. Class 10k Printing
Sub-surface reverse graphic overlay printing.
03. Silver / Carbon Ink
Conductive circuit curing & anti-abrasion carbon overcoat.
04. Automated SMT / LED
Ultra-compact 0402 / 0603 LED placement & bonding.
05. Hydro-Embossing
Rim & pillow key tactile embossing under thermal control.
06. Metal Dome Array
Gold/nickel plated snap dome insertion with spacer seals.
07. AOI & Electrical E-Test
100% loop resistance, open/short & LED test verification.
08. Vacuum ESD Packaging
Moisture-barrier vacuum packaging for safe transatlantic transit.
Why St. John’s Procurement Teams Partner with Shenzhen VUKO Electronics
Shenzhen VUKO Electronics Co., Ltd. is not merely a component assembler; we act as an extended engineering and supply chain department for global OEM clients. Based in the epicentre of the world's electronics supply network in Shenzhen, we bring distinct structural advantages to Atlantic Canadian businesses:
14+ Years Verified Factory
Onsite-verified manufacturer with direct export authority, accredited under ISO 9001 and compliant with RoHS, REACH, and CE standards.
Full BOM Sourcing Power
Eliminate component brokers. We source authentic ICs, passives, connectors, displays, and thermal peltiers directly from franchised global lines.
Alibaba Trade Assurance
Risk-free procurement for Canadian buyers: orders can be placed via Trade Assurance with complete payment safeguarding and on-time shipment guarantees.
Direct DFM Engineering
Get direct English-language review of Gerber files, mechanical tolerances, and graphic artwork within 24 hours, catching issues before copper etching.
Frequently Asked Questions: Sourcing Membrane Switches in St. John’s
Direct technical answers addressing lead times, shipping logistics, material reliability, and engineering documentation for Canadian purchasing agents.
What CAD/artwork files are required to initiate a custom membrane switch quote? +
To provide an exact quote and complimentary Design for Manufacturability (DFM) check within 24 hours, our engineering team requires:
- Graphic Artwork: Vector files (.AI, .PDF, or .DXF) detailing key dimensions, window placements, Pantone/RAL color codes, and embossing profiles.
- Circuit Schematic: Gerber files (RS-274X) or 1:1 CAD trace layouts detailing pitch, contact resistance constraints, pinout mapping, and tail length.
- Component Schedule: Specifications for integrated surface-mount LEDs, resistors, EMI shielding layers, or connector termination headers (e.g., Nicomatic, Berg, or FCI 2.54mm pitch).
How does VUKO protect membrane keypads against salt spray corrosion in maritime Atlantic Canada? +
For St. John's ocean tech and offshore marine customers, we implement a multi-stage defense stack:
- Perimeter Gasket Isolation: An unbroken 3M marine-grade acrylic adhesive perimeter seal that prevents moisture capillary ingress.
- Carbon Inking Overcoat: Printed conductive silver tracks are sealed with an anti-abrasive, chemically inert carbon past layer, preventing oxidation and dendritic silver migration.
- Hermetic Tail Transitions: The flexible tail exit features silicone potting or hot-melt encapsulation to eliminate the common failure point where flex tails interface with metal housings.
- Sub-Zero UV Overlays: Autotex XE or 0.18mm–0.25mm textured polyester films that resist salt crusting and extreme UV radiation without yellowing or cracking.
What are typical prototype lead times and international shipping windows to Newfoundland? +
Standard prototype iterations (5 to 20 units) are typically fabricated, assembled, and electrically verified in 7 to 10 working days following DFM sign-off. Volume production runs take approximately 15 to 20 working days. For delivery to St. John's, Mount Pearl, or Gander, we dispatch via priority air couriers (DHL Express, FedEx International Priority, or UPS Worldwide Saver) which clear Canadian customs in Halifax/Montreal and arrive at St. John's facilities in 3 to 5 business days. DDP (Delivered Duty Paid) arrangement is available upon request.
Can VUKO provide turnkey assemblies that integrate rigid PCBA boards with membrane keypads? +
Yes. One of our core strategic competitive advantages is full turnkey mechatronic integration. Rather than forcing you to handle secondary assembly, VUKO can produce the multi-layer FR-4 or aluminum PCB, source all SMT components through our BOM procurement channels, perform automated pick-and-place soldering, apply conformal coatings (silicone, acrylic, or polyurethane), and permanently bond the waterproof membrane keypad onto the rigid assembly. The complete unit arrives 100% functionally tested as a single drop-in subassembly.
What is the Minimum Order Quantity (MOQ) for custom prototypes or legacy replacements? +
Our minimum order quantity starts at just 5 pieces for custom membrane switch prototypes, FPC flex boards, and bare PCB fabrications. We understand that St. John's maritime engineering and specialized instrumentation development often operate in low-volume, high-mix cycles where requiring 1,000 units is unrealistic. We fully support low-volume prototyping and scale seamlessly into batches of tens of thousands of units as your deployment expands.
How do you handle obsolescence and PCBA reverse engineering for older vessel consoles? +
For legacy marine control panels where original engineering drawings, Gerber data, or BOM lists have been lost, VUKO provides full PCBA cloning and reverse engineering services. You can send an intact physical sample to our Shenzhen laboratory. Our engineers will extract netlists, generate complete multi-layer Gerber schematics, identify modern drop-in replacements for obsolete microcontrollers or passive components, and re-manufacture drop-in replacement units that match original mechanical mounting dimensions.
Ready to Build Custom Membrane Keypads for the St. John's Market?
Accelerate your marine, subsea, or industrial hardware timeline. Upload your mechanical drawings, Gerber files, or BOM specifications for a comprehensive DFM evaluation and quote within 24 hours.