High-Reliability Human-Machine Interface Solutions
Membrane Switch Manufacturer & Suppliers serving the Galway market
Precision engineered tactile keypads, IP67/IP68 sealed graphic overlays, flexible printed circuits, and complete box-build PCB assembly solutions tailored for Galway's world-leading MedTech and precision engineering sectors.
Integrated Electronics Stack
High-Performance Interface & Electronic Hardware Portfolio
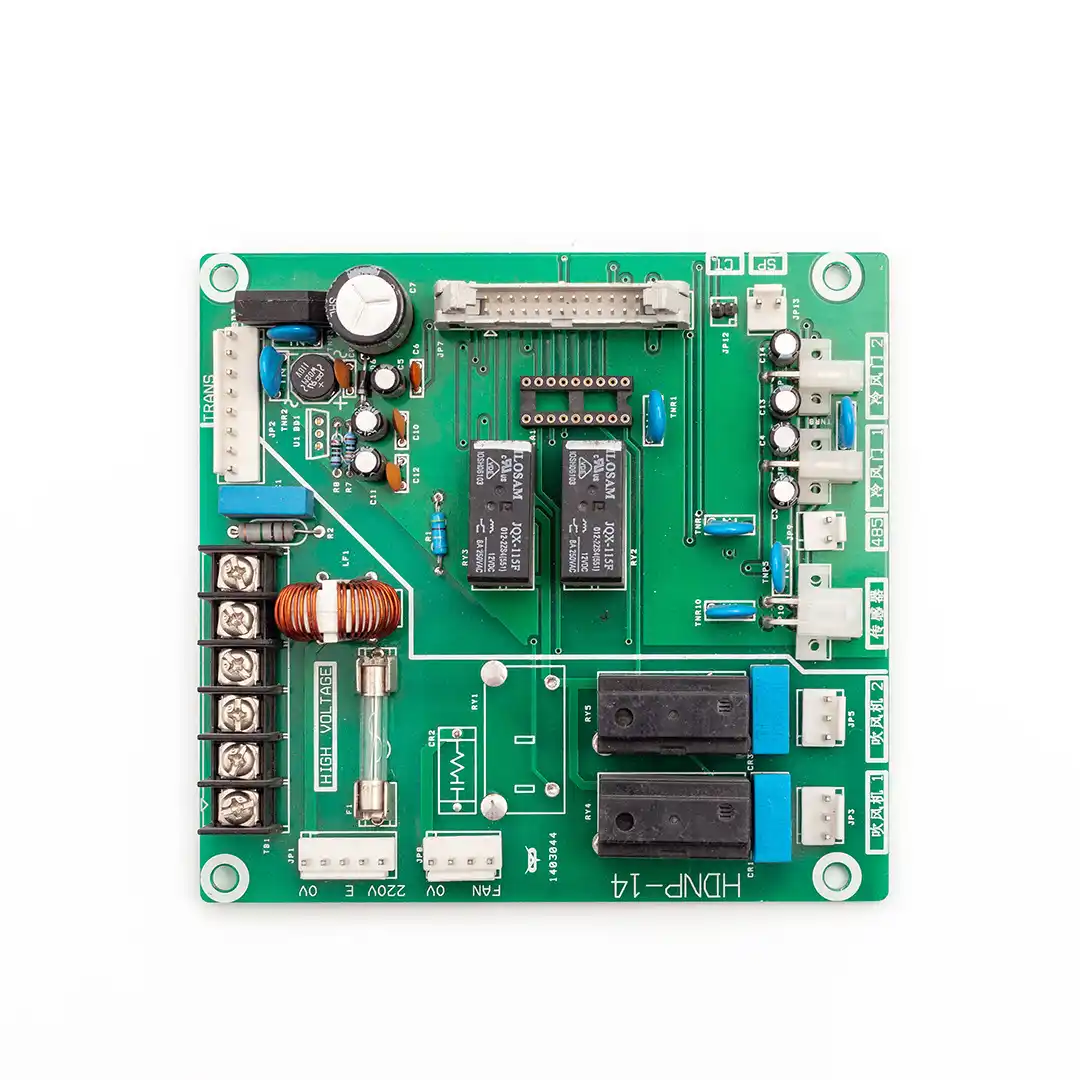
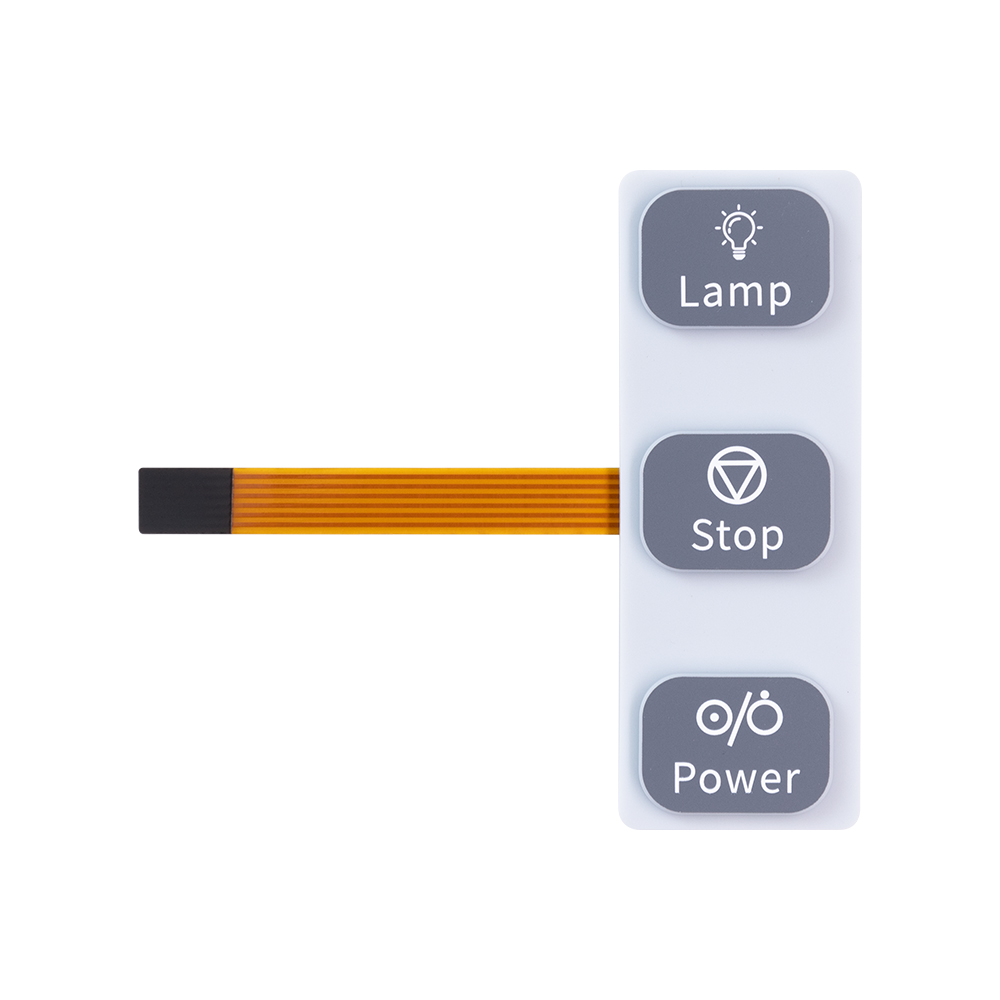
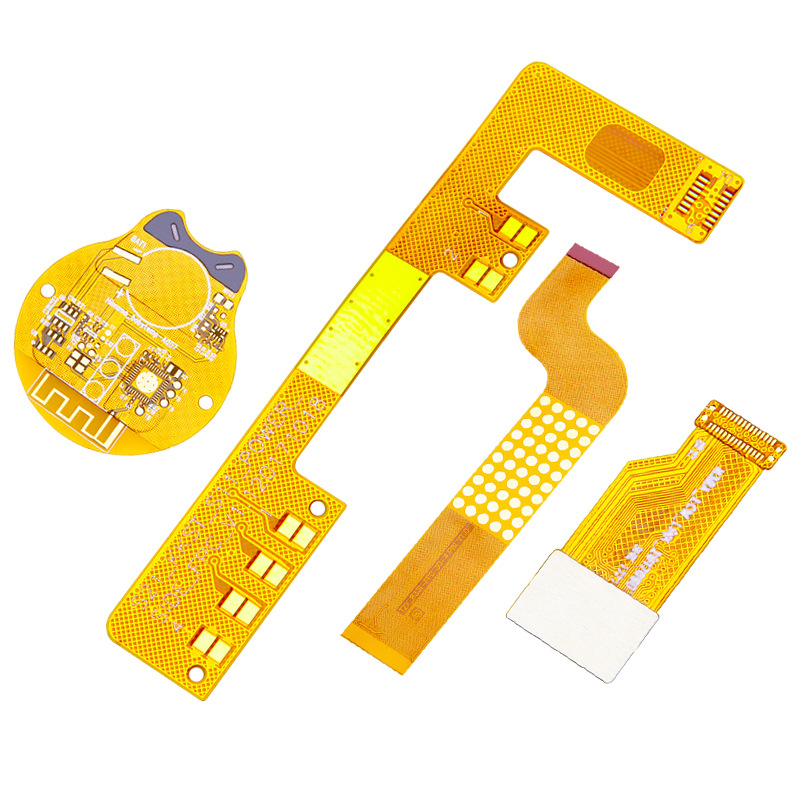
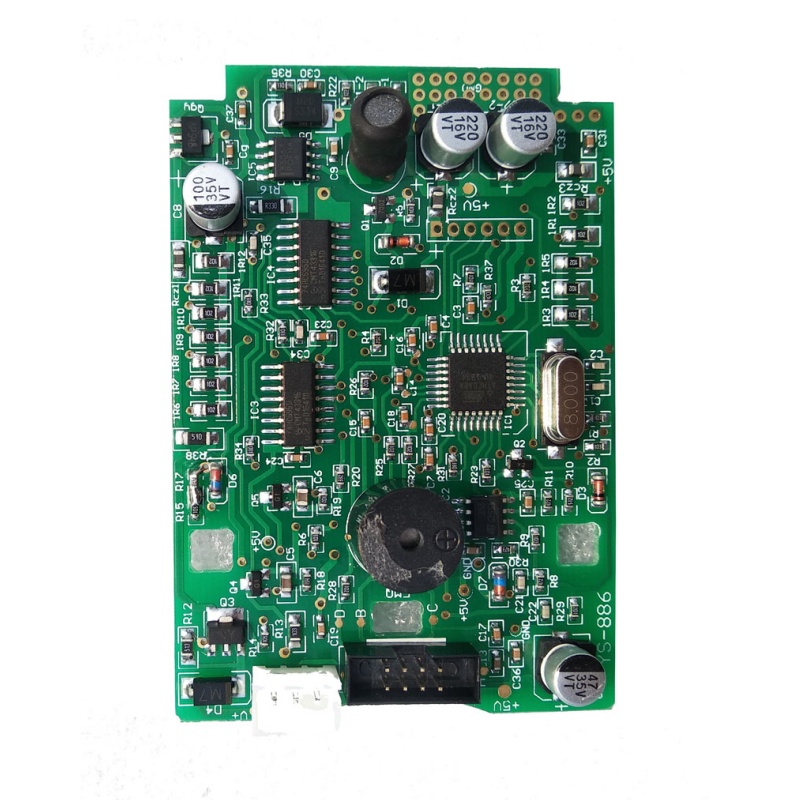
From micro-footprint FPC tactile interfaces to complete SMT board assembly and sensor sub-modules, explore our factory-direct hardware lines manufactured for demanding deployment environments.
Engineering Technical Whitepaper
High-Integrity Membrane Switch Engineering for the Galway Industrial Ecosystem
County Galway, anchored by the Ballybrit, Parkmore, and Mervue business parks, represents one of Europe's premier hubs for medical device technology, advanced instrumentation, marine research, and precision industrial engineering. Developing Human-Machine Interfaces (HMIs) for OEMs located along Ireland's western seaboard requires strict adherence to operating parameters that diverge sharply from generic consumer electronics. Membrane switches deployed in this market must routinely survive aggressive hospital sterilization chemistries, cyclic marine Atlantic condensation, continuous factory cleanroom washdowns, and intensive mechanical duty cycles exceeding several million actuations.
As an end-to-end electronics manufacturing partner with integrated PCB fabrication, turnkey SMT assembly, flexible printed circuit (FPC) production, and membrane switch lines, Shenzhen VUKO Electronics Co., Ltd. bridges the gap between rapid design prototyping and rigorous production repeatability. By maintaining component sourcing, substrate etching, screen printing, and mechanical die-cutting within a single ISO 9001 certified ecosystem, we guarantee Galway design engineers predictable signal timing, hermetic IP67/IP68 boundary sealing, and UL 94V-0 compliant material traceabilities.
Direct Design Takeaway: In high-frequency disinfection environments common to Galway's MedTech cluster, standard polycarbonate overlays suffer from environmental stress cracking (ESC) within months of deployment. Specifying biaxially oriented textured polyester (Autotype MacDermid Autotex XE or fine-grain PET) paired with medical-grade 3M 200MP / 467MP acrylic adhesives eliminates micro-fissuring and edge delamination under isopropyl alcohol (IPA), bleach, and quaternary ammonium wiping regimes.
Technical Architecture: Membrane Switch Substrate Matrix
| Architecture Metric | Silver Conductive Screen-Printed PET | Polyimide (PI) Flexible Printed Circuit (FPC) | Rigid FR4 Backed Membrane Panel |
|---|---|---|---|
| Nominal Trace Resistance | < 1.0 Ω/cm (silver paste) | < 0.05 Ω/cm (electro-deposited copper) | < 0.01 Ω/cm (1oz/2oz copper foil) |
| Interconnect Pitch Capability | 1.27 mm to 2.54 mm minimum pitch | Fine pitch down to 0.5 mm (FPC ZIF compatible) | Ultra-dense SMT pin headers, board-to-board |
| Component Density | Surface conductive epoxy bonding for LEDs | Standard lead-free reflow soldering for passives & ICs | Full complex mixed SMT + DIP, micro-controllers, BGA |
| Moisture & Ingress Sealing | Perimeter gasket adhesive sealing up to IP65 | Continuous polyimide coverlay; sealed up to IP67/IP68 | Hermetic faceplate sealing with integrated mechanical housing |
| Actuation Life Expectancy | Up to 1,000,000 cycles (polyester or metal dome) | Over 5,000,000 cycles (high-fatigue stainless domes) | Over 5,000,000 cycles (rigid non-deflecting ground plane) |
| Optimal Galway Application | Diagnostic monitoring panels, lab controllers, dispensers | Sterilizable surgical consoles, endoscopic monitors | Heavy industrial processing, marine navigation consoles |
Contextual Deployment
Mission-Critical Applications Across Galway's Industries
Engineered to meet the stringent mechanical, environmental, and electro-optical performance profiles mandated by research laboratories, medical plants, and marine infrastructure along the Wild Atlantic Way.
Surgical & Class II/III Medical Devices
Galway produces roughly one-third of the world’s medical stents and critical cardiovascular devices. Our FPC-backed tactile membrane switches integrate flush antimicrobial polyester surfaces, blind debossed guidance rings, and sealed rear gaskets capable of withstanding gamma sterilization, autoclaving vapors, and high-strength hospital disinfectant fluids without graphic decay or silver migration.
Diagnostic Bio-Instrumentation
In analytical flow cytometry and automated assay incubation systems operating in Galway cleanroom laboratories, electro-static discharge (ESD) can destroy delicate sensor readings. We implement solid copper-mesh or printed carbon-grid EMI/RFI shields directly beneath the graphic overlay, shunting discharges up to 15kV safely away from sensitive analog-to-digital controllers.
Marine Electronics & Aquaculture Sensors
Deployments around Galway Bay, the Shannon-Shannon Estuary, and offshore aquaculture cages face extreme coastal salinity and relentless humidity. Our marine-grade tactile interfaces feature IP67 silicone perimeter seals, hydrophobic breathable vent membranes to equilibrate barometric pressure swings, and UV-stabilized anti-glare window overlays legible under direct sunlight.
Precision Automation & Process Machinery
High-throughput automated tooling and pharmaceutical packaging facilities in Ballybrit require robust operator pendants. We integrate nickel-plated stainless steel snap domes providing crisp tactile feedback (actuation forces ranging from 280g to 450g), assuring unmistakable switch registration even when technicians wear thick protective nitrile or cleanroom gloves.
Strategic Foresight
Technological Convergence: Trends Shaping Galway's HMI Procurement
The manufacturing landscape in the West of Ireland is advancing rapidly from passive electromechanical switches toward intelligent, interactive edge-sensing control consoles. Medical design and manufacturing (MD&M) procurement leads across County Galway are currently navigating four structural industry transitions:
Transition from PET to Copper FPC Backers
While traditional screen-printed silver paste on PET suffices for standard consumer keypads, medical instrumentation OEMs are transitioning to polyimide flex circuits. FPC backers eliminate silver migration failure risks under sustained electric potential and high ambient West of Ireland relative humidity, allowing micro-SMD LEDs and 0.5mm pitch ZIF connectors to be soldered without conductive epoxy vulnerabilities.
Hybrid Capacitive Touch & Tactile Integration
Modern clinical diagnostic equipment increasingly merges multi-point capacitive touch sensing zones with mission-critical physical tactile buttons for emergency stop, reset, or high-reliability actuation. Our engineering team assists Galway R&D departments in tuning capacitive copper sensor layouts through thick acrylic or glass cover lenses while retaining discrete tactile metal dome key clusters.
Backlighting Uniformity: LGF & Optical Waveguides
Ambient lighting variations across surgical theaters and intensive care units require homogeneous key illumination without uneven hotspotting. By implementing ultra-thin (0.125mm to 0.25mm) Light Guide Films (LGF) excited by edge-mounted high-efficiency SMDs, we achieve razor-sharp symbol legibility at minimal current draw, avoiding the electromagnetic interference generated by obsolete electroluminescent (EL) foils.
Manufacturer Advantages
Why Galway Procurement Managers Rely on VUKO Electronics
Combining the cost efficiency and scaling capacity of our high-precision Shenzhen production base with world-class engineering documentation, strict DFM discipline, and rapid door-to-door delivery into Shannon and Dublin logistics corridors.
Alibaba.com Onsite-Verified & ISO 9001
Every fabrication batch conforms to rigid quality control workflows. Our facility is onsite-inspected and verified, with full Trade Assurance order protection. We deliver transparent material traceability, lot serialization, and comprehensive Certificate of Conformance (CoC) reports on all bare boards, membrane keypads, and SMT assemblies.
Pre-Production DFM Review in Under 24h
Avoid costly re-spins and scheduling slippages. Our dedicated engineering desk rigorously audits your Gerber files, BOM component availability, key actuation travel tolerances, tail routing geometries, and dielectric breakdown clearances, returning actionable DFM feedback within 24 business hours.
True One-Stop Ecosystem: From 5-Piece Prototypes to Volume
Rather than managing separate vendors for graphic printing, metal domes, flexible interconnects, multilayer FR4 motherboards, and passive component kitting, VUKO unifies the complete bill of materials. We accommodate pilot trial builds from as low as 5 pieces through to scheduled production batches of hundreds of thousands.
14+
Years International OEM Export
< 24h
Engineering DFM Response
5 Pcs
Low Prototype MOQ Support
100%
Electrical & Optical E-Tested
Direct Sourcing Clarity
Frequently Asked Questions by Galway Hardware Buyers
Clear, unvarnished technical and logistics answers regarding documentation, material ratings, compliance, and transatlantic fulfillment into Ireland.
Which file formats are required to quote a custom membrane switch and PCBA build?
For membrane switch overlays and graphic layers, provide vector artwork in Adobe Illustrator (.AI), vector PDF, or CorelDraw, with specified Pantone/RAL color codes and window transparencies. For the underlying circuitry, provide RS-274X Gerber files and drill files. For complete turnkey PCBA builds, supply an Excel-formatted Bill of Materials (BOM) including exact Manufacturer Part Numbers (MPNs), reference designators, and an XY centroid (pick-and-place) file.
How do you guarantee IP67/IP68 ingress protection against hospital disinfectants?
We employ continuous perimeter closed-cell acrylic foam adhesive gaskets (such as 3M 467MP, 468MP, or VHB systems) combined with autotex biaxially-oriented textured polyester. The adhesive layer extends unbroken outside the circuit trace boundary, preventing creeping fluid ingress when subjected to aggressive hospital clean-downs utilizing sodium hypochlorite (bleach), glutaraldehyde, or 70% IPA solutions.
What is the typical prototype and production turnaround time to Galway, Ireland?
Rapid prototype membrane switch samples and bare PCB runs are typically fabricated in 5 to 8 working days following engineering DFM sign-off. Turnkey PCBA builds require 10 to 18 working days depending on component procurement lead times. Express air courier shipments via DHL Express, FedEx Priority, or UPS reach Galway, Shannon, or Dublin freight hubs within 3 to 5 business days, backed by Trade Assurance customs clearing documentation.
Are your manufacturing materials fully compliant with EU RoHS and REACH regulations?
Yes. All laminates, solders, conductive pastes, graphic films, adhesives, and surface platings strictly comply with EU RoHS Directive 2011/65/EU and REACH (EC 1907/2006). All FR4 laminates meet UL 94V-0 flammability ratings. We provide signed declaration certificates and laboratory testing documentation for your internal Device Master Record (DMR) or regulatory audit dossier.
Can you provide custom tactile actuation feel options for glove-wearing operators?
Absolutely. We stock a comprehensive range of stainless steel and nickel-plated tactile domes in four-leg, round, and oblong configurations from 6mm to 20mm diameters, with actuation forces ranging from 180g (light clinical touch) up to 500g (heavy industrial snap feedback). Custom embossed graphic keys (rim embossing, pillow embossing, or dome embossing) ensure positive tactile indexing for operators wearing surgical or industrial gloves.
How do you handle end-of-line quality verification prior to transatlantic dispatch?
Every single membrane switch undergoes automated electrical continuity, short-circuit, and contact resistance testing via dedicated test fixtures. Actuation force curves and click ratios are verified using calibrated force gauges. For assembled PCBA units, we conduct Automated Optical Inspection (AOI), X-ray inspection for fine-pitch BGAs/QFNs, and custom functional testing (FCT) using client-supplied firmware and test jigs.