Thermal Core
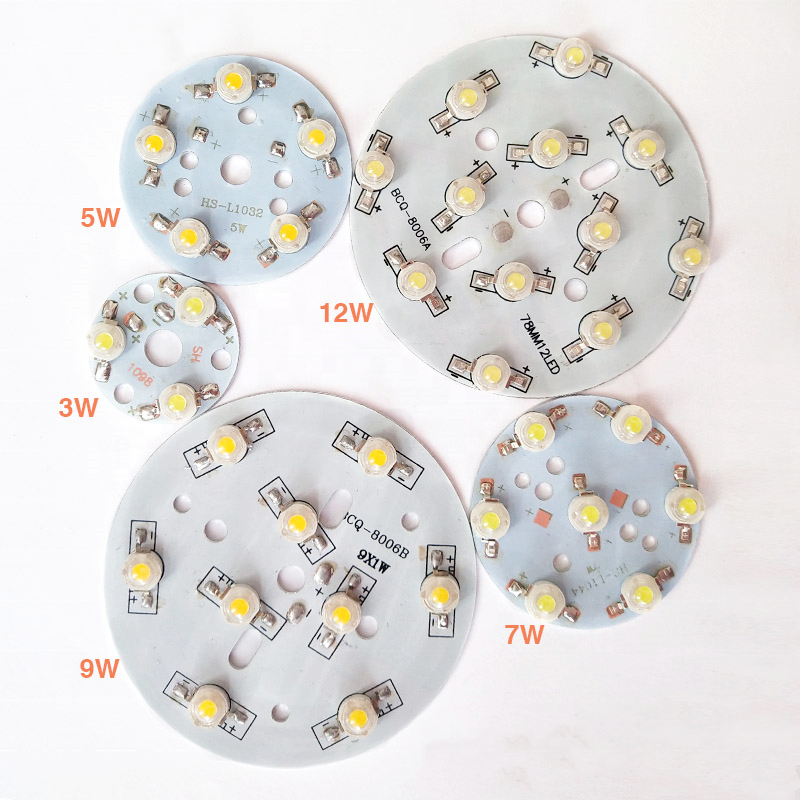
Custom Circular Aluminum LED Bulb Lighting PCB
0.5oz to 3oz Copper weight with HASL/OSP finish, designed for extreme heat dissipation in sealed marine LED fixtures.
Get a QuoteSeamlessly integrate CE-compliant input interfaces, high-grade flexible PCBs, and robust component assemblies matched to complex industrial operating criteria.
0.5oz to 3oz Copper weight with HASL/OSP finish, designed for extreme heat dissipation in sealed marine LED fixtures.
Get a Quote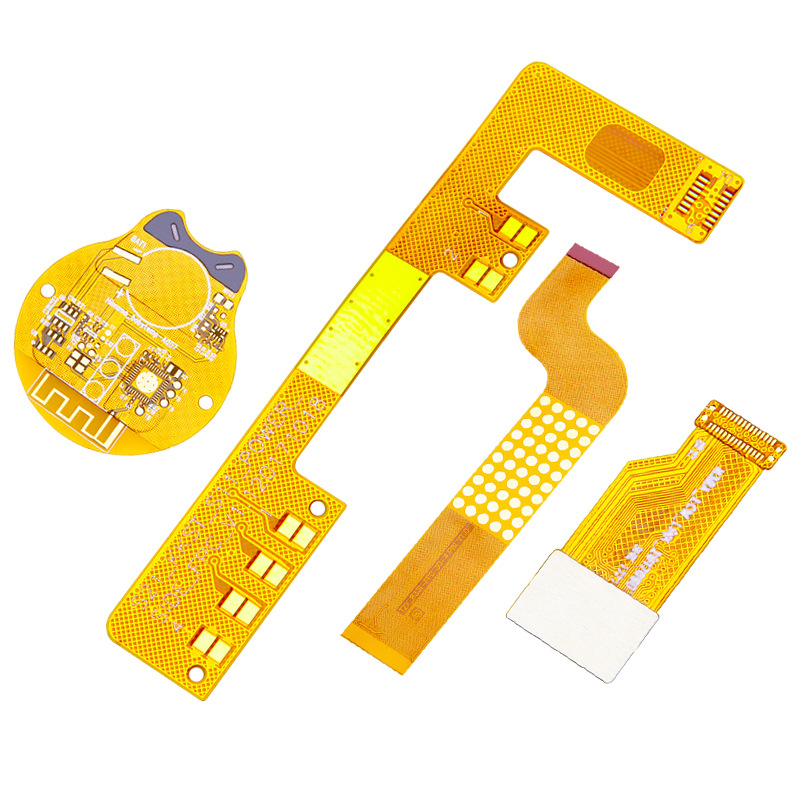
Polyimide (PI) substrate flex circuit engineered for extreme environmental tolerance in medical equipment & industrial actuators.
Get a Quote
Single/Double-sided quick-turn flexible circuits ideal for engineering R&D validations and proof-of-concept testing.
Get a Quote
OEM precision fabrication with 1oz copper, tight trace impedance control, and UL 94V-0 certified laminate integrity.
Get a Quote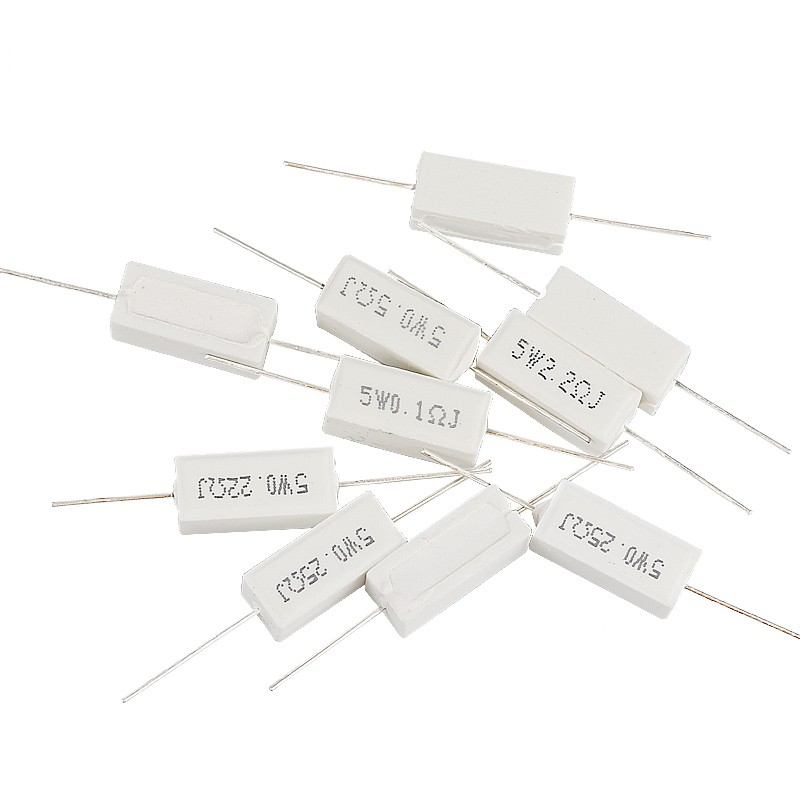
Axial lead power damping component built for high surge current resistance and long-term stability in harsh power grids.
Get a Quote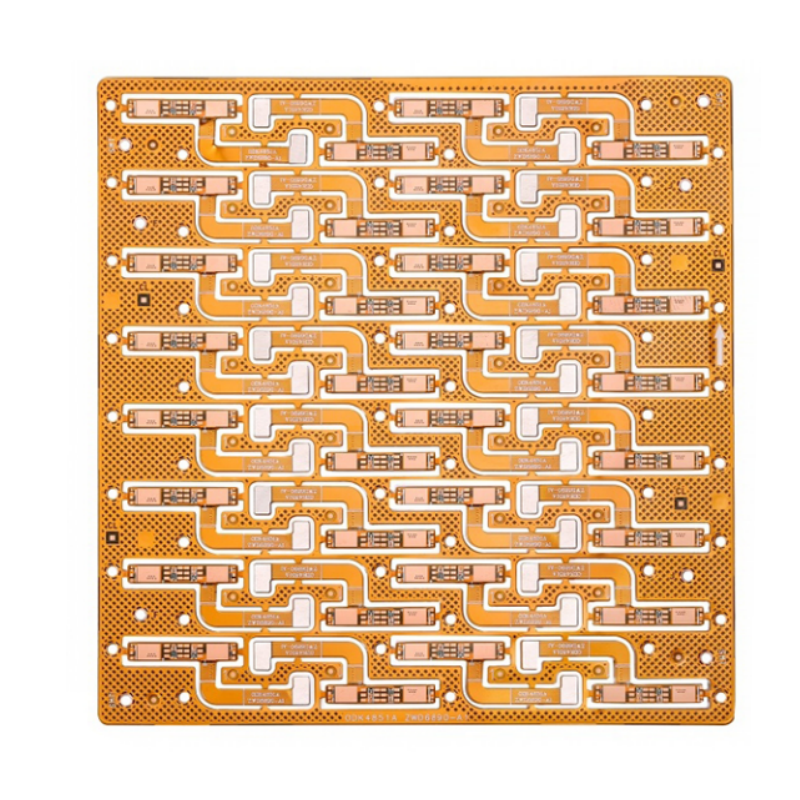
Integrated FPC and component mounting, automated optical inspection, and connector welding under ISO 9001 protocols.
Get a Quote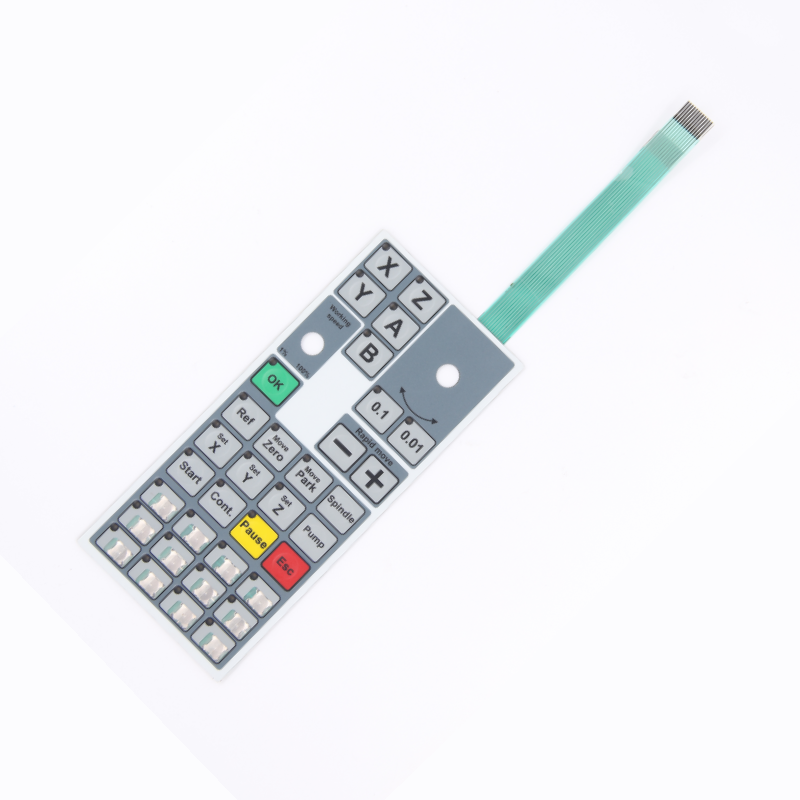
Silver-printed circuit layer with stainless steel tactile snap-domes, IP65 perimeter barrier, and chemical-resistant PET overlay.
Get a Quote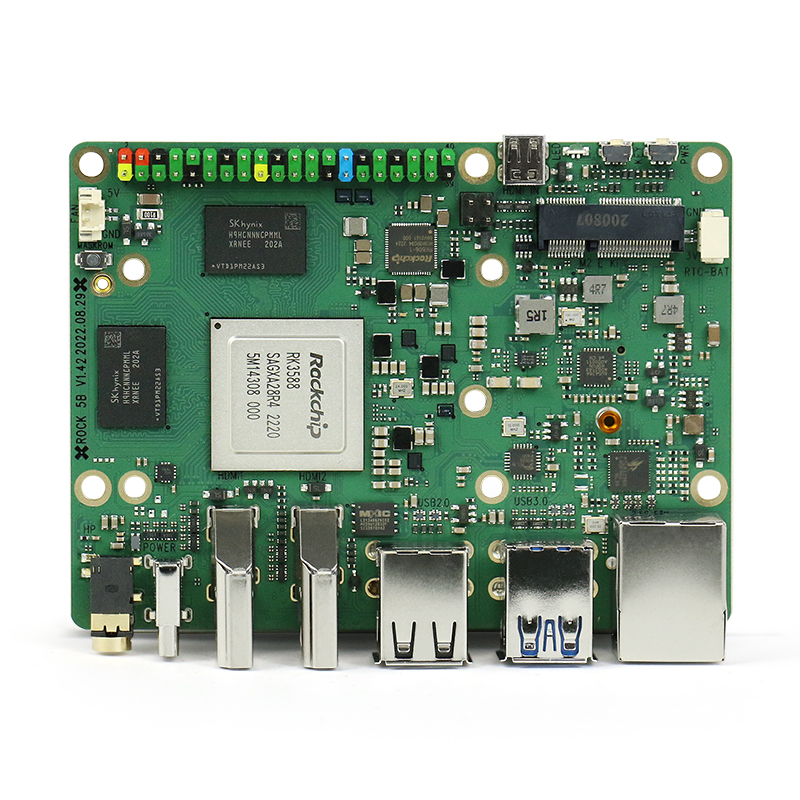
High-performance edge computing platform equipped with 8G/16G LPDDR4X, 8K video pipeline, and broad industrial peripheral connectivity.
Get a QuoteOvercoming the twin adversaries of airborne marine salinity and non-condensing relative humidity through materials science.
Operating electrical hardware in Koror and across the Republic of Palau requires overcoming unique microclimatic stresses rarely addressed by off-the-shelf commercial electronics. With ambient humidity routinely exceeding 85%, persistent maritime salt-fog aerosol dispersion, and heavy UV exposure, generic push-buttons and capacitive-only glass touchscreens suffer from high failure rates. In humid island settings, mechanical switch mechanisms allow saline particulates to infiltrate contact gaps, creating catastrophic electrochemical migration, tin whiskering, and parasitic leakage currents.
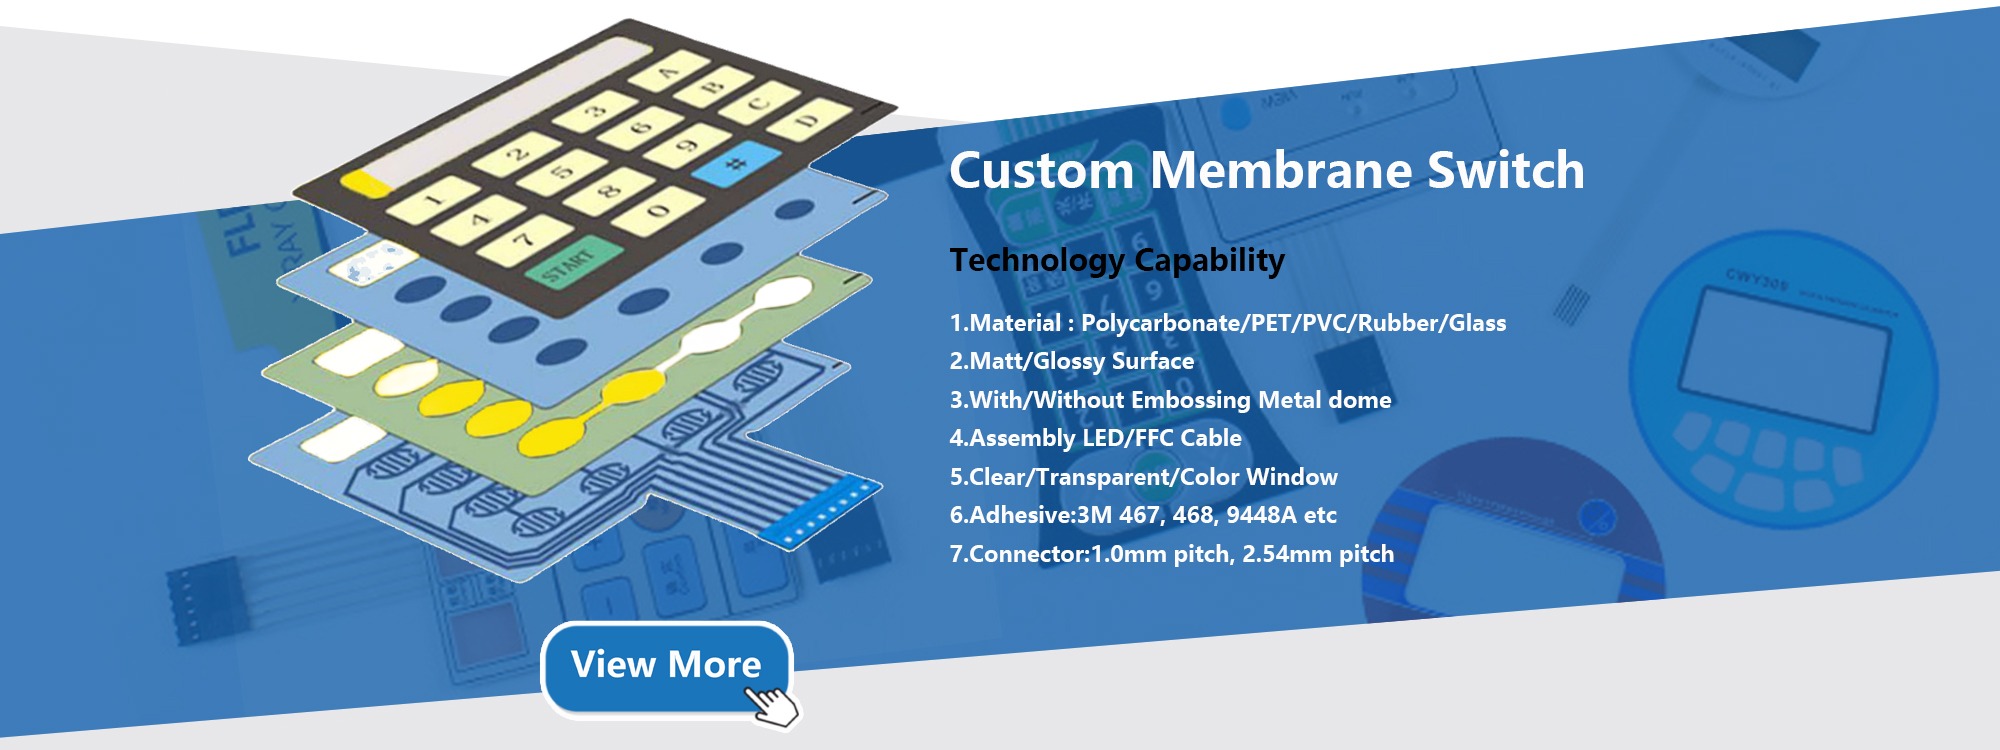
To address these operational hurdles, CE Certified Membrane Keypads engineered by Shenzhen VUKO Electronics Co., Ltd. leverage multi-layered hermetically sealed architectures. By using specialized optical-grade Autotype Autotex XE polyester (PET) graphic layers combined with 3M 467MP/468MP high-performance acrylic adhesives, our panels isolate internal conductor tracks and metal click domes from ambient humidity and salt ions. The switch cavity remains isolated from the external environment, delivering an impermeable barrier that withstands continuous IP65 through IP67 ingress testing conditions.
Continuous closed-loop adhesive perimeters bond graphic films seamlessly to support backplates, stopping liquid capillary creep and condensing vapor from reaching conductive silver ink matrices.
Standard Polycarbonate (PC) yellows and becomes brittle under equatorial UV indices. Our selective application of textured PET maintains polymer chain stability without fading, micro-cracking, or delamination.
Microscopic electrolysis occurs when silver traces carry DC potentials in humid salt air. VUKO screen-prints a conductive carbon shielding overcoat across all contact pads, preventing dendritic short circuits.
From deep-sea diving compressors to solar mini-grid controllers, explore how custom membrane panels maintain operational continuity.
Koror serves as the principal economic hub and gateway for Palau's world-renowned marine tourism and conservation sectors. Vessels navigating the Rock Islands Southern Lagoon operate high-output Nitrox blending consoles, water desalinators, and outboard telemetry displays that encounter continuous seawater splash and marine diesel oil vapours.
Our customized membrane switch assemblies feature stainless steel four-leg tactile snap-domes (280g to 400g actuation force). This provides definitive tactile feedback to boat captains and technical divers wearing thick neoprene gloves, preventing accidental multiple keystrokes during turbulent open-water transit.
Palau's aggressive transition toward clean energy has driven wide installation of commercial solar photovoltaic invertors, central hybrid Battery Energy Storage Systems (BESS), and reverse osmosis municipal water filtration centers across Koror and Airai. Electronic controls placed outdoors undergo intense solar heating cycles followed by torrential tropical precipitation.
Traditional rubber elastomeric interfaces swell and deteriorate when exposed to ambient ozone and airborne chemicals. VUKO manufactures custom membrane switches with integrated FPC (Flexible Printed Circuit) tails plated in immersion gold (ENIG). Unlike standard silver paste printed ribbon tails that degrade in moist environments, our FPC tails eliminate ribbon oxidation at the controller mating connector.
Diagnostic monitors and autoclave sterilization units operated within the Belau National Hospital system demand user interfaces that tolerate daily cleaning with hospital-grade disinfectants, including isopropyl alcohol, bleach, and quaternary ammonium compounds.
Our CE-certified membrane panels provide smooth, flat surface contours without seams, raised screws, or recessed crevices. This stops pathogenic micro-organisms and debris from accumulating, allowing thorough wipe-down sterilization without fluid seeping into underlying PCB control modules.
Comparative benchmarks for high-humidity, marine-tolerant human-machine interfaces.
| Performance Characteristic | Commercial Grade Standard | VUKO Industrial Marine Grade (Koror Spec) | Testing & Compliance Protocols |
|---|---|---|---|
| Overlay Base Material | Standard Monolithic PVC / Polycarbonate | Autotype Autotex XE Textured Polyester (PET) | ASTM G154 Accelerated UV Weathering |
| Operating Temperature | -10°C to +50°C | -35°C to +85°C Continuous Rating | IEC 60068-2-1 / IEC 60068-2-2 |
| Relative Humidity Resistance | Up to 75% Non-Condensing | 98% Relative Humidity @ 40°C (Damp Heat) | MIL-STD-202G, Method 103B Condition B |
| Contact Circuit Layer | Silver Flake Ink Screenprint | Silver Ink with Carbon Shield or Polyimide FPC | Electrochemical Migration Test @ 50V DC |
| Tactile Actuation Life (MTBF) | Approx. 100,000 cycles | Over 1,000,000 actuations (Stainless Domes) | Automated Robotic Finger Actuation Test |
| Salt Spray Corrosion Resistance | 24 Hours Standard Test | 96 to 120 Hours Continuous Saline Fog | ASTM B117 / ISO 9227 Neutral Salt Spray |
| Surface Chemical Resilience | Damaged by Acetone & Solvents | Resistant to IPA, Hydrocarbons, Marine Fuels | DIN 42 115 Chemical Reagent Wipe Down |
| EMC / ESD Protection Shield | Optional or Absent | Integrated Aluminum Foil or Carbon Grid Shield | EN 61000-4-2 Air Discharge 15kV, Contact 8kV |
Every membrane switch manufactured for export to Pacific regional enterprises follows stringent production protocols.
Engineering files (Gerber RS-274X, CAD DXF/DWG, artwork PDF) are reviewed for switch trace widths, spacing clearances, and venting cutouts to prevent air-cushion lock.
Text, color fills, and transparent display windows are printed in Class 10,000 cleanrooms using sub-micron optical alignment jigs and UV-curable dielectric coatings.
Gold or nickel-plated stainless steel metal snap domes are pick-and-placed onto circuit traces with automated machinery, ensuring consistent actuation centers.
Every completed membrane switch undergoes automated electrical continuity verification, loop resistance mapping, contact bounce checks, and insulation resistance audits.
Leveraging Shenzhen's comprehensive electronics supply chain to supply reliable components across Oceania.
Eliminate multiple suppliers. We fabricate bare rigid PCBs, etch high-density flex circuits, source authentic BOM passives, build membrane switch overlays, and complete SMT/DIP assemblies under one roof.
We welcome projects starting from just 5 to 10 prototype units for initial field validation in Koror before scaling smoothly to volume production, preventing upfront capital lockup.
Our operations follow ISO 9001 certified quality control, RoHS lead-free environmental standards, UL 94V-0 flammability ratings, and CE directives, ensuring smooth customs processing and operation.
Key technical and logistics inquiries answered for procurement engineers across Palau and the Western Pacific.
Connect with our technical application team today. Upload your CAD drawings, Gerber files, or interface sketches to receive an expert DFM review and factory-direct quotation within 24 hours.