Precision HMI & Electronics Solutions for Liverpool Engineering
Explore our core export lines: customized FPC and membrane interfaces, bare circuit boards, SMT assemblies, and critical hardware modules certified for rigorous commercial deployment.
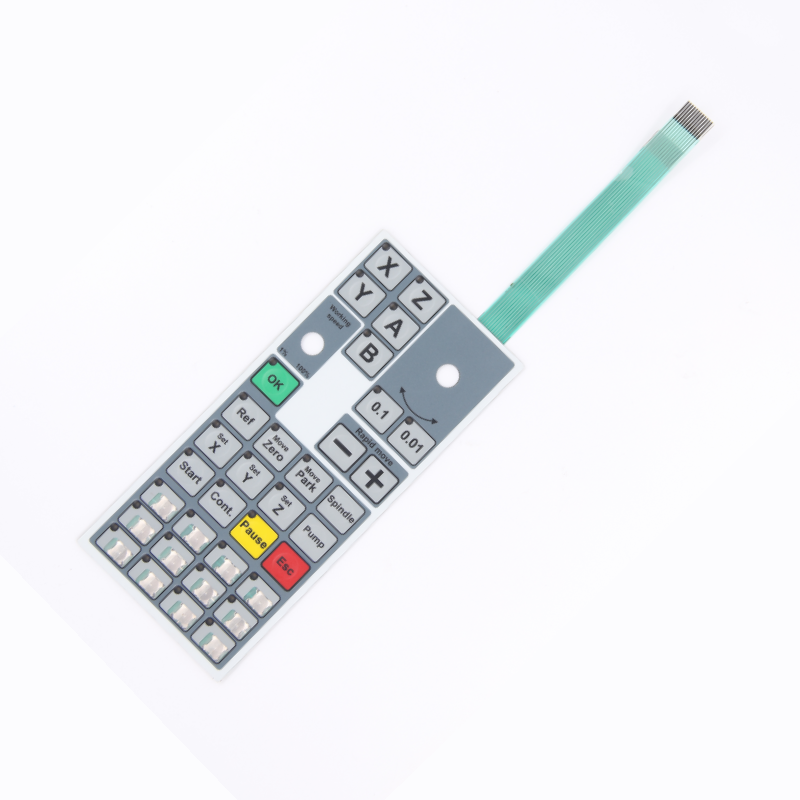
Custom Membrane Switch, PET PC Flexible Keypad, Silver Ink Circuit, FPC FFC Tail
Send an Inquiry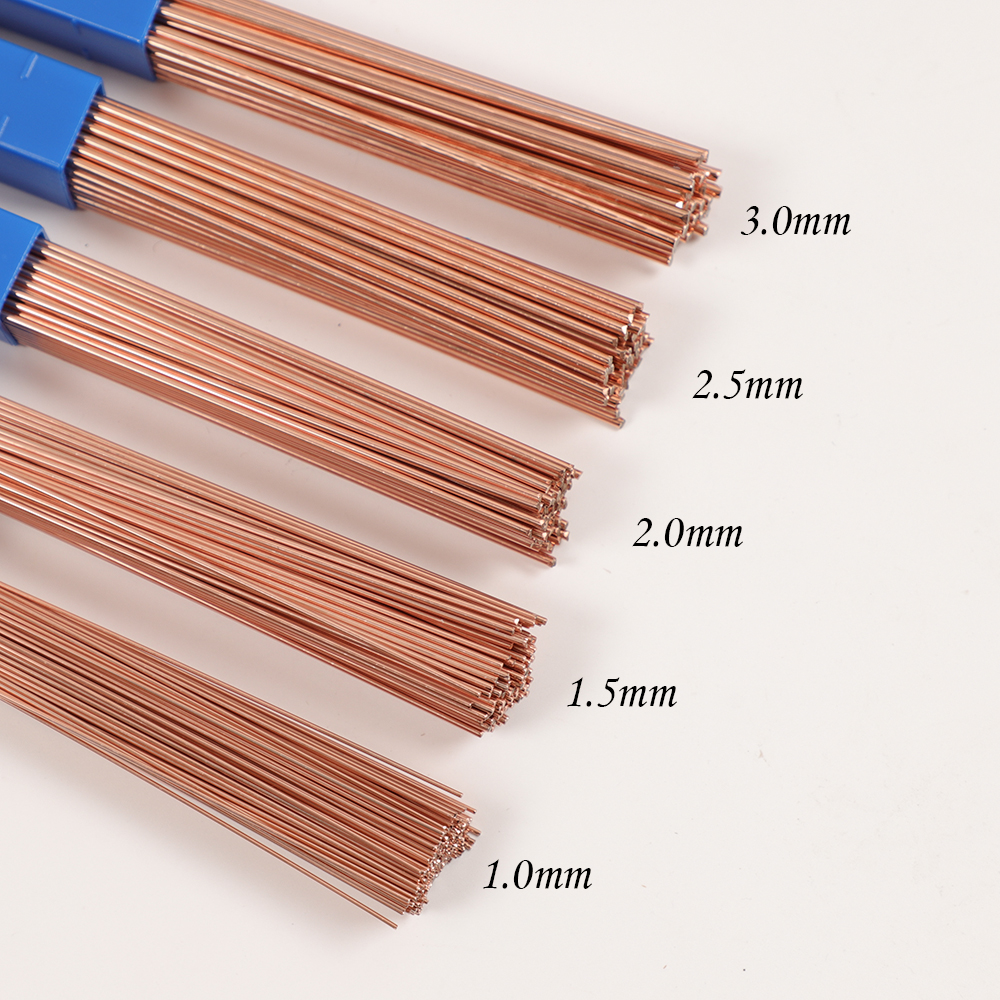
Brass Welding Rod Phosphorus Copper Soldering Electrode 50cm 1mm-3mm
Send an Inquiry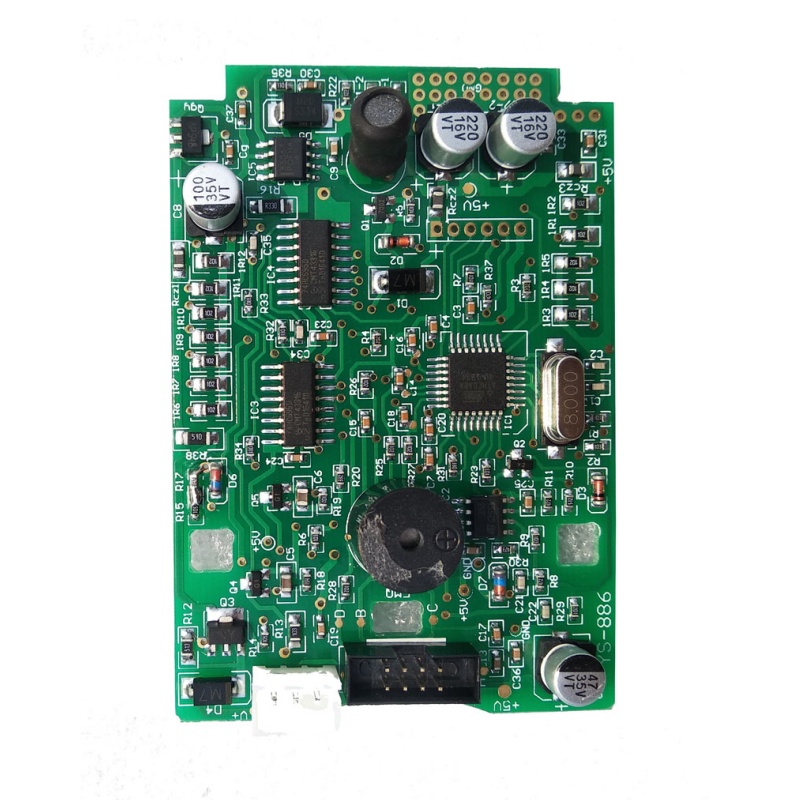
Custom Smart Device PCBA Assembly OEM PCB Board SMT Assembly for IoT Sensor
Send an Inquiry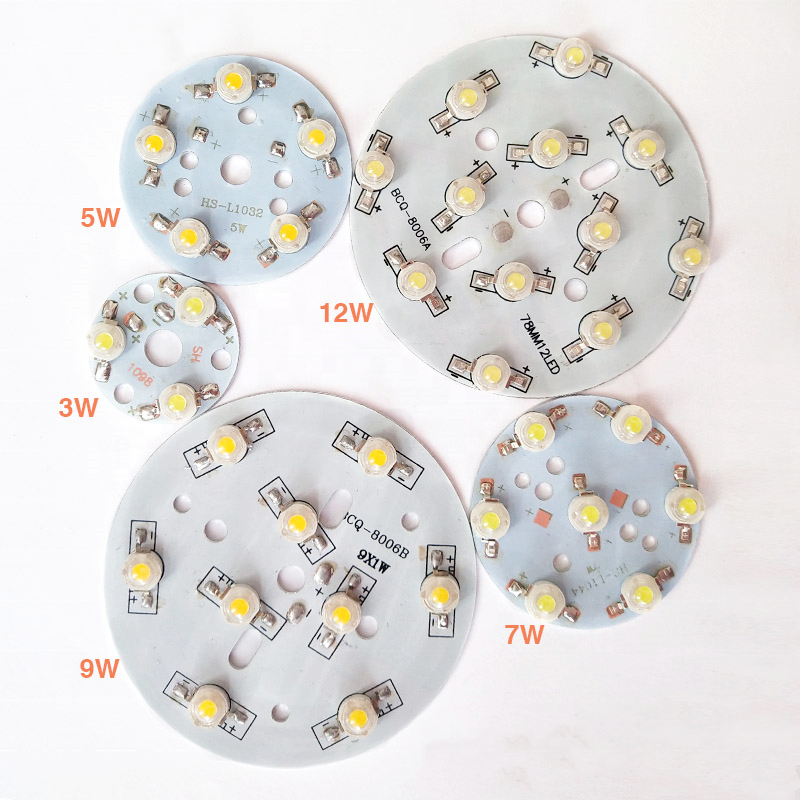
Custom Size Aluminum LED PCB PCBA Circular Bulb Lighting Board 0.5oz-3oz Copper
Send an Inquiry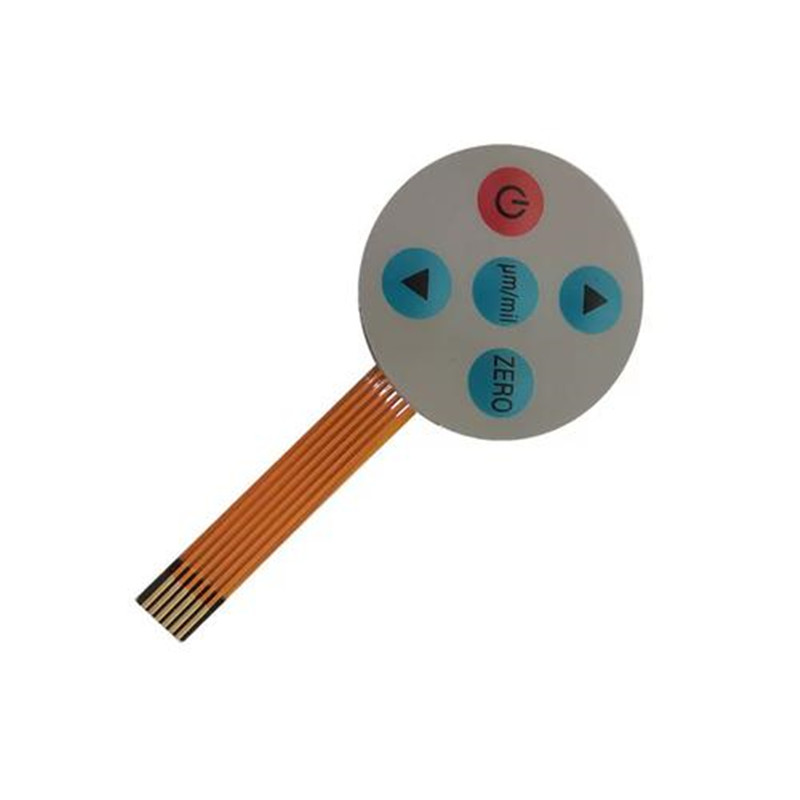
FPC Tail Membrane Switch Keypad, Custom Flexible Circuit Panel, Silk Screen
Send an Inquiry
OEM PCBA Service One Stop PCB Assembly SMT DIP Soldering Circuit Board
Send an Inquiry
Smart Electronics Custom Multilayer PCB Board OEM Service FR4 Base Material
Send an Inquiry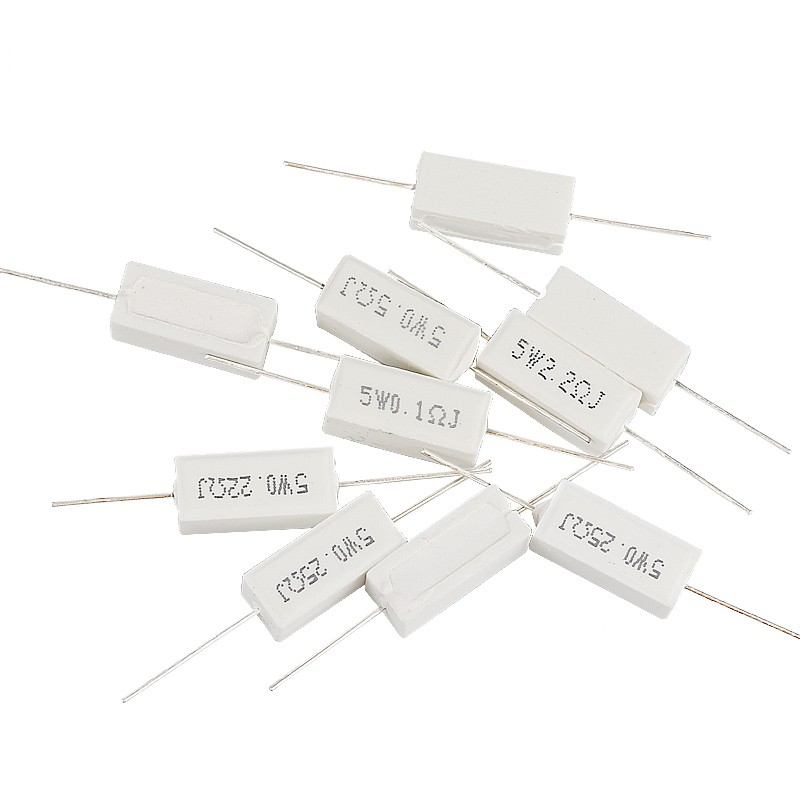
5W 0.22 Ohm Ceramic Cement Resistor Wirewound Axial Lead Electronic Component
Send an InquiryWhy Polyimide FPC Circuits Outperform Silver Paste in Harsh Environments
Understanding the critical electro-mechanical distinctions between screen-printed silver ink tracks and etched copper polyimide (FPC) flexible circuits for United Kingdom OEMs.
Zero Electrochemical Silver Migration
Traditional screen-printed membrane switches rely on flake silver paste suspended in a polymer matrix. In maritime environments with persistent humidity, moisture along with low continuous DC voltages induces electrolytic silver dendritic migration, causing short-circuit failures across closely-spaced traces.
- Eliminates conductive path crystallization
- Robust dielectric barrier via polyimide coverlays
- Withstands 95% relative humidity long-term cycling
High-Density Component Integration
Polyimide FPC substructures utilize standard photolithographic etching, enabling line widths and track spacing down to 0.1mm (4 mil). This enables direct SMT mounting of miniature LEDs, phototransistors, and active controllers straight onto the flex tail.
- Fine-pitch connector pitch (down to 0.5mm ZIF)
- Soldered SMT components using lead-free reflow
- Embedded active driver ICs directly on keypads
Dynamic Mechanical Flex Endurance
Where keypads interface with moving consoles or hinged enclosures, copper foils laminated between polyimide sheets provide dynamic bend cycles exceeding 200,000 movements without resistance spikes, vastly outpacing brittle printed silver tracks.
- Consistent loop resistance (< 1 Ohm per run)
- Customized FR4 or stainless steel stiffener backings
- High peel-strength lamination with 3M 467/468 adhesives
| Engineering Parameter | Silver Printed PET Membrane Switch | Polyimide (PI) Copper FPC Membrane Switch | Advantage for Liverpool Projects |
|---|---|---|---|
| Trace Resistance | 10 Ω to 100 Ω (depending on length) | < 0.5 Ω to 1.5 Ω (Pure etched copper) | Enables fast logic signals, low noise, and clean ground planes. |
| Marine / Humidity Resilience | Vulnerable to silver dendritic growth over 85% RH | Immune (solid rolled/annealed copper + PI barrier) | Critical for Liverpool docklands, Mersey port logistics, & marine vessels. |
| SMT Soldering Reliability | Requires conductive epoxy adhesive (curing risk) | True reflow soldering with lead-free alloy | Prevents shear failure under heavy mechanical vibration. |
| Connector Pitch Tolerance | Standard 1.0mm to 2.54mm pitch | Fine pitch 0.5mm ZIF locking connectors | Compact controller footprint in constrained industrial enclosures. |
| Expected Operating Life | 500,000 to 1,000,000 cycles | > 3,000,000 tactile switch cycles | Guarantees low field maintenance across automated machinery. |
Localized Applications Across the Liverpool & North West Corridor
Liverpool is undergoing an industrial renaissance spanning maritime logistics at the Port of Liverpool, pharmaceutical research in the Knowledge Quarter, automotive manufacturing around Halewood, and commercial energy generation along the Mersey basin.
Port of Liverpool & Maritime Equipment
Operating near open docklands requires salt-mist protection, wide operating temperature resilience (-30°C to +85°C), and ingress resistance up to IP67. Our FPC membrane keypads serve container crane wireless remotes, dockside weighing scales, vessel navigational consoles, and automated gate telemetry stations.
- Textured Autotex PET overlays resisting UV and saline degradation
- Gold-plated tactile domes ensuring contact certainty through thick work gloves
- EMI/RFI aluminum shielding layers stopping radio interference
Biopharma & Knowledge Quarter Laboratories
Merseyside's medical, vaccine manufacturing, and life sciences sectors demand interface panels capable of undergoing daily sanitization with aggressive agents including isopropyl alcohol, hydrogen peroxide, and sodium hypochlorite without graphic fading or seal delamination.
- Antimicrobial textured hard-coat films (Microban compatible)
- Completely flat, hermetically sealed wipe-down surfaces
- Integrated clear display filter windows with anti-glare treatment
Halewood Automotive & Advanced Manufacturing
From automated electric vehicle supply chain facilities to manufacturing plant floor robotics in Knowsley and Speke, high mechanical shock, solvent splashes, and heavy cycle rates necessitate robust tactile feel and high electrical repeatability.
- Automotive-grade adhesive backings (3M 300LSE for low surface energy plastics)
- Custom actuation forces from 250g to 450g for positive operator feedback
- Integrated bi-color LED indicators for immediate equipment state validation
Direct China Factory Pricing • Rapid Delivery to Liverpool
By eliminating UK intermediary brokers, Liverpool original equipment manufacturers achieve between 35% and 55% procurement cost reductions while working directly with our Shenzhen engineering staff. We ensure rapid DDP sea shipments into the Port of Liverpool or express 3-5 day air couriers direct to John Lennon Airport customs facilities.
Next-Generation HMI Trends Driving UK Industrial Procurement
How technological integration in Industry 4.0 and sustainable manufacturing is shifting user interface specifications throughout the United Kingdom.
Capacitive Sensing Combined with Tactile Domes
Engineers are increasingly merging touch-free or gesture capacitive sliders with definitive tactile emergency-stop and confirmation domes on one consolidated FPC substrate. This hybrid approach ensures seamless cleaning while maintaining operator safety in industrial controls.
Ultra-Thin Profile & Weight Reduction
Traditional rigid sub-panels and bulky mechanical switches are being replaced by ultra-flat (less than 1.2mm total thickness) membrane structures. This decreases transport weight, eases ergonomic hand-held casing design, and accelerates final assembly times on UK factory floors.
Full Turnkey "Panel-to-Board" Consolidation
UK purchasing departments are transitioning away from buying keypads, bare boards, and wire harnesses separately. Sourcing the complete assembly—FPC membrane switch connected to an assembled PCBA mainboard—minimizes supplier liability and guarantees 100% functional match.
Frequently Asked Questions by UK Engineering & Sourcing Teams
Clear, direct answers regarding custom tooling, UK import tariffs, prototyping speed, and quality inspection protocols.
We require your graphic artwork files (vector formats: Adobe Illustrator .AI, CorelDRAW .CDR, or vector .PDF) specifying Pantone or RAL color codes, alongside the mechanical/circuit schematic (AutoCAD .DXF, .DWG, or Gerber RS-274X files) denoting circuit pinout, dome locations, embossed key profiles, and tail dimensions.
We provide flexible incoterms including EXW, FOB Shenzhen, CIF, and full DDP (Delivered Duty Paid) to your Liverpool warehouse. Under DDP, we manage UK Customs clearance, payment of import duty, and declaration through HMRC, meaning no customs paperwork complications for your local team.
Unlike rigid manufacturers requiring thousands of units, our MOQ starts from just 5 to 10 prototype pieces. Prototype lead times typically run 7 to 10 working days following engineering drawing sign-off, with mass production runs completing in 15 to 20 working days.
Yes. We specify genuine marine-grade Autotex or Toray biaxially oriented PET film with perimeter sealing using 3M high-performance acrylic adhesives (3M 200MP / 300LSE). Copper FPC traces completely avoid electrolytic corrosion caused by coastal humidity and saline air intrusion.
Every material used—from substrate laminates, conductive copper, printing inks, solder alloys, to surface finish treatments—complies fully with EU RoHS, REACH, and UK equivalent regulations. We provide certificates of conformity (CoC) and complete material declarations with every production batch.
Every single keypad is 100% electrically tested for circuit continuity, contact loop resistance, and insulation resistance. We also conduct automated optical inspection (AOI) for graphic registration, LED color/intensity validation, and tactile dome actuation force sampling using digital force gauges.
Why Global Buyers Partner with VUKO Electronics
Combining end-to-end electronics manufacturing under one roof with world-class quality systems and customer-centric support.
Alibaba Onsite-Verified
Verified supplier credentials with complete third-party on-site audits, offering full Trade Assurance financial and shipment protection.
Turnkey Vertical Factory
From bare multilayer PCB fabrication and SMT component sourcing to custom FPC and graphic lamination—no outsourced middlemen.
Dedicated Engineering DFM
Our engineers perform detailed Design for Manufacturability reviews on all incoming files within 24 hours to prevent costly production errors.
Low MOQ Prototyping
Custom engineering from 5 pieces to support Liverpool hardware startups, university spinouts, and large OEMs validating new designs.