Integrated Industrial Components & Assembly Systems
Engineered for seamless integration with custom matrix membrane switches, harsh-environment controllers, and industrial control electronics.
Engineering Matrix Membrane Keypads for the South Pacific Environment
A systematic analysis of tactile feedback mechanics, material stability, and hermetic perimeter sealing against marine atmospheric corrosion.
Climatic Degradation Vectors & Material Selection in Guadalcanal Province
Deploying Human-Machine Interfaces (HMI) across Honiara and outer island facilities exposes electromechanical assemblies to unique ambient stressors. With year-round relative humidity frequently exceeding 85%, ambient operating temperatures ranging between 26°C and 34°C, and heavy atmospheric salt concentration carried by trade winds across Iron Bottom Sound, standard commercial electronic keypads suffer rapid degradation. The primary failure mode observed in non-ruggedized membrane keypads is silver migration across conductor pathways, caused by micro-condensation seeping into unsealed matrix traces, alongside premature delamination of low-grade pressure-sensitive adhesives (PSAs).
To eliminate cross-contamination and dendritic crystal growth between the row and column matrix lines, our specialized manufacturing pipeline implements autoclave-grade, bi-axially oriented Polyethylene Terephthalate (PET) and custom Polyimide (PI) carrier films coated with carbon-stabilized, non-migrating conductive silver traces. Combined with 3M 200MP, 300LSE, or VHB structural bonding films applied via cleanroom heated-roller lamination, our matrix membrane keypads achieve a permanent, hermetically sealed IP67 rating that repels moisture ingress, airborne diesel particulates from local power generation, and airborne chloride salt mist.
Chloride-Proof Sealing
Full perimeter hydrophobic venting and gasket-level adhesive cutouts prevent capillary moisture draw under high tropical humidity.
Gold-Plated Metal Domes
Nickel and flash-gold coated stainless steel domes guarantee over 1,000,000 actuations without oxidation-induced contact bounce.
UV & Sun Resistance
Autotex XE anti-glare, UV-stabilized polyester overlays prevent graphic yellowing, brittleness, and graphic peeling under direct solar exposure.
Multiplexing Efficiency: Pin Optimization in Industrial Control Schemes
In modern embedded design, physical I/O pins on programmable logic controllers (PLCs) and microcontrollers (such as STM32, ESP32, and Microchip AVR platforms) represent a premium resource. Direct single-line pushbuttons require one physical input pin per tactile switch plus ground wiring harnesses. For municipal equipment, telemetry logging modules, and remote off-grid solar inverters utilized across Honiara's industrial zones (such as Ranadi Industrial Estate), matrix interconnection architecture minimizes interconnect complexity and failure points.
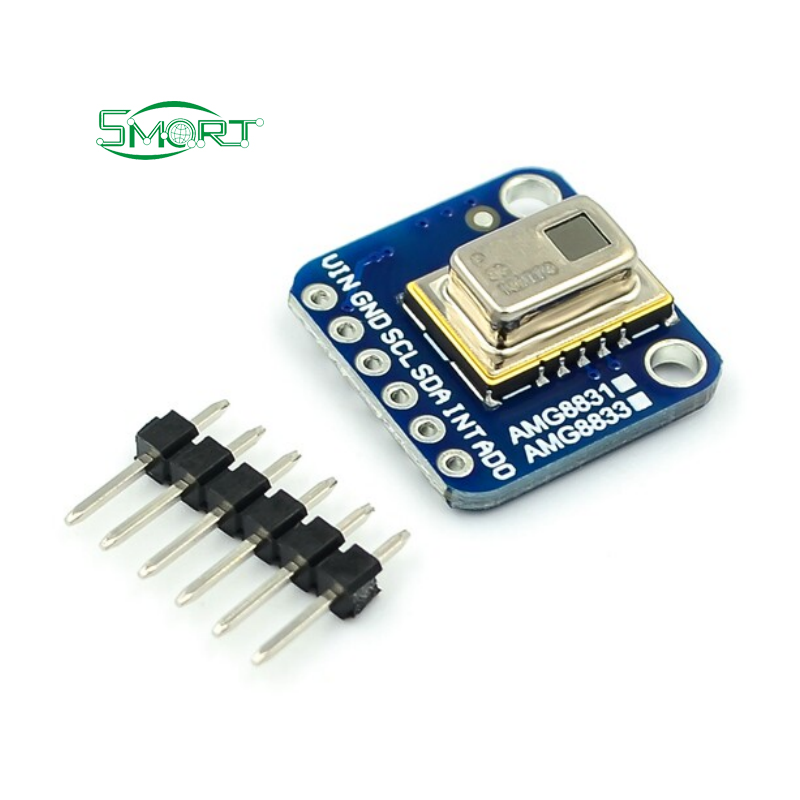
In an $X \times Y$ matrix keypad (e.g., standard 4x4 or 3x4 layout), rows act as dynamic output scan lines while columns serve as input sense lines with pull-up or pull-down resistors. A 16-key matrix demands only 8 microcontroller GPIO pins, effectively liberating board real estate for auxiliary sensors like the GY-AMG8833 thermal array, display interfaces, and communications transceivers. Furthermore, our engineering facility incorporates integrated carbon ESD discharge suppression rings and optional transparent conductive ITO / copper mesh layers, providing active electromagnetic shielding against lightning surges and high static charges common in tropical storm zones.
Mission-Critical Use Cases Across Solomon Islands
Empowering sustainable industrial modernization, renewable energy infrastructure, and maritime logistics throughout the archipelago.
Off-Grid Solar & Hybrid Battery Storage Systems
As Solomon Islands Electricity Authority (Solomon Power) expands mini-grid and off-grid solar initiatives across rural Guadalcanal, Western Province, and Malaita, inverter controller interfaces must withstand continuous outdoor thermal stress. Our matrix keypads feature UV-cured textured polyester graphic overlays and wide-temperature spacer layers (-40°C to +85°C) that maintain flawless tactile responsiveness on solar hybrid inverter interfaces, lithium battery management panels, and prepaid power dispensing kiosks.
Maritime Navigation, Inter-Island Ferries & Tuna Fleet Operations
Honiara acts as the maritime transit nexus for the archipelago, supporting tuna processing at Noro, cargo transport, and fishing vessel fleets. Salt spray and continuous physical wash-downs quickly disable conventional pushbutton keyboards. Our marine-grade matrix membrane panels utilize closed-cell silicone perimeter seals, gold-plated contacts, and embedded backlighting LEDs, ensuring deck-level radio controls, radar displays, and sonar control heads continue functioning safely without short-circuiting.
Agricultural, Timber & Palm Oil Automation
From palm oil processing in the Guadalcanal Plains to timber milling and cocoa drying facilities, plant floor controllers operate under heavy particulate and vibration exposure. Matrix membrane switches offer a completely flat, non-porous surface that easily sheds dust, oil droplets, and moisture, allowing high-pressure wash-down sanitation without risk of particulate jamming that plagues mechanical switches.
Emerging Technology Trends in Pacific Island HMI Manufacturing
Bridging Shenzhen’s Tier-1 industrial manufacturing ecosystem with the accelerating infrastructure needs of Honiara.
Integrated Turnkey Engineering: Transitioning from Component Sourcing to Unified Modules
Historically, engineering projects in the South Pacific suffered from extended lead times and integration risks caused by purchasing membrane keypads from one supplier, bare circuit boards from another, and passive electrical components from secondary brokers. When a multi-vendor assembly fails in the field, tracking root causes between adhesive degradation, solder bridge defects, or PCB trace impedance anomalies becomes an expensive logistical nightmare.
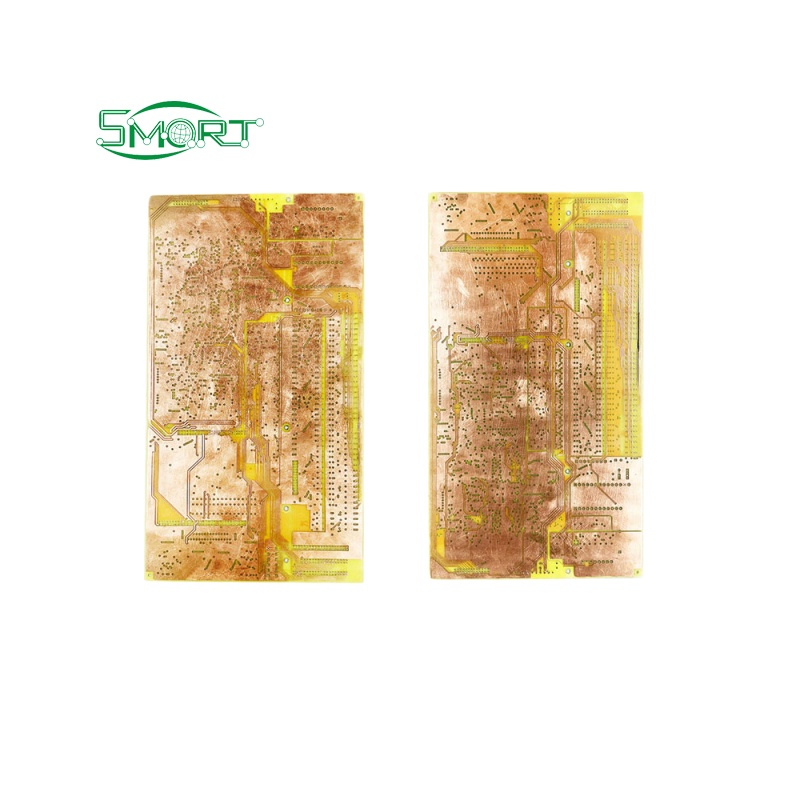
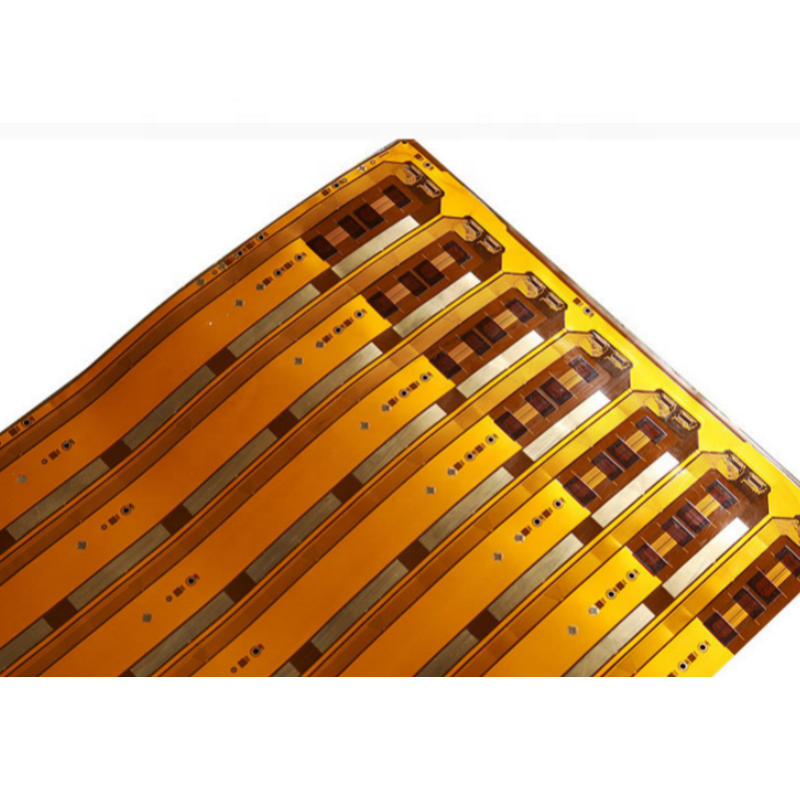
Shenzhen VUKO Electronics Co., Ltd. provides a complete vertical manufacturing framework directly serving engineering teams and procurement directors across Honiara. By unifying Bare PCB Fabrication (1-12+ layers), Precision FPC and Rigid-Flex Circuits, Full SMT/DIP Turnkey PCBA Assembly, and Custom Tactile Matrix Keypads under a single roof, we eliminate intermediate handling overheads and deliver fully pre-tested sub-assemblies. Every batch undergoes automated optical inspection (AOI), complete flying probe electrical continuity verification, and rigorous tactile actuation profiling before dispatch via express international air freight into Honiara International Airport (HIR).
Frequently Asked Questions by Pacific Importers & Engineers
Direct answers addressing freight logistics, environmental longevity, testing protocols, and minimum orders.
How do you protect matrix membrane switches from tropical fungus and high humidity in Honiara?
We deploy specialized antimicrobial and antifungal polyester overlay films coupled with hydrophobic ePTFE micro-pore breathing vents. These equalize internal atmospheric pressure during rapid temperature fluctuations without admitting high-humidity condensation or microscopic spores that can corrode silver conductors.
What is the standard Minimum Order Quantity (MOQ) for custom keypad prototypes?
Unlike traditional industrial tooling vendors that demand thousands of units, our prototype line supports low-volume orders starting from just 5 pieces. This enables hardware developers in Honiara to validate mechanical fit, tactile snap ratio, and graphic aesthetics before committing to full-scale mass production.
Can you provide turnkey PCBA with components sourced to back the keypad?
Yes. We specialize in comprehensive Bill of Materials (BOM) kitting, rigid FR4/Aluminum PCB fabrication, and surface-mount technology (SMT) component placement. We can mount microcontroller ICs, resistors, connectors, and LED indicators directly on a rigid or flexible PCB backer behind your membrane switch.
What file formats must be supplied to initiate a formal DFM review and quotation?
For the graphic overlay, we accept vector graphics in Adobe Illustrator (.AI), CorelDRAW (.CDR), or high-precision vector PDF format with Pantone/RAL color codes. For circuit layers and backing PCBA, please supply RS-274X Gerber files alongside drill files and a complete BOM with manufacturer part numbers.
What shipping methods and lead times apply for cargo destined for the Solomon Islands?
Urgent prototype and pre-production batches ship directly via express air couriers (DHL, FedEx, UPS) directly to Honiara within 4 to 7 working days. For high-volume mass production, we facilitate consolidated sea freight shipping to the Port of Honiara with moisture-proof, vacuum-sealed, and anti-static export crating.
How are international transactions secured and commercial warranties handled?
Orders can be fully secured through Alibaba Trade Assurance, providing complete payment protection, milestone escrow, and guaranteed dispatch timelines. Additionally, our production is certified under ISO 9001 quality systems, with full 100% electrical continuity testing performed prior to boxing.
Why Global OEMs Partner with VUKO Electronics
Combining world-class Shenzhen manufacturing density with stringent quality assurance standards.
Alibaba.com Onsite-Verified Supplier
Independently audited manufacturing facility with over 14 years of proven export expertise, ensuring complete operational transparency and verified production capacity.
Rigorous 100% Quality Inspection
Every single membrane keypad and PCBA undergo comprehensive automated optical inspection (AOI), high-voltage isolation checks, contact loop resistance profiling, and tactile actuation curve verification.
Rapid 24-Hour Engineering Turnaround
Our senior design for manufacturability (DFM) team reviews your vector art, schematic pinouts, and PCB layouts within 24 hours, actively spotting footprint mismatches and material vulnerabilities before fabrication.